Utility Distribution & High-Strength Monopoles
Direct factory-engineered transmission, distribution, and multi-service structural solutions deployed across major international tenders and utility power grids.
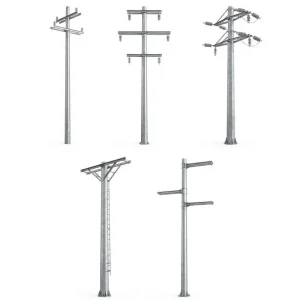
High-Quality URBAN-GRID Series Urban Low Voltage Steel Power Distribution Poles Suppliers, Factories
Technical Datasheet
Custom XINTONG High Strength Light Pole Series: Engineered for Extreme Conditions & Heavy Loads Manufacturers, Factories
Technical Datasheet
High-Quality STADIUM SERIES High Mast Light Factory, Exporter
Technical Datasheet
Best Series Decorative Street Light Pole Manufacturers, Manufacturer
Technical Datasheet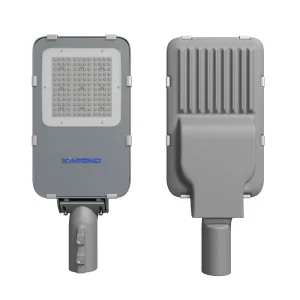
Best XT-DT-1 Series (Split Type) Manufacturer, Factories
Technical Datasheet
OEM XT-YTH-9 Series (All-In-One) Factory, Factories
Technical Datasheet
Custom XINTONG Full Series Municipal Street Light Poles Conical, Octagonal & Customizable Poles for Municipal Engineering Factory, Factories
Technical Datasheet
Buy XT-YTH-3 Series (All-In-One) Exporter, Exporters
Technical DatasheetGlobal Grid Modernization: The Structural Transition to Steel Monopoles
An analytical overview of utility asset hardening, decentralized renewable interconnections, and the systemic phase-out of legacy wood and spun concrete poles across transmission corridors.
The global electrical power transmission and distribution (T&D) infrastructure is traversing an unprecedented structural renaissance. Propelled by the rapid acceleration of the clean energy transition, legacy grid assets engineered in the mid-to-late 20th century are confronting systemic obsolescence. Traditional treated timber poles, while historically ubiquitous due to low initial purchase costs, exhibit severe biological degradation, vulnerability to rot and termite attack, variable mechanical fiber strength, and hazardous creosote leaching. Simultaneously, prestressed spun concrete poles, despite their compressive integrity, present extreme freight weight handicaps, brittle failure modes during seismic shear events, and micro-cracking that exposes inner reinforcement cages to catastrophic chloride attack in coastal regions.
In response to elevated climate volatility—manifested in Category 4 and 5 hurricane landfall events, intense derecho convective windstorms, and extreme ambient temperature cycles—international transmission system operators (TSOs) and distribution system operators (DSOs) are universally turning to cold-formed polygonal and tapered tubular steel power poles. According to global utility infrastructure surveys, the structural steel monopole segment is projected to expand at an annual compound rate exceeding 6.8% through 2035. This demand is further accelerated by the physical footprint limitations of urban and suburban rights-of-way (RoW). Where high-voltage lattice towers demand exorbitant land acreage and extensive clearance setbacks, engineered steel monopoles achieve equivalent transverse and longitudinal moment capacity on compact, single-drilled shaft foundation footprints.
Renewable Energy Grid Tie-In
Utility-scale photovoltaic farms and onshore wind energy hubs are frequently situated in remote geographical basins. Interconnecting these variable generation assets with central transmission backbones necessitates 33kV to 220kV feeder lines featuring rapid-erection steel monopoles capable of supporting high-capacity conductor bundle tensions.
Grid Hardening & Extreme Wind Design
In alignment with ASCE 74 and IEC 60826 structural criteria, contemporary utilities mandate poles capable of surviving extreme wind gust velocities exceeding 250 km/h with concurrent radial ice accretions of 25mm to 50mm, eliminating catastrophic cascading line failure mechanisms.
Compressed EPC Project Timelines
Telescopic slip-joint design allows pre-engineered steel segments to be transported efficiently in standard ocean shipping containers and assembled within hours on site via hydraulic jack clamping, reducing total substation-to-feeder construction cycles by up to 60% compared to cast-in-place concrete structures.
International EPC Tender Requirements & Metallurgical Standards
Decoding the technical specifications demanded by global utilities: ASCE 48-11, ASTM structural steel grades, PLS-POLE finite element validation, and certified anti-corrosion chemistry.
Global procurement teams operating across North America, the European Union, the GCC region, and Latin America face stringent technical vetting hurdles when sourcing overhead power poles. A failure in line hardware or pole structural integrity results not merely in direct material loss, but catastrophic grid de-energization, multi-million-dollar contractual penalties, and public safety liabilities. Consequently, qualified engineering tenders mandate unequivocal adherence to established structural and metallurgical benchmarks.
Primary structural calculations must be modeled utilizing nonlinear finite element tools such as PLS-POLE (Power Line Systems), verifying extreme load cases encompassing: (1) Heavy Wind with Zero Ice, (2) Extreme Radial Ice with Sustained Wind, (3) Broken Conductor Unbalanced Torsional Shock, and (4) Stringing/Maintenance Crew Dynamic Shock. Structural wall sections are engineered utilizing high-strength, low-alloy (HSLA) structural steels—predominantly Q355B/D, Q460D compliant with GB/T 1591, which directly parallel ASTM A572 Grade 50/65 and EN 10025-2 S355JR / S460ML. These steels offer an optimal balance of yield strength, ductility for cold press forming, and high Charpy V-notch impact toughness at sub-zero operating temperatures down to -40°C.
| Evaluation Parameter | Cold-Formed Steel Monopoles | Prestressed Spun Concrete | Chemical-Treated Timber | Traditional Lattice Towers |
|---|---|---|---|---|
| Design Service Life | 60+ Years (HDG ISO 1461) | 30–40 Years (Micro-crack prone) | 15–25 Years (Biological decay) | 50–60 Years (Fastener reliant) |
| Installation Weight Ratio | 1.0x (Baseline Lightweight) | 3.5x – 5.0x (Severe freight drag) | 1.2x – 1.6x (Variable moisture) | 1.3x – 1.8x (Disassembled) |
| Right-of-Way (RoW) Footprint | Minimal (1.5m – 2.5m Base Ø) | Compact (2.0m – 3.0m Base Ø) | Moderate (Requires guy wires) | Massive (8m x 8m to 16m x 16m) |
| Seismic & Lateral Shock Ductility | High Plastic Deformation Margin | Brittle Catastrophic Fracture | Moderate Deflection / Splitting | High (Redundant Member Matrix) |
| Environmental Contamination | 100% Recyclable, Non-Toxic | High Carbon Clinker Concrete | Creosote / Pentachlorophenol | 100% Recyclable |
| Erection Speed per Mile | 2 to 3 Days (Slip-Joint Crane) | 5 to 7 Days (Heavy Crane Lift) | 3 to 4 Days (Auger / Direct Bury) | 12 to 18 Days (Manual Bolting) |
China Factory 4.0: Supply Chain Resilience & Production Scale
Inside Yangzhou Xintong's 100,000 m² heavy-equipment industrial base in Gaoyou, Jiangsu: High-precision automated tandem press brakes, submerged arc welding, and automated hot-dip galvanizing lines.
In the heavy structural fabrication sector, supply chain consistency and process repeatability dictate project profitability. Headquartered in Gaoyou, Jiangsu—China’s premier industrial cluster for traffic and electrical infrastructure—Yangzhou Xintong Traffic Equipment Group has engineered an integrated end-to-end manufacturing footprint that eliminates subcontracting overhead and protects EPC delivery milestones. From raw hot-rolled plate decoiling to intermodal containerized export dispatch, every critical manufacturing phase is conducted within our audited 100,000 m² smart plant.
Automated Single-Seam Tandem Press Bending
Our facility houses 14-meter and 16-meter dual-machine CNC hydraulic tandem press brakes with a combined compression rating of up to 2,400 tons. This machinery enables cold forming of conical, octagonal, 12-sided, and 16-sided polygonal shafts up to 16 meters in a single continuous section without transverse circumferential splicing, dramatically enhancing structural fatigue life.
Robotic Submerged Arc Welding (SAW)
Longitudinal seams undergo automated dual-wire Submerged Arc Welding (SAW) conforming to AWS D1.1 structural welding codes. Non-destructive examination (NDE) incorporating 100% visual inspection and randomized ultrasonic (UT) testing ensures continuous weld penetration exceeding 85% on standard shafts and 100% complete joint penetration (CJP) at critical base flange gusset connections.
Full-Immersion Hot-Dip Galvanizing
After mechanical descaling, pickling, and fluxing, poles are fully submerged in a molten zinc bath maintained precisely at 450°C (±5°C). The metallurgical iron-zinc diffusion reaction forms an impervious, metallurgically bonded multi-layer armor (Gamma, Delta, Zeta, and Eta phases) conforming to BS EN ISO 1461 and ASTM A123, ensuring certified thickness upwards of 86 µm to 120 µm.
Engineered for Extreme Microclimatic Environments
From hyper-saline coastal trade corridors to sub-zero alpine permafrost, our custom metallurgical and coating treatments withstand the Earth’s harshest operational conditions.
C5-M Coastal & Marine
For installations within 500 meters of open sea (e.g., Chancay Port, Peru and Cebu Baseport, Philippines), we engineer a specialized duplex coating system: hot-dip galvanizing followed by an electrostatically applied epoxy-phenolic barrier and polyurethane topcoat (total DFT >180 µm) preventing sodium chloride pitting.
Hyper-Arid & Desert GCC
Deployed across Kuwait and Saudi Arabian energy grids, poles endure 55°C surface heat and blowing particulate abrasion. Our high-adhesion polyester thermoset coatings resist continuous UV photodegradation, while specialized anchor-bolt shroud enclosures seal out corrosive saline sands.
Typhoon Corridor Wind Resistance
Engineered for coastal Pacific rim typhoon passages, structural poles integrate aerodynamic polygonal section damping (12 or 16 facets) to disrupt vortex shedding, paired with high-tensile Q460D steel base plates engineered to withstand bending moments surpassing 1,200 kN·m.
High-Density Urban Right-of-Way
Where metropolitan street corridors provide zero clearance for traditional lattice footprints or concrete guy wires, self-supporting tubular steel distribution poles integrate low-profile flanged foundations with underground cable entry handholes and smart pole multifunction cross-arms.
Heavy-Duty Infrastructure & Distribution Monopoles
Full-spec municipal, high mast, and power distribution systems fabricated to project-specific drawings with complete mill test certificates and third-party inspection dossiers.
OEM PUBLIC TRANSIT Series Municipal High Mast Poles Manufacturers, Supplier
Technical Datasheet
OEM AIRPORT-PORT SERIES High Mast Light Manufacturer, Supplier
Technical Datasheet
High-Quality URBAN-GRID Series Urban Low Voltage Steel Power Distribution Poles Suppliers, Factories
Technical Datasheet
Buy XINTONG Municipal Street Light Pole Series Factories, Exporter
Technical Datasheet
OEM XINTONG Multifunctional Light Poles Integrated Design, Octagonal, Conical & Square Poles For Smart City Engineering Supplier, Factory
Technical Datasheet
Custom XINTONG High Strength Light Pole Series: Engineered for Extreme Conditions & Heavy Loads Manufacturers, Factories
Technical Datasheet
Best XT-DT-1 Series (Split Type) Manufacturer, Factories
Technical Datasheet
High-Quality STADIUM SERIES High Mast Light Factory, Exporter
Technical DatasheetFrequently Asked Engineering & Procurement Questions
Authoritative guidance on foundation load limits, slip-joint design tolerances, zinc galvanizing thickness verification, and global logistics optimization.
Our structural design calculations strictly comply with ASCE Manual 48-11 (Design of Steel Transmission Pole Structures) and IEC 60826 (Design Criteria of Overhead Transmission Lines). Calculations are verified via PLS-POLE finite element modeling, providing complete node displacement analysis, second-order P-Delta moment evaluations, and anchor-bolt stress interaction reports required by utility engineers of record.
Telescopic slip joints (friction fit) are preferred for high-voltage multi-segment transmission monopoles due to their streamlined profile, reduced manufacturing cost, and zero maintenance requirements (no loose bolts). The standard overlap length is engineered at 1.5 times the internal mate diameter. Flanged bolted connections are recommended when site clearance prevents longitudinal hydraulic jacking or in specialized substation dead-end structures.
We fabricate predominantly from high-strength low-alloy structural steels: Q235B, Q355B/D, and Q460D, fully cross-certified to ASTM A572 Grade 50/65 and EN 10025-2 S355/S460. Every production batch is dispatched with EN 10204 Type 3.1 Mill Test Certificates (MTC) documenting chemical ladle analysis (Carbon Equivalent CEV), yield point, tensile strength, elongation, and Charpy impact energy ratings.
Poles are galvanized after complete fabrication in adherence to BS EN ISO 1461 and ASTM A123. Both internal and external surfaces receive complete immersion coverage. Coating thickness is verified non-destructively utilizing calibrated magnetic flux gauges across the top, mid, and base sections. Minimum average coating thickness guaranteed is 86 µm, with custom specifications up to 120 µm+ available for aggressive C4 and C5 environments.
Our internal Quality Assurance department operates certified Level II NDT inspectors. Standard factory inspection dossiers encompass 100% Visual Testing (VT) of all weld profiles, 100% Ultrasonic Testing (UT) of full-penetration transverse flange welds, Magnetic Particle Testing (MT) of longitudinal seams, and dimensional verification of taper, sweep, twist, and bolt-circle geometry.
For large overseas tenders, poles are designed with precise modular taper diameters enabling internal nesting: smaller top sections are telescoped inside larger base sections during ocean container stuffing (40ft High Cube). This proprietary packaging engineering reduces total oceanic freight cubic volume by 35% to 50%, generating immense landed cost savings for international EPC contractors.