Certified Transmission & High-Capacity Utility Pole Series
Factory-direct structural steel monopoles, distribution poles, and specialized municipal lighting infrastructure fabricated in strict adherence to international electrical and metallurgical standards.
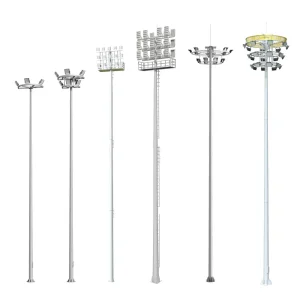
STADIUM SERIES High Mast Floodlight Infrastructure
View Specifications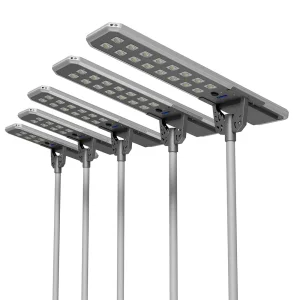
OEM XT-YTH-9 Series (All-In-One) Integrated System
View Specifications
PUBLIC TRANSIT Series Municipal High Mast Poles
View Specifications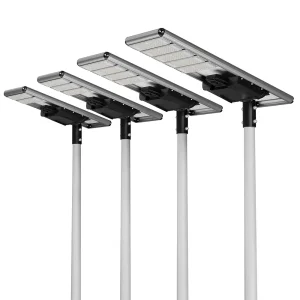
Buy XT-YTH-3 Series All-In-One Solar Lighting
View Specifications
Decorative Landscape & Architectural Light Pole
View Specifications
XINTONG Municipal Arterial Street Light Pole Series
View Specifications
AIRPORT-PORT Series High Mast Apron Light Tower
View Specifications
Multifunctional Integrated Smart City Utility Pole
View SpecificationsStructural Precision & Electrical Load Engineering Under IEC Standards
Designing overhead transmission monopoles demands rigorous mechanical calculation, dynamic wind-induced vibration analysis, and precise yield strength verification to secure national grid resilience.
IEC 60652 & IEC 60826 Load Validation
Structural integrity is calibrated against IEC 60826 (Design Criteria of Overhead Transmission Lines) and IEC 60652 (Full-Scale Loading Tests on Overhead Line Structures). Monopoles undergo rigorous Finite Element Analysis (FEA) to verify limit state designs across dead load, conductor tensile pulling force, transverse wind shear, and broken-wire unbalanced torsion scenarios.
High-Yield Steel Metallurgy (Q355 / Q460)
We deploy strictly certified low-silicon killed structural steel coils (Q235B, Q355B/D, Q420D, Q460D conforming to ASTM A572 Grade 50/65 and EN 10025 S355JR/S460). Controlled silicon content (<0.04% or between 0.15% and 0.25%) prevents the Sandelin effect during hot-dip galvanizing, ensuring uniform, shatter-proof metallurgical bonding of the protective zinc-iron alloy layers.
Submerged Arc Longitudinal Welding
Pole sections are bent through continuous 14-meter tandem CNC bending presses into 12-sided, 16-sided, or conical polygonal geometries. Automated submerged-arc longitudinal welding (SAW) achieves over 85% penetration in the shaft seam and 100% full-penetration ultrasonic testing (UT) compliance on structural base-plate flange connection welds per AWS D1.1 standards.
| Evaluation Parameter | IEC Certified Tubular Steel Monopole | Traditional Steel Lattice Tower | Spun Pre-Stressed Concrete Pole |
|---|---|---|---|
| Right-of-Way (RoW) Footprint | Ultra-compact (1.5m – 3.0m base radius); optimal for dense corridors. | Extensive (8m – 15m footprint); requires high land acquisition cost. | Moderate (2m – 4m base radius); heavy structural limitation. |
| Erection Speed & Labor | Rapid modular slip-joint assembly (1 to 2 days per pole). | Complex bolt assembly; multi-week erection cycle. | Extreme lifting weight; prone to hairline fracture during rigging. |
| Aerodynamic Wind Resistance | Polygonal aerodynamic design reduces drag coefficient (Cd ~0.65). | High drag matrix with complex dynamic vortex shedding (Cd >1.2). | Large solid surface area, high tipping moment under extreme gust. |
| Corrosion Life Span | 25 to 50+ years via ISO 1461 / ASTM A123 hot-dip galvanization. | Moderate; thousands of bolted joints subject to crevice corrosion. | Susceptible to freeze-thaw spalling and internal rebar carbonation. |
| Aesthetic & Urban Integration | Clean, streamlined industrial profile; powder coating available in RAL tones. | Heavy industrial intrusion; high visual resistance in populated areas. | Bulky, unrefined industrial aesthetic with zero aesthetic flexibility. |
100,000 m² Integrated Manufacturing Hub in Gaoyou, Jiangsu
By centralizing raw material procurement, cold-forming, continuous submerged-arc welding, and hot-dip galvanizing within our wholly owned industrial base, Xintong eliminates subcontractor bottlenecks to secure aggressive delivery schedules for global EPCs.
Gaoyou Industrial Ecosystem
Located in China's prime manufacturing corridor for steel utility structures and roadway lighting, Xintong leverages direct-tier partnerships with domestic primary steel manufacturers (Baosteel, Shougang). This ecosystem delivers massive volume pricing advantages, immediate sheet inventory buffering, and zero logistics downtime from coil delivery to cutting.
Automated Heavy-Plate Forming
Our factory floor houses tandem 1600-ton 14-meter CNC press brakes capable of forming polygonal utility sections up to 28mm in wall thickness in single pieces. This eliminates cross-sectional circumferential splices across individual pole stages, dramatically minimizing notch stress concentrations and preserving dynamic structural deflection limits.
In-House Hot-Dip Galvanizing
Unlike fabricators who outsource surface treatment to job-shop coaters, Xintong maintains integrated internal hot-dip galvanizing kettles (14m length x 2.2m width x 3m depth). Operating with high-grade #0 zinc ingots (>99.995% purity) at 445°C–455°C, we systematically guarantee coating thicknesses exceeding 86 µm up to 120+ µm per ASTM A123.
Solving Global Enterprise Procurement Bottlenecks
International infrastructure developers, utility operators, and EPC contractors encounter severe budget overruns and tender disqualification due to unverified documentation, weld fatigue, and joint mismatch. Xintong provides turnkey engineering verification from day one.
Tender Submittal Engineering Packages
We shorten utility tender qualification cycles by providing complete documentation: structural calculation packages calibrated with PLS-POLE / PLS-CADD models, TEKLA 3D manufacturing shop drawings, foundation anchor-bolt reaction matrices, and localized DIALux photometric simulations for integrated multi-service poles.
Dimensional Slip-Joint Tolerances
Multi-section transmission poles depend on precise slip-joint friction overlaps (typically 1.5 times the female inside diameter). Using computerized laser tracking and digital templates, we guarantee joint tolerances within ±2mm, preventing costly on-site hydraulic jacking failures or pole leaning during line tension stringing.
Third-Party Audits & Traceability
Every shipment carries full Mill Test Certificates (MTR) according to EN 10204 3.1. We routinely collaborate with international inspection agencies including SGS, Bureau Veritas, TÜV Rheinland, and Intertek for factory audits, witness ultrasonic flaw detection, and hot-dip zinc coating weight testing prior to port dispatch.
Engineering Monopoles for Extreme Global Terrains
Standard pole specifications cannot withstand localized environmental extremes. Xintong tailors material chemistry, section geometry, and protective barriers to survive coastal typhoons, desert thermal swings, and sub-zero ice loading.
Coastal High-Salinity & Typhoon Zones
In regions prone to category 4-5 tropical cyclones (e.g., Southeast Asia, Caribbean), structures are engineered for gust velocities exceeding 60 m/s. We apply a heavy duplex protection system: ISO 12944 C5-M marine-grade epoxy primer plus fluorocarbon or aliphatic polyurethane topcoat over ASTM A123 galvanizing to stop airborne chloride corrosion.
Desert Corridors & High Thermal Amplitudes
For installations across the Middle East and North Africa experiencing ambient shifts from -5°C to +55°C and severe sandstorm scouring, our poles employ UV-stabilized, high-hardness electrostatic polyester coatings. Base flanges are elevated with protective neoprene shrouds to prevent corrosive alkaline soil accumulation.
Sub-Zero Alpine & Radial Ice Loading
High-latitude grids (Central Asia, Nordic regions) require structural steel with guaranteed Charpy V-notch impact toughness at -40°C (Q355D/E or EN 10025 S355NL). Calculations incorporate extreme radial ice sleeves (20mm – 40mm) and longitudinal conductor breakage tension to prevent brittle cascading collapse.
Dense Urban Right-of-Way Distribution
Metropolitan utilities converting overhead 10kV–110kV lines along restricted boulevards use our sleek tapered polygonal monopoles. Custom crossarms accommodate dual-circuit distribution, fiber-optic OPGW ground cables, low-voltage street lighting arms, and telecom transceivers without encroaching on vehicle clearance.
Renewable Evacuation Lines (Solar & Wind)
Off-grid and utility-scale solar farms and wind complexes require fast, modular transmission tie-ins to high-voltage substations. Our standardized flange-connected steel poles expedite substation interconnection lines across uneven mountain ridges and agricultural plains with zero concrete setting delays.
The Evolution of Power Transmission Infrastructure
Grid modernization is driving structural steel utility assets toward intelligent sensory telemetry, multifunctional shared-infrastructure deployment, and low-carbon metallurgical lifecycles.
Smart IoT Structural Health Monitoring
Modern monopoles increasingly integrate internal fiber Bragg grating (FBG) strain sensors, 3-axis inclinometers, and wireless wind-vibration telemetry modules. Real-time dynamic load monitoring alerts utility dispatchers to dangerous galloping conductor oscillations, ground foundation subsiding, or localized structural fatigue before catastrophic outages occur.
Hybrid Infrastructure & Smart City Co-Location
The rigid separation between power transmission, municipal illumination, and 5G cellular hardware is dissolving. Xintong leads the deployment of integrated steel monopoles carrying medium-voltage transmission crossarms at top elevation, mid-shaft smart street lighting luminaires, and lower-level micro-base stations and environmental monitoring sensors.
Decarbonized Galvanization & Circular Steel
International tender scoring under ESG frameworks now demands quantified Environmental Product Declarations (EPD). Xintong's manufacturing transitions utilize recycled-scrap electric arc furnace (EAF) steel plates and closed-loop waste acid recovery systems during chemical pickling, cutting embedded carbon footprints by up to 32% per ton of fabricated pole.
Frequently Addressed Utility & EPC Questions
Authoritative engineering explanations covering slip-joint friction fits, deflection limits, corrosion coatings, and international compliance verification.
What international standards govern Xintong's transmission pole design and load testing?
Our power transmission monopoles and substations are engineered in accordance with IEC 60652 (Loading Tests on Overhead Line Structures) and IEC 60826 (Design Criteria of Overhead Transmission Lines). For North American and European projects, we routinely cross-certify against ASCE Manual 72 (Design of Steel Transmission Pole Structures), EN 40, EN 10025, and ASTM A572 / A123. Full structural design calculations, finite element stress models, and shop drawings are submitted with each bid.
How are slip-joint overlaps determined and verified for multi-piece utility poles?
Slip-joint splice overlaps are calculated as 1.5 times the internal diameter of the outer (female) section splice end, with a permissible manufacturing deviation of ±10%. Prior to packing and containerization, test assembly is performed at our Gaoyou plant using calibrated hydraulic jacks to ensure positive dimensional mating, exact linear alignment, and zero binding. Scribe marks are laser-etched onto both mating surfaces for foolproof on-site field assembly.
What is the standard anti-corrosion specification and design life expectancy?
All structural steel components undergo chemical shot blasting or pickling to clean surface finish Sa 2.5, followed by full-immersion hot-dip galvanizing per ASTM A123 / ISO 1461. The standard minimum zinc coating thickness is 86 µm (610 g/m²), but can be upgraded to 120 µm – 150 µm for corrosive C4 and C5 environments. In heavy-industrial or marine settings, we apply a duplex system combining hot-dip galvanization with a certified 100 µm polyurethane or epoxy powder coat, delivering maintenance-free service lives exceeding 50 years.
What maximum top deflection criteria are maintained under maximum serviceability wind load?
Under normal serviceability working load (unfactored continuous wind condition), horizontal top deflection is typically engineered not to exceed 1.5% to 2.5% of total above-ground pole height (H/60 to H/40). Under maximum ultimate design limit state wind conditions (conforming to IEC 60826 gust events), deflection is restricted to prevent conductor phase-to-phase flashover or ground clearance violation, verified via nonlinear P-Delta analysis.
Can Xintong handle containerization and breakbulk logistics for heavy, extra-long pole segments?
Yes. Our factory is directly linked to major shipping ports (Shanghai, Taicang, Ningbo). Standard pole sections up to 11.8 meters are packaged with non-abrasive saddles and protective strapping to load seamlessly into 40ft High Cube (40HQ) containers. For monolithic structures exceeding 12 meters in single sections, we handle breakbulk (BB) or Open Top flat-rack shipping with specialized sea-fastening calculations to eliminate transit deformation.
What third-party inspection certifications and non-destructive testing (NDT) are supplied?
Every production batch includes EN 10204 3.1 material test certificates for chemical and mechanical properties. In-house quality engineers execute 100% Visual Inspection (VT), Ultrasonic Testing (UT) on full-penetration base flange welds per AWS D1.1, Magnetic Particle Inspection (MT) on corner joints, and Elcometer magnetic zinc thickness verification. Third-party witness audits by SGS, Bureau Veritas, or customer engineers are readily supported prior to bill of lading issuance.
Engineered Street, Utility & Smart Infrastructure Solutions
Discover additional factory-manufactured distribution poles, heavy-load street lighting infrastructure, and off-grid solar equipment engineered for municipal and utility electrification tenders.
Custom High Strength Heavy-Load Light Pole Series
View Specifications
Full Series Municipal Street Light Poles (Conical & Octagonal)
View Specifications
Best XT-DT-1 Series (Split Type Solar Utility Light)
View Specifications
URBAN-GRID Low Voltage Steel Power Distribution Poles
View Specifications
High-Lumen Arena & Substation Stadium Mast
View Specifications
Intermodal Logistics Port & Terminal Mast
View Specifications
Industrial Grade Octagonal Municipal Light Pole
View Specifications
Smart Grid Multifunctional Monitoring Utility Pole
View SpecificationsConnect Directly with an Export Structural Engineer
Bypass standard intermediary trading desks. Submit your bill of quantities (BOQ), line voltage specs, wind zone parameters, and foundation soil profiles to receive fully certified structural calculations and factory-direct pricing within 24 business hours.
Verified Corporate Credentials
- Manufacturer: Yangzhou Xintong Traffic Equipment Group Co., Ltd.
- Establishment: 1999 (25+ Years Manufacturing Heritage)
- Plant Location: Guoji Industrial Area, Suiqiao Town, Gaoyou, Jiangsu, China
- Footprint: 100,000 m² | 7 Production Lines | 500+ Staff
- Certified Compliance: IEC 60652, IEC 60826, ASTM A123, EN 40, ISO 9001/14001
- Direct Inquiries: +86 178 5195 5363 | +86 180 3624 5278