High Mast & Municipal Infrastructure Assemblies
Heavy-duty steel support masts, intelligent optical heads, and integrated smart fixtures manufactured under certified ISO/EN structural benchmarks.
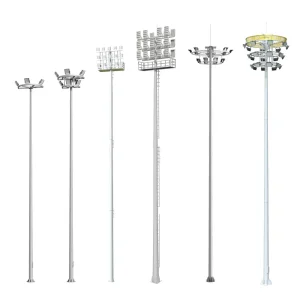
High-Quality STADIUM SERIES High Mast Light Factory, Exporter
Request Datasheet
OEM PUBLIC TRANSIT Series Municipal High Mast Poles Manufacturers, Supplier
Request Datasheet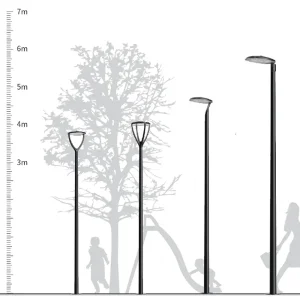
Best Series Decorative Street Light Pole Manufacturers, Manufacturer
Request Datasheet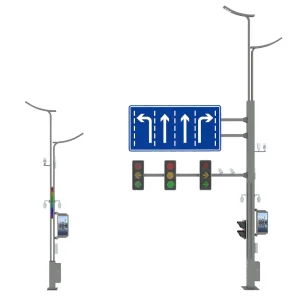
OEM XINTONG Multifunctional Light Poles Integrated Design, Octagonal, Conical & Square
Request Datasheet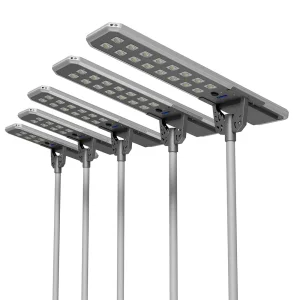
OEM XT-YTH-9 Series (All-In-One) Factory, Factories
Request Datasheet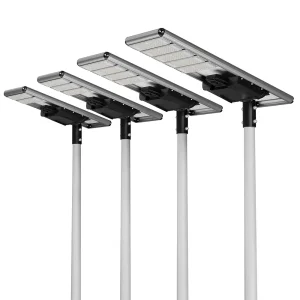
Buy XT-YTH-3 Series (All-In-One) Exporter, Exporters
Request Datasheet
OEM AIRPORT-PORT SERIES High Mast Light Manufacturer, Supplier
Request Datasheet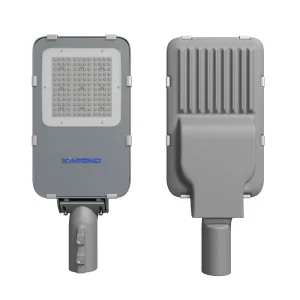
Best XT-DT-1 Series (Split Type) Manufacturer, Factories
Request DatasheetHigh Mast Lighting Architecture: Mechanical Dynamics & Global Deployment
A comprehensive examination of aerodynamic wind resistance, metallurgical fatigue limits, mechanical winch redundancy, and solid-state photometric convergence in critical infrastructure.
Structural Integrity & Aero-Elasticity
High mast area poles operating above 20 meters experience complex vortex-induced vibrations and aerodynamic drag. Our structural designs utilize tapered 12-sided, 16-sided, or 20-sided polygonal cross-sections manufactured from Q355B low-alloy structural steel, providing optimal damping ratios and minimal cross-wind turbulence coefficients conforming to EN 40 and AASHTO standard parameters.
Motorized Latching Mechanisms
Maintenance at heights above 25 meters represents a significant operational cost and risk. Our self-latching motorized raising and lowering systems (R&L) eliminate bucket truck dependencies. Stainless-steel aircraft-grade wire ropes (SUS316) operate through a dual-drum worm gear winch, utilizing dual mechanical locking pins that engage automatically at the masthead to release tension on the suspension cables indefinitely.
Photometric Distribution & Cut-off
High mast area illumination requires uniform lux distribution across thousands of square meters without blinding operators or creating light spill into adjacent airspace. Integrating asymmetric forward-throw TIR optical lenses with ultra-low BUG (Backlight, Uplight, Glare) ratings, our luminaire fixtures deliver system efficiencies over 160 lm/W while maintaining strict dark-sky compliance.
| System Attribute | Standard Highway Configuration | Maritime Port & Terminal Spec | Airport Apron / Airside Tier | Multi-Sport Arena / Stadium |
|---|---|---|---|---|
| Typical Mounting Height | 18m – 25m (Polygonal) | 30m – 45m (16/20 Sided) | 20m – 35m (Restricted Cut-off) | 25m – 50m (Cross-Arm Fixed) |
| Steel Grade & Thickness | Q235B / Q355B (6mm – 8mm) | Q355B Heavy (8mm – 12mm) | Q355B (6mm – 10mm) | Q355B Low-Alloy (8mm – 14mm) |
| Corrosion Resistance Class | ISO 1461 Hot-Dip (86µm) | C5-M Marine Coating + HDG (120µm) | ISO 1461 + Polyurethane Finish | Duplex System (HDG + Powder) |
| Design Wind Load Velocity | 140 – 160 km/h | Up to 240 km/h (Typhoon Zone) | 160 – 180 km/h | 150 – 180 km/h |
| Headframe & Lowering Type | Motorized Raising/Lowering | Heavy-Duty Motorized Ring | Fixed Headframe or Motorized | Fixed Service Platform / Ladder |
| Lighting Control Architecture | 0-10V / Astronomical Timer | DMX512 / IoT Centralized Gateway | DALI-2 / Redundant Airside Bus | DMX / High-Speed Broadcast Sync |
Precision Steel Fabrication & China's OEM Cost Advantage
Operating from our 100,000 square meter specialized facility in Gaoyou, Jiangsu, we merge metallurgical precision, submerged automatic arc welding, and fully internal hot-dip galvanization baths.
Continuous Deep-Drawing & Tandem Pressing
Tapered high mast shafts demand extreme longitudinal straightness and minimal seam distortion. Utilizing dual 1,600-ton synchronous tandem CNC bending machines capable of processing single-length plate sections up to 14 meters, our shafts feature unified single longitudinal seams, drastically minimizing welding stress concentrations across heavy load sections.
Automatic Submerged Arc Welding (SAW)
Full penetration longitudinal and base-flange welds undergo rigorous ultrasonic and magnetic particle testing (NDT) in compliance with AWS D1.1 structural welding standards. Robotic internal and external fillet welds at base flange transitions prevent mechanical shearing under dynamic cyclic loading provoked by gusts and microburst wind events.
In-House Hot-Dip Galvanizing & Coating
Complete structural elements undergo chemical pickling, degreasing, fluxing, and total immersion inside our internal molten zinc kettles (maintained at 450°C). Conforming to ASTM A123, ISO 1461, and AS/NZS 4680, coatings provide a metallurgical iron-zinc alloy layer exceeding 86–120 microns, complemented by optional thermoset architectural fluorocarbon powder topcoats.
Macro-Industry Evolution: Smart Interconnectivity & Energy Neutrality
The global transition from static high-pressure sodium (HPS) floodlighting to dynamic, sensor-driven LED topologies is revolutionizing industrial operating expenditures.
Centralized Smart Management (CMS) via LoRaWAN & Cellular IoT
Contemporary container terminals and transportation nodes no longer rely on unmonitored baseline lighting. OEM high mast systems now integrate wireless mesh controllers (LoRaWAN, Zigbee, NB-IoT) mounted at each luminaire driver bracket. Facility supervisors can partition vast logistics yards into dynamic photometric zones, dynamically scheduling luminous flux output depending on shifts, ship berth schedules, or security triggers, cutting auxiliary energy draw by up to 68%.
Adaptive Optics with Aerodynamic Luminaire Design
Traditional floodlight brackets imposed massive effective projected areas (EPA) on mast headframes, forcing engineers to oversize wall thicknesses and foundational caissons. Modern industrial luminaire housings utilize extruded aerospace-grade aluminum (A380/6063) engineered with aerodynamic air channels that dissipate thermal loads while cutting EPA by 35%. Multi-lens arrays offer precision cutoff angles, eliminating terminal glare for crane operators and runway air traffic.
Tailored Engineering for Critical Industrial Infrastructure
From saline sea spray along maritime quays to extreme sub-zero wind chills along trans-continental highways, high mast area lighting must perform without downtime.
Maritime Ports & Intermodal Container Yards
Operating in aggressive marine environments requires C5-M grade corrosion protection, stainless-steel electrical cabinets, and zero-glare vertical illuminance for rail-mounted gantry (RMG) crane operators. High masts positioned along container corridors deliver uniform 50–100 lux horizontal illuminance across stack alleys while resisting extreme coastal typhoons.
International Airports & Apron Logistics
Airside installations mandate strict compliance with ICAO Annex 14 and FAA photometric standards. Luminaire headframes must feature sharp-cutoff forward distribution that prevents pilot disability glare on final approach. Masts integrate obstruction lights (low/medium intensity Red Type A/B) and spark-resistant aviation ground-power junctions.
Multi-Tier Highway Interchanges & Toll Plazas
Complex multilane expressways require broad, seamless illumination coverage without creating visual flicker across elevated ramps and tunnels. High masts eliminate clutter caused by dozens of conventional small poles, enhancing driver situational awareness and substantially mitigating collision hazards.
Rail Freight Yards & Marshalling Depots
Rail freight hubs demand long, narrow photometric throws that penetrate between parallel railcars without generating stark shadow traps. Custom asymmetric beam orientations optimize ground safety for switch crew personnel while resisting severe vibration stresses induced by heavy rolling stock.
Petrochemical Refineries & Heavy Industry
Hazardous processing zones require explosion-proof junction boxes, surge protection devices (SPDs up to 20kV/40kA), and chemical-resistant polyurethane external coatings that withstand volatile sulfuric vapors, high thermal ambient temperatures, and 24/7 operating stress.
Multipurpose Stadiums & Sports Arenas
Illuminating football stadiums, track and field complexes, and sports training parks requires high color rendering indices (CRI > 80/90) and low television flicker factor (TLCI > 85) for 4K/UHD broadcast standards, supported by rigid fixed cross-arm masts with safety access ladders.
Tender Compliance Framework for International EPC Contractors
Overseas project procurement teams require exhaustive documentation, structural calculation proofs, and traceable testing regimens to satisfy consulting engineer oversight.
Structural Calculations & Soil-Structure Interaction
Every tender-ready project proposal from Xintong comes backed by comprehensive engineering calculation packages. We utilize specialized FEA structural analysis software to calculate base overturning moments, torsional shear, natural resonant frequencies, and anchor bolt stress profiles based on project-specific geotechnical survey reports and local ASCE 7 or Eurocode wind maps.
DIALux evo Optical Modeling & Verification
To eliminate compliance disputes, our photometric engineering department models full site geometries in DIALux evo before metal fabrication commences. We evaluate target horizontal, vertical, and semi-cylindrical lux values, overall uniformity ratios (U0, UI), glare ratings (GR < 45), and isolux curves, confirming tender compliance on the initial submittal.
Factory Acceptance Testing (FAT) & Material Traceability
Procuring authorities and third-party inspection agencies (SGS, Bureau Veritas, TÜV) receive 100% traceable steel mill certificates (EN 10204 3.1), ultrasonic weld inspection logs, magnetic particle test reports, zinc thickness gauge readings (magnetic induction method), and luminaire IP66/IK09 environmental certification dossiers.
Export Logistics, Container Optimization & KD Packing
High mast pole sections utilize nested telescoping slip-joints (telescopic overlapping lengths typically 1.5 times the mating diameter) engineered to pack directly into 40-foot HQ shipping containers. This KD (knocked-down) architecture maximizes container cube utilization, protecting protective zinc surfaces with wooden cradles and heavy-duty geotextile wraps during maritime transit.
Frequently Asked Questions: Engineering & Commercial
Direct technical responses addressing structural lifespan, motorized safety latches, foundation requirements, and custom manufacturing lead times.
We fabricate high mast sections using high-tensile structural steel conforming to Q355B (yield strength ≥ 355 MPa, comparable to ASTM A572 Grade 50 or EN 10025 S355JR) or Q235B for lower-stress upper extensions. Each pole design undergoes FEA stress modeling according to AASHTO Standard Specifications for Structural Supports for Highway Signs, Luminaires, and Traffic Signals or EN 40 standards. We calculate the ultimate limit state (ULS) and serviceability limit state (SLS) against client-specified basic design gust velocities, typically ranging from 120 km/h up to 260 km/h for cyclone-prone coastal ports.
Our motorized raising and lowering headframe incorporates a positive mechanical docking system (self-latching). Once the luminaire carriage reaches the mast top, spring-loaded mechanical lock arms pivot into heavy-duty structural latch barrels on the headframe. The motor then reverses slightly, transferring 100% of the luminaire ring's physical weight onto the solid steel latches. This ensures that the stainless-steel aircraft cables (SUS316) are completely relieved of mechanical tension during normal operation, preventing cable creep, wind-induced fatigue, and catastrophic drop risks. In addition, the internal hoist winch includes dual fail-safe braking systems.
All steel components are hot-dip galvanized inside our modern automated facility following fabrication, adhering rigorously to ISO 1461 and ASTM A123 standards. The minimum average coating thickness exceeds 86 microns, with coastal marine infrastructure orders receiving up to 120 microns. For extremely corrosive environments (ISO 12944 C5-I or C5-M classifications), we apply an integrated duplex coating system comprising abrasive sweep blasting, zinc-phosphate pre-treatment, and an electrostatic architectural polyester or fluorocarbon powder coating that provides over 25 years of corrosion-free performance.
Yes. We maintain an in-house team of senior optical, mechanical, and electrical project engineers. For any active tender or EPC contract, we generate certified DIALux evo simulations establishing luminance levels, lux uniformity, visual glare indexes, and electrical load schedules. We also provide stamped structural CAD drawings, anchor cage foundation template blueprints, and customized luminaire cross-arm configurations tailored to specific wind conditions and luminaire quantities.
We engineer our high masts utilizing a modular, precision-tapered slip-joint (telescoping overlap) system. Each section (typically 10 to 12 meters in length) is engineered with precise dimensional tolerances to slide tightly into the subsequent section with an overlap depth approximately 1.5 times the mating diameter. This knockdown structure permits seamless packing inside standard 40-foot Open Top (OT) or High Cube (HQ) shipping containers, eliminating expensive breakbulk shipping fees and protecting the galvanized surfaces during transit.
High Mast, Structural Support & Renewable Area Lighting
Select specialized structural poles and luminaire configurations engineered for harsh weather, heavy loads, and rapid commercial deployment.
OEM XT-YTH-9 Series (All-In-One) Factory, Factories
Request Datasheet
Buy XT-YTH-3 Series (All-In-One) Exporter, Exporters
Request Datasheet
OEM AIRPORT-PORT SERIES High Mast Light Manufacturer, Supplier
Request Datasheet
Best XT-DT-1 Series (Split Type) Manufacturer, Factories
Request Datasheet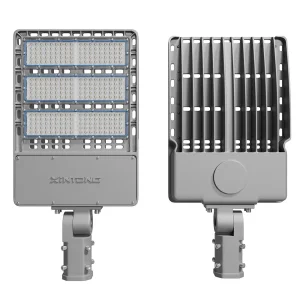
Buy XINTONG Municipal Street Light Pole Series Factories, Exporter
Request Datasheet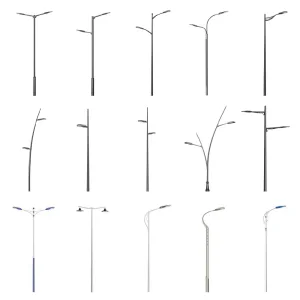
Custom XINTONG High Strength Light Pole Series Engineered for Extreme Conditions
Request Datasheet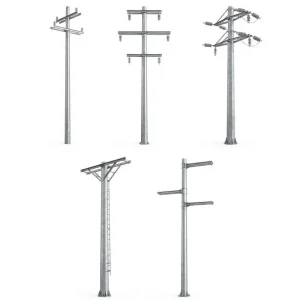
High-Quality URBAN-GRID Series Urban Low Voltage Steel Power Distribution Poles
Request Datasheet