Certified Structural Solutions for Distribution Networks
Explore our export-ready utility poles, high-strength luminaires, and smart infrastructure platforms designed for tender-specific wind load calculations and extreme environmental survivability.
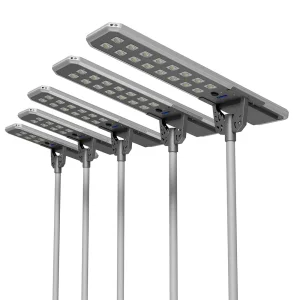
OEM XT-YTH-9 Series (All-In-One) Factory, Factories
View Product Specs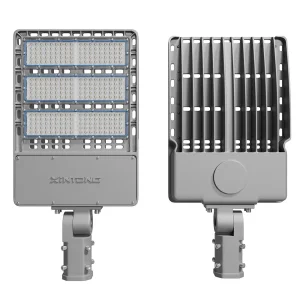
Buy XINTONG Municipal Street Light Pole Series Factories, Exporter
View Product Specs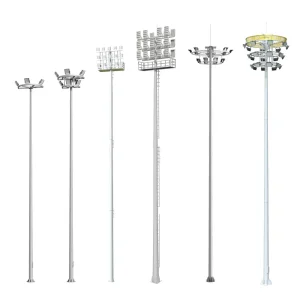
OEM PUBLIC TRANSIT Series Municipal High Mast Poles Manufacturers, Supplier
View Product Specs
Custom XINTONG Full Series Municipal Street Light Poles Conical, Octagonal & Customizable
View Product Specs
OEM AIRPORT-PORT SERIES High Mast Light Manufacturer, Supplier
View Product Specs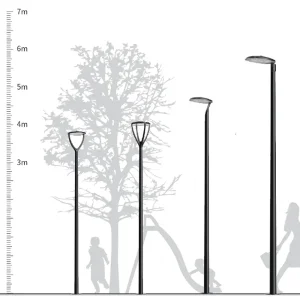
Best Series Decorative Street Light Pole Manufacturers, Manufacturer
View Product Specs
High-Quality STADIUM SERIES High Mast Light Factory, Exporter
View Product Specs
Custom XINTONG High Strength Light Pole Series: Heavy Loads Factories
View Product SpecsGlobal Rural Electrification Trends: Structural Evolution in Power Distribution
Analyzing macroeconomic drivers, regulatory evolutions, and the worldwide transition from traditional timber and concrete supports to engineered tubular steel poles.
SDG-7 Mandates & Last-Mile Grid Push
The international push toward the United Nations Sustainable Development Goal 7 (Universal Access to Affordable, Reliable, and Modern Energy) has radically transformed transmission economics. Over 675 million people globally remain without access to electricity, concentrated heavily in Sub-Saharan Africa, Central Asia, and isolated archipelagos in Southeast Asia. Regional governments and development banks (World Bank, AfDB, ADB) are mobilizing capital toward rural low-voltage (LV) and medium-voltage (MV) electrification corridors, driving unprecedented procurement demands for high-durability, standardized distribution steel structures.
Obsolescence of Wood & Spun Concrete
Historically, rural networks relied on creosote-treated wood poles or prestressed spun concrete poles. However, catastrophic failure rates under extreme weather events, accelerated rotting from soil microbial activity, termite infestations, and severe logistics penalties (concrete poles weighing up to 3 to 4 times more than hollow steel poles) have prompted electric utilities worldwide to update standard specifications. Polygonal and conical hot-dip galvanized steel poles offer an unmatched strength-to-weight ratio, zero biological degradation, and reduced foundation mass.
Decentralized Mini-Grids & Multi-Utility Roles
Modern rural distribution infrastructure is no longer exclusively centralized. The rapid deployment of solar-diesel hybrid microgrids, wind-battery off-grid stations, and agricultural solar pumping schemes requires distribution poles to function as multi-utility nodes. Today's rural poles frequently support dual circuits (e.g., 33kV distribution on upper crossarms, 400V 3-phase low-voltage below), integrated optical ground wire (OPGW) or ADSS telecom links for rural broadband, and integrated solar LED luminaires that enhance nocturnal community safety without additional substation load.
Enterprise Procurement Criteria: Mitigating EPC Risk & Lifecycle TCO
How state grid operators, independent power producers (IPPs), and turnkey EPC contractors evaluate metallurgical integrity, deflection tolerance, and freight logistics.
| Evaluation Parameter | Preservative-Treated Wood | Prestressed Spun Concrete | Xintong Hot-Dip Galvanized Steel Poles |
|---|---|---|---|
| Structural Service Life | 12 – 18 Years (Accelerated decay in tropics) | 20 – 30 Years (Prone to spalling & rebar rust) | 50+ Years (ISO 1461 Hot-Dip Galvanized) |
| Weight Ratio (Typical 11m Pole) | ~350 kg – 480 kg | ~900 kg – 1,400 kg (High crane requirement) | ~180 kg – 280 kg (Manual or light crane erection) |
| Freight Packing Density | Low; bulky irregular logs, high break-bulk rate | Extremely low; fragile, non-nestable | Exceptional; nested slip-joints, 40ft HQ container optimized |
| Bushfire & Termite Vulnerability | High vulnerability; combustible, bio-edible | Medium; cracking under intense thermal shock | Zero vulnerability; non-combustible, impervious to pests |
| Total Cost of Ownership (30-Yr TCO) | High (Frequent replacement & inspections) | Medium-High (Heavy handling & transport costs) | Lowest Lifecycle Cost (Virtually maintenance-free) |
Stringent Tender Verification
International competitive bidding (ICB) for transmission authorities (e.g., REA Kenya, TANESCO, PLN Indonesia, CFE Mexico) enforces zero-defect engineering documentation. Standard compliance demands full mechanical design calculations to ASCE Manual 48-11 or BS EN 40 standards, finite element analysis (FEA) validating moment capacity at critical ground-line sections, and destructive transverse tip-load validation to guarantee safety factors under broken-wire conditions.
Metallurgical & Zinc Density Standards
Procurement teams require certified mill test reports (MTR) according to EN 10204 3.1 certifying silicon and phosphorus content to guarantee optimal reactive steel behavior during immersion in molten zinc. Galvanizing must conform strictly to ASTM A123 / ISO 1461, achieving local coating thickness minimums exceeding 86 µm (up to 120 µm for heavy industrial or coastal salinity zones) to prevent premature pitting and subsurface oxidation.
Supply Chain Freight Optimization
For overseas projects, shipping costs represent up to 35% of total landed pole expenses. Tier-1 buyers demand modular telescoping slip-joint designs. By designing poles in nested, multi-segment sections with precise slip-joint overlaps (1.5 times the mating inner diameter), Xintong achieves up to 400% packing efficiency inside standard 40ft High Cube containers compared to rigid one-piece structural poles.
Advanced Production Ecosystem: Precision Steel Fabrication & Quality Control
Within our 100,000 m² Gaoyou facility, digital automated manufacturing lines convert prime certified structural coil into high-yield distribution and transmission poles.
Raw Steel Traceability
Direct procurement from prime steel mills (Baosteel, Shougang) ensuring Q235B, Q355B, and high-yield Q460 steel grades. Every master coil undergoes chemical spectrographic analysis and Charpy V-notch impact testing to ensure zero brittle failure under sub-zero or high-dynamic cyclic loading.
1600T Tandem Press CNC
Single-step mechanical bending utilizing our dual 1,600-ton 14-meter tandem CNC hydraulic press brakes. Enables formation of precise conical, octagonal, dodecagonal, and 16-sided polygonal profiles up to 14 meters in a single continuous section, minimizing circumferential seams.
Submerged Arc Welding (SAW)
Automated tracking submerged-arc longitudinal welding ensures deep penetration, defect-free welding lines compliant with AWS D1.1 structural welding standards. Zero open craters, uniform bead geometry, and 100% non-destructive ultrasonic testing (NDT) on critical tension seams.
Internal & External Galvanizing
Immersion in dedicated pre-treatment acid pickling and molten zinc baths operating at 450°C. Total encapsulation forms metallurgical iron-zinc intermetallic layers (Gamma, Delta, Zeta) capped by pure zinc (Eta), protecting inner bore walls against internal condensate accumulation.
Quality Assurance Protocols & Laboratory Metrology
At Yangzhou Xintong Traffic Equipment Group, our quality control is certified under ISO 9001, ISO 14001, and ISO 45001. Prior to factory containerization, every production lot undergoes an exhaustive 6-stage verification gate:
Localized Deployment Scenarios: Overcoming Global Terrain Challenges
Custom structural configurations engineered specifically for remote topographies, severe microclimates, and complex cross-country distribution alignments.
Coastal Corridors & Archipelagos
Environmental Challenge: Severe marine salinity (C5-M atmospheric corrosivity), high humidity, and recurring seasonal typhoons/cyclones.
Engineering Solution: Heavy-gauge Q355B steel with minimum 100 µm hot-dip galvanization plus a duplex electrostatically sprayed thermoset polyester powder coating. Aerodynamic circular or octagonal cross-sections designed for wind gusts up to 240 km/h (67 m/s) with sealed internal cable grommets.
Mountain Pass & Rocky Terrains
Environmental Challenge: Heavy logistics constraints, lack of access roads for heavy cranes, steep slopes, and high seismic fault risk.
Engineering Solution: Modular lightweight slip-joint segments (under 250 kg per section) transportable via light utility vehicles or animals. Micro-pile flange baseplate mounting systems requiring minimal rock excavation, coupled with ductile high-elasticity steel grades absorbing seismic ground accelerations.
Arid Corridors & Shifting Sands
Environmental Challenge: Extreme diurnal temperature cycling (-10°C to +55°C), intensive UV irradiation, and abrasive windborne sandstorms.
Engineering Solution: Direct burial steel poles with factory-applied heavy polyurethane anti-abrasion coatings up to 2 meters above groundline. Integrated copper-clad grounding terminals and specialized sand-exclusion vent caps preventing internal cavity accumulation.
Agricultural Feeder & Hybrid Grids
Environmental Challenge: Expansive agricultural areas requiring extended spans (up to 150m) to minimize footprint over arable land.
Engineering Solution: Tapered dodecagonal heavy-bending poles engineered for elevated conductor stringing tensions (ACSR conductors) with pre-welded transformer mounting brackets, drop-out fuse cutouts, and integrated low-voltage service take-off points.
Structural Sizing & Loading Performance Matrix
Reference technical specifications for common rural electrification steel distribution and multi-circuit pole profiles.
| Pole Class & Height | Nominal Line Voltage | Base / Top Diameter | Wall Thickness | Design Working Load | Ultimate Breaking Load | Standard Foundation Type |
|---|---|---|---|---|---|---|
| XT-REP-09 (9.0 m) | Low Voltage (0.4 kV) | 160 mm / 100 mm | 3.0 mm – 4.0 mm | 2.5 kN | 5.0 kN | Direct Burial (1.5m depth) / Flange |
| XT-REP-11 (11.0 m) | Medium Voltage (11 kV – 15 kV) | 210 mm / 140 mm | 3.5 mm – 4.5 mm | 4.5 kN | 9.0 kN | Direct Burial (1.8m depth) / Anchor Cage |
| XT-REP-12 (12.0 m) | Distribution MV (22 kV – 33 kV) | 240 mm / 150 mm | 4.0 mm – 5.0 mm | 6.0 kN | 12.0 kN | Reinforced Concrete Anchor Bolt Cage |
| XT-REP-14 (14.0 m) | Dual Circuit MV (33 kV) | 290 mm / 170 mm | 4.5 mm – 6.0 mm | 8.5 kN | 17.0 kN | Reinforced Concrete Anchor Bolt Cage |
| XT-REP-18 (18.0 m) | Sub-Transmission (66 kV) | 380 mm / 200 mm | 6.0 mm – 8.0 mm | 14.0 kN | 28.0 kN | Deep Drilled Shaft / Cast-in-Place Flange |
Need Custom Loading & Sag Calculations?
Our senior transmission engineering division provides full PLS-POLE and DIALux simulations tailored to your terrain elevation, conductor cross-sections, and national wind code requirements.
Engineering, Procurement & Export Technical FAQ
Authoritative technical answers addressing the critical structural, logistic, and contractual questions posed by international EPC engineers and utility supply directors.
Design calculations are governed by ASCE Manual 48-11, BS EN 40, or TIA-222 standards. The total lateral loading combines transverse wind pressure acting on the projected pole area, dynamic conductor wind drag, and transverse angle tension loads. Permissible tip deflection is typically restricted to 2.5% to 5.0% of total height under maximum working load to prevent conductor galloping, flashovers, and phase clashing.
Our poles undergo full immersion galvanizing according to ASTM A123 or EN ISO 1461. Steel thickness between 3mm and 6mm achieves an average coating thickness of 86 µm (610 g/m²), while sections exceeding 6mm receive a minimum of 100 µm to 120 µm. For high-salinity maritime or acid-rain zones, optional dual-coating systems with architectural polyester powder coatings are applied to ensure 50+ years of operational anti-corrosion life.
Slip-joint connections eliminate high-cost, field-bolted flange plates and hardware failure risks. In multi-piece poles, the upper segment slides over the lower segment with a minimum engagement length of 1.5 times the mating inner diameter. This connection is driven tightly via hydraulic come-alongs or pulling winches, providing complete moment transfer while dramatically saving container shipping space through telescoping nesting.
Direct burial is the preferred cost-effective choice for rural electrification corridors where pouring deep reinforced concrete pads is economically unfeasible. Direct burial typically requires embedment equal to 10% of pole length plus 0.6 meters, often encased in compacted aggregate or lean concrete. Flange baseplate with anchor cages is reserved for rocky strata, angle poles, terminal dead-ends, or highway installations with vehicle impact requirements.
We utilize proprietary 3D CAD packing optimization. By pairing tapered modular diameters, smaller top sections are nested directly inside larger base sections. Crossarms, bracket hardware, bolts, and small accessories are packed within seaworthy steel-strapped crates. This maximizes container cubic capacity (CBM), fitting between 60 to 120 completed rural distribution poles inside a single 40ft High Cube container, slashing landed shipping unit costs.
Yes. Our smart manufacturing allows integrated fabrication of dual-purpose rural poles. These structures feature pre-engineered bracket plates for solar photovoltaic modules and lithium battery packs, mid-shaft luminaire arms for nocturnal pathway illumination, and dedicated pole-top attachment rings for ADSS optical fiber cables, providing both electrical and broadband infrastructure simultaneously.
Distribution, Solar & Multi-Application Steel Poles
Engineered for seamless integration across municipal networks, rural feeder grids, remote mini-grids, and specialized transport applications.
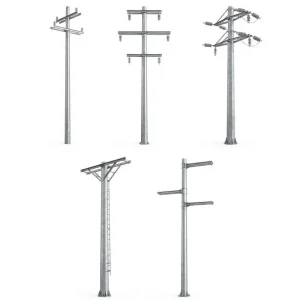
High-Quality URBAN-GRID Series Low Voltage Steel Power Distribution Poles Suppliers
View Product Specs
Best XT-DT-1 Series (Split Type) Manufacturer, Factories
View Product Specs
Buy XT-YTH-3 Series (All-In-One) Exporter, Exporters
View Product Specs
OEM XINTONG Multifunctional Light Poles Integrated Design Smart City Supplier
View Product Specs
OEM XT-YTH-9 Series (All-In-One) Factory, Factories
View Product Specs
Buy XINTONG Municipal Street Light Pole Series Factories, Exporter
View Product Specs
OEM PUBLIC TRANSIT Series Municipal High Mast Poles Manufacturers, Supplier
View Product Specs