High-Performance Structural Lighting Columns
Engineered to withstand harsh environments, extreme wind corridors, and saline coastal atmospheres.
Macro-Industry Dynamics & Global Infrastructure Trends
Decarbonization, urban density, and smart roadway electrification drive modern lighting pole specifications.
Global Infrastructure Resilience
The global infrastructure sector requires asset life cycles extending beyond 25–30 years under severe environmental stressors. Hot-dip galvanization (HDG) has transitioned from a standard specification to a critical metallurgical requirement under EN ISO 1461 and ASTM A123 to counteract aggressive industrial sulfur dioxides and coastal chlorination.
- Elimination of structural micro-cracks via pre-heating processes.
- Controlled zinc-iron alloy layers offering self-healing sacrificial galvanic defense.
- Minimization of lifecycle municipal maintenance expenditures.
EPC Contractor Economic Realities
Modern EPC contractors face compressed project timelines and strict liquidated damages clauses. Sourcing directly from an integrated tier-one manufacturer ensures unified traceability from raw steel coil slit down to finished anchor bolts, avoiding multi-tiered markups and fragmented quality standards across distinct subcontractors.
- Elimination of intermediary margins via end-to-end direct manufacturing.
- Single-point accountability for structural calculations and finish coatings.
- Pre-matched luminaire mounting brackets and anchor bolt cages.
The Smart City Integration Shift
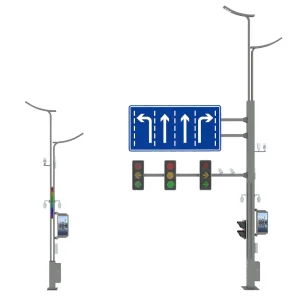
Standard illumination masts are evolving into multi-sensor IoT telecommunication nodes. Galvanized steel provides the ultimate structural torsional stiffness required to stabilize sensitive 5G micro-cells, high-resolution pan-tilt-zoom (PTZ) optics, roadside weather units, and electric vehicle (EV) charging peripheral loads without dynamic harmonic distortion.
- Torsional stiffness designed for millimetric surveillance tracking.
- Concealed internal wiring raceways with compartmentalized maintenance doors.
- Multi-bracket structural validation preventing resonant wind fatigue.
Structural Design & Anti-Corrosion Engineering
Comprehensive technical breakdown of Q235/Q355 substrate handling, submerged arc welding, and hot-dip immersion standards.
| Parameter / Criteria | Q235 Structural Steel Grade | Q355 High-Strength Steel Grade | Compliance / Standard Benchmark |
|---|---|---|---|
| Yield Strength (ReH) | ≥ 235 MPa | ≥ 355 MPa | GB/T 700 / EN 10025-2 S235JR / ASTM A36 |
| Tensile Strength (Rm) | 370 – 500 MPa | 470 – 630 MPa | GB/T 1591 / EN 10025-2 S355JR / ASTM A572 Gr 50 |
| Galvanization Process | Hot-Dip Full Immersion (Bath Temp ~450°C) | Hot-Dip Full Immersion (Bath Temp ~450°C) | EN ISO 1461, ASTM A123, AS/NZS 4680 |
| Average Zinc Coating | 86 µm – 100 µm (Up to 700 g/m²) | 100 µm – 120 µm (Up to 850 g/m²) | Magnetic Induction Calibration (ISO 2178) |
| Welding Integrity | Automatic Submerged Arc Longitudinal Seam | Automatic Submerged Arc Longitudinal Seam | AWS D1.1 Structural Welding Code / EN ISO 15614 |
| Corrosion Resistance Life | 25+ Years in Urban/Inland Settings | 30+ Years in C4/C5 Harsh Marine Corridors | ISO 12944 Atmospheric Corrosivity Categories |
Localized Applications & Turnkey Field Scenarios
Engineering adaptation across diverse global climatic regions, from arid deserts to freezing mountainous terrains.
Seaports & Maritime Terminals
High-salinity atmospheres present relentless corrosion challenges. Deployments such as the Cebu Baseport project feature heavy-wall octagonal/polygonal masts with heavy zinc encapsulation, protecting the mast shaft against corrosive sea sprays.
- Motorized lowering crowns for effortless high-wind servicing.
- Heavy-duty base plates with anti-vibration damping pads.
Arid & High-Heat Corridors
Desert settings, like regional highway systems in Kuwait and Saudi Arabia, combine blistering ultraviolet exposure, rapid diurnal thermal swings (-5°C to 50°C), and airborne abrasive sandstorms.
- Duplex coating systems: HDG + Electrostatic UV-stabilized polyester powder.
- Sealed IP65 access hatches preventing fine sand penetration.
Sub-Zero & Heavy-Snow Routes
Projects like the Manas Airport to Bishkek highway route encounter freezing temperatures and aggressive road-clearing de-icing salts that corrode base welds.
- Low-temperature impact-tested steel grades avoiding cold embrittlement.
- Reinforced double-flange root welds designed for sustained snow load.
High-Load Smart Metropolises
Urban thoroughfares demanding simultaneous support of street lights, solar tracking fixtures, CCTV analytics, and transit coordination sensors without dynamic flexing.
- Segmented internal conduit design separating LV power and optical fiber.
- DIALux-modeled cantilever designs ensuring zero glare and uniform lux.
Engineering Governance & Future Technology Roadmap
Stringent tender certifications and next-generation advancements in composite galvanizing and IoT intelligence.
Quality Governance & Testing
Every manufacturing batch undergoes comprehensive testing prior to bill-of-lading issuance to ensure structural integrity and compliance.
- Ultrasonic Flaw Detection: Verifies complete weld joint penetration across longitudinal seams.
- Coating Thickness Gauge: Calibrated to ASTM B499 to verify micro-thickness specifications.
- Full Factory Audit: Mill test certificates (MTC 3.1) and DIALux submittals provided for direct bid approvals.
Advanced Zinc-Aluminum-Magnesium Coatings
Moving beyond standard hot-dip solutions, advanced applications now adopt next-generation Zinc-Aluminum-Magnesium (Zn-Al-Mg) bath chemistry.
- Superior self-healing cut-edge behavior via protective simonkolleite barriers.
- 3x to 5x higher resistance in aggressive salt-spray testing chambers (ASTM B117).
- Reduced coating weight while achieving higher mechanical abrasion thresholds.
IoT-Enabled Structural Health Monitoring
Modern high-mast systems and smart distribution infrastructure now interface with low-power LoRaWAN and NB-IoT telemetry.
- Tri-axial accelerometers monitoring base vibrational resonance and fatigue.
- Early warning deflection detection during extreme hurricane-force winds.
- Predictive maintenance alerts minimizing manual physical inspection risks.
Frequently Asked Technical & Sourcing Questions
Comprehensive engineering insights for municipal procurement authorities, structural consultants, and contractors.
What is the distinction between electro-galvanizing and hot-dip galvanizing for lighting poles?
Electro-galvanizing (cold galvanizing) applies a thin zinc layer (typically 5–15 µm) via electroplating, suitable only for light indoor equipment. Hot-dip galvanizing submerges cleaned steel in molten zinc (~450°C), forming bonded zinc-iron metallurgical alloy layers (86–120 µm). This process provides superior barrier and sacrificial galvanic protection, which is essential for roadside infrastructure exposed to outdoor weathering.
How are lighting pole wind loads calculated for coastal or cyclonic zones?
Calculations follow AASHTO Standard Specifications for Structural Supports for Highway Signs, Luminaires, and Traffic Signals or EN 40 standards. Engineers calculate effective projected area (EPA) including pole shaft, bracket outreaches, and luminaire wind drag, dynamic wind pressures, and drag coefficients. Mast thickness, base plate gusset stiffeners, and anchor bolt configurations are scaled accordingly to withstand specified gust speeds (e.g., 160 km/h up to 240 km/h).
Can you manufacture customized pole cross-sections and bracket geometries?
Yes. Utilizing large-scale CNC bending presses, XINTONG produces conical, octagonal, polygonal, and custom square configurations. Custom cantilever arms, dual-arm roadway brackets, mid-hinge lowering mechanisms, and integrated smart city sensor platforms are fabricated directly from customer submittal drawings or developed through our internal engineering department.
What documentation accompanies an international export shipment?
Every commercial export order includes Material Test Reports (MTR / Mill 3.1) confirming chemical composition and tensile/yield properties, hot-dip galvanizing batch thickness inspection certificates, ultrasonic weld testing records, dimensional verification checklists, packaging lists, and container load diagrams for customs clearance and tender compliance.
Explore Additional Infrastructure & Heavy-Load Solutions
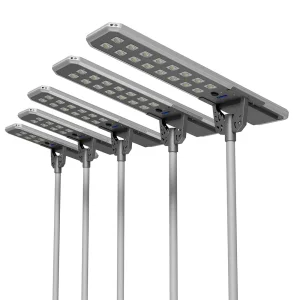
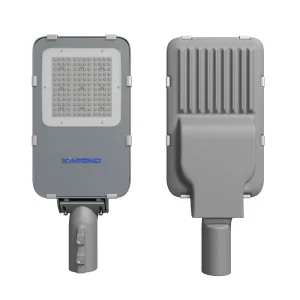
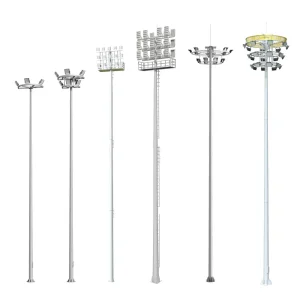
Select from specialized split-type solar fixtures, municipal octagonal series, and heavy-duty airport towers.