Primary Engineering Series
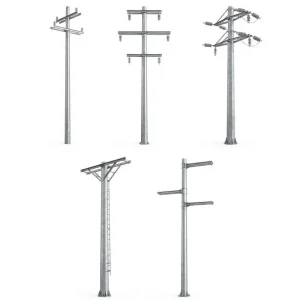
Featured Utility Distribution & Infrastructure Poles
Precision-manufactured structural steel poles engineered to meet EN 1090-2, ASTM A123, and IEC 60652 standards. Fully verified through destructive testing, digital FEA modeling, and zinc-metallurgical analysis.
Industry Paradigm & Regulatory Evolution
The Global Transition to CE Certified Tubular Steel Power Poles
Modern electrical grids require robust, resilient, and non-combustible infrastructure. Utility operators across the European Union, the Americas, and APAC are aggressively phasing out pressure-treated timber and heavy prestressed spun concrete in favor of engineered polygonal and tubular steel distribution poles.
CE CPR Regulation No 305/2011
For an electric power pole to achieve valid CE certification within European and aligned tender markets, the manufacturing facility must hold a Factory Production Control (FPC) audit under EN 1090-1 and satisfy technical execution specifications according to EN 1090-2 (Execution of steel structures EXC2/EXC3).
- Fully traceable 3.1 Mill Test Certificates (MTC)
- Qualified Welding Procedure Specifications (WPS/WPQR)
- Charpy V-Notch impact toughness tested down to -20°C
Grid Hardening Against Climate Volatility
Wildfires, Category 5 cyclonic wind loads, and torrential freeze-thaw cycles have compromised legacy wooden and spun concrete poles worldwide. Hot-dip galvanized structural steel delivers deterministic yield behavior under transverse wind shear and longitudinal cable breakage shock loads.
- 100% non-combustible wildfire resilience
- Elastic deflection recovery without micro-cracking
- Calculated gust mitigation up to 60 m/s (216 km/h)
Renewables & Distributed Energy Integration
Decentralized solar, wind micro-generation, and battery storage demand distribution feeder upgrades. CE-certified steel poles can support complex multi-circuit cantilever crossarms, reclosers, auto-switchgear, step-down transformers, and fiber-optic ADSS communications.
- Modular crossarms for 10kV to 132kV overhead systems
- Integrated grounding lugs & internal conductor channels
- Substation dead-end and angle-strain configurations
Tender Engineering Specifications
Engineering Verification: Comparing Steel, Concrete, and Wood Poles
Procurement teams for major EPC projects must justify Total Cost of Ownership (TCO), logistics overhead, and environmental impact. Below is a comparative technical matrix illustrating why CE-certified tubular steel poles consistently win public utility tenders.
| Performance Parameter | CE Certified Steel Pole (Xintong) | Prestressed Spun Concrete | Creosote-Treated Wood Pole |
|---|---|---|---|
| Structural Strength-to-Weight Ratio | Extremely High (30-50% lighter than concrete) | Low (Heavy crane required for all handling) | Moderate (Subject to internal rot & grain variance) |
| Service Life Expectancy | 50 – 70 Years (ISO 1461 hot-dip galvanized) | 25 – 40 Years (Subject to spalling & rebar corrosion) | 15 – 25 Years (Decay, termite attack, leaching) |
| Bending Moment & Deflection Behavior | Ductile yield; predictable FEA failure limits | Brittle catastrophic failure mode under shear | Non-uniform deflection; organic micro-fractures |
| Transport & Freight Optimization | Telescopic Slip-Joint Design fits 40ft HQ containers | Extremely bulky, heavy freight costs, breakage risk | Length-limited by forestry; high deadweight freight |
| Environmental & End-of-Life Lifecycle | 100% Recyclable high-value scrap recovery | Landfill disposal burden; non-recyclable matrix | Hazardous chemical waste (creosote / pentachlorophenol) |
| Installation Speed & Foundation Cost | Anchor bolted base plate or direct embedment | Deep direct auger hole, extensive crane leveling | Direct burial; high sensitivity to soil saturation |
Smart Manufacturing & Quality Traceability
China Factory 4.0: Metallurgical Precision at 100,000 m² Scale
Operating from our smart production hub in Gaoyou, Jiangsu, Yangzhou Xintong Traffic Equipment Group integrates continuous automated bending, robotic submerged arc longitudinal welding, and an advanced closed-loop galvanizing facility to guarantee uncompromised structural integrity for global EPC contractors.
1. Raw Plate CNC Cutting & Grading
Every steel coil or heavy plate is sourced from Tier-1 mills (Baosteel, Shougang) with mandatory spectrographic chemical testing. Laser and high-definition underwater plasma cutters slice conical tapers up to 20mm thickness with sub-millimeter edge precision, preparing zero-gap beveled seams.
2. 1600T/2400T Tandem Hydraulic Bending
Our dual CNC tandem hydraulic press brakes bend single-piece polygonal sections up to 14 meters without intermediate transverse joints. Octagonal, 12-sided, 16-sided, or conical tubular geometries are stamped with uniform wall thickness and strict angular concentricity.
3. Automated Submerged Arc Welding (SAW)
Longitudinal seams are automatically clamped and welded using dual-wire Submerged Arc Welding machines with continuous ultrasonic tracking. Full root penetration exceeds 95% of wall thickness with zero porosity, undercut, or slag inclusion, inspected per AWS D1.1 / EN ISO 15614.
4. Hot-Dip Galvanizing per ISO 1461
Fully immersed into a 15-meter molten zinc kettle maintained at 450°C. Controlled silicon chemistry ensures dense, intermetallic iron-zinc alloy diffusion layers (Gamma, Delta, Zeta, Eta), delivering certified coating thickness exceeding 86 µm (up to 120 µm for marine C5-M zones).
5. Electrostatic Powder Duplex Finish
For urban aesthetic or high-corrosion industrial zones, poles receive an automated surface sweep blast followed by an electrostatic architectural polyester powder coat cured at 200°C. Resists salt-fog testing for over 1,500 hours without flaking or chalking.
6. NDT & Digital Proof Testing
Quality assurance protocols include Magnetic Particle Testing (MT), Ultrasonic Testing (UT) on full-penetration base plate welds, coating thickness magnetic gauge audits, and full-scale horizontal deflection pull tests verified against customer FEA modeling.
Field Deployment Engineering
Engineered Field Scenarios: From High-Salinity Coasts to Mountain Corridors
Transmission and distribution engineers encounter vast geological and climatic variations. Xintong designs customized pole tapers, wall thicknesses, and connection brackets to accommodate specialized geotechnical and environmental profiles.
Coastal Port Corridors & Severe Saline Atmospheres (ISO 12944 C5-M)
In maritime commercial logistics zones like the Cebu Baseport project, chloride-saturated humid sea spray rapidly corrodes substandard zinc coatings. Xintong utilizes high-purity #0 zinc with controlled aluminum additions, producing a minimum 100 µm zinc layer backed by an optional fluoropolymer or polyurethane duplex coat to guarantee 40+ years of zero-maintenance structural longevity.
- Grade 316 stainless steel access fasteners & earth-ground hardware
- Fully sealed pole tops to prevent internal marine condensation buildup
Substation Terminal Take-Offs & Angle Strain Poles
At the interface between high-voltage overhead lines and urban underground cable risers, dead-end termination poles must resist sustained unbalanced cable tension up to 120 kN without unacceptable tip deflection. Fabricated with thicker wall profiles (8mm to 16mm Q355B structural steel) and gusset-reinforced flange bases anchored to high-strength concrete foundation cages.
- Calculated tip deflection limited to less than 1% of above-ground height
- Pre-drilled CNC attachment points for lightning arresters & potheads
Narrow Urban Rights-of-Way & Multi-Circuit Distribution
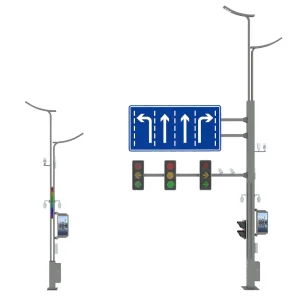
Modern city boulevards cannot accommodate wide lattice transmission towers. Xintong's slim polygonal tubular steel poles feature compact cantilever crossarms capable of carrying dual 33kV circuits alongside low-voltage 400V neutral-supported secondary distribution, fiber-optic telecom lines, and integrated street lighting fixtures.
- Significantly reduced footprint compared to wooden H-frames or lattice masts
- Direct embedment with polyurethane backfill or anchor base options
Desert Corridors: High Thermal Shock & Sand Abrasion
In high-UV, arid environments such as Kuwait and the wider Gulf region, daytime steel temperatures frequently exceed 65°C followed by swift nocturnal drops, accompanied by aggressive airborne sandblasting. Our heavy-duty galvanized surface combined with mechanical hardness prevents abrasive zinc erosion.
- Micro-hardness of zinc-iron alloy layer (Zeta phase) exceeds base steel
- Complete structural resistance against cyclic thermal expansion fatigue
Engineering Knowledge Base
Frequently Asked Technical & Procurement Inquiries
Straightforward, data-backed answers addressing structural metallurgy, CE documentation, international slip-joint assembly, and destructive testing standards for EPC consulting engineers.
What specific standards and certifications govern CE marked electric power poles?
CE marking on structural steel poles is governed primarily by Regulation (EU) No 305/2011 (Construction Products Regulation - CPR). The core technical benchmark is EN 1090-1 (Requirements for conformity assessment of structural components) and EN 1090-2 (Technical requirements for steel structures, typically specified at Execution Class EXC2 or EXC3 for utility transmission).
Additionally, poles configured with lighting arms or auxiliary luminaires conform to EN 40-3-1 / EN 40-3-3 for structural design calculations and verification by testing. Every consignment produced by Yangzhou Xintong includes a Declaration of Performance (DoP), 3.1 Mill Test Certificates verifying yield and tensile properties per EN 10025, and third-party inspection sign-offs.
How do Chinese steel grades Q235B and Q355B correlate with European S235JR and S355JR?
The correlation between Chinese national standards (GB/T 1591 / GB/T 700) and European designations (EN 10025-2) is fully documented and recognized by international engineering consultants:
• Q235B vs. EN S235JR: Both provide a minimum yield strength ($R_e$) of 235 MPa for thickness $\le 16$mm, with Charpy V-notch longitudinal impact test absorption of $\ge 27\text{ Joules}$ at +20°C.
• Q355B vs. EN S355JR: Both exhibit a minimum yield strength of 355 MPa and tensile strength between 470–630 MPa, with identical 27J impact values at +20°C. For sub-zero installations down to -20°C, Xintong utilizes normalized Q355D or S355J2 with guaranteed cryogenic toughness.
What is the standard slip-joint (telescopic overlap) tolerance for multi-section poles over 15m?
For transmission poles exceeding single-piece manufacturing or standard shipping container dimensions (12 to 14 meters), telescopic slip joints are engineered per ASCE Manual 72 and European standards. The minimum overlap length is calculated using the empirical industry standard:
$$\text{Overlap Length} = 1.5 \times \text{Inside Diameter of the Female Joint Tip}$$
During factory assembly, male and female joints are laser-checked for axial straightness and concentricity. Field installation utilizes hydraulic pullers or chain come-alongs to seat sections to match factory-stamped witness index marks, eliminating the need for expensive in-field welding.
How does hot-dip galvanizing guarantee corrosion protection for over 50 years?
Unlike organic paint which provides only a barrier, hot-dip galvanizing per ISO 1461 / ASTM A123 produces a metallurgical bond between iron and molten zinc. The steel is chemically degreased, acid-pickled, fluxed, and immersed in zinc at 450°C. This forms a series of iron-zinc alloy layers:
1. Gamma Layer (75% Fe, 25% Zn): High hardness, metallurgical bond to core steel.
2. Delta Layer (90% Zn, 10% Fe): Hexagonal crystals providing wear resistance.
3. Zeta Layer (94% Zn, 6% Fe): Columnar crystals harder than the structural base metal.
4. Eta Layer (100% Zn): Ductile pure zinc exterior.
Even if scratched down to bare steel during rigging, the surrounding zinc sacrifices itself cathodically (galvanic protection), preventing underfilm rust migration.
What parameters are required to generate an engineer-stamped foundation and pole proposal?
To deliver fully calculated CAD submittal drawings, foundation bolt schedules, and structural moment calculations, our engineering department requires the following tender inputs:
• Line Configuration: Nominal operating voltage, conductor type/diameter (e.g., ACSR Drake/Grosbeak), number of circuits, ground wire / OPGW count.
• Span & Loading: Ruling span distance, maximum design wind speed (m/s or km/h), radial ice thickness (mm), ambient temperature extremes.
• Pole Function: Suspension (tangent), angle strain (e.g., 15°, 30°, 60°), or terminal dead-end.
• Mounting Type: Base-plate flange with anchor cage assembly or direct burial (embedded depth calculated as 10% + 2 feet).
Export Product Catalog
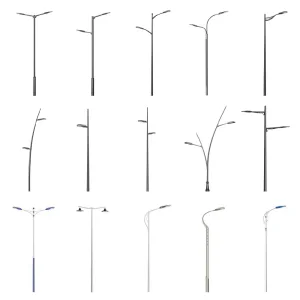
Comprehensive Certified Steel Poles & Lighting Systems
Direct factory supply from our 100,000 m² Jiangsu facility. Every model is supported by standard structural calculations, wind-load certifications, DIALux simulation files, and tender-ready datasheets.