High Mast & Specialized Infrastructure Solutions
Direct from our 100,000 m² ISO/EN/AASHTO certified manufacturing base. Precision-fabricated polygonal high masts and specialized poles designed for extreme wind resistance, vibration resilience, and 24/7 continuous rail operation.
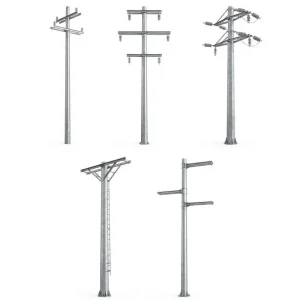
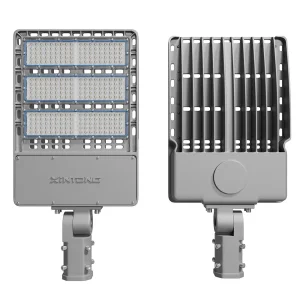
The Global Commercial & Industrial Reality of Rail Yard Lighting
Modernization of freight logistical corridors and strict safety mandates under AREMA, UIC, and EN standards drive structural shifts from legacy high-pressure sodium fixtures to intelligent high mast LED towers.
Rail freight operations represent the circulatory system of global supply chains. Within classification yards, gravity hump yards, container transshipment depots, and intermodal locomotive servicing terminals, lighting is not merely a utility—it is a critical life-safety baseline. Historically, massive rail yards depended on high-pressure sodium (HPS) or metal halide lamps mounted on 25m to 45m steel lattice towers. These systems suffered from severe disadvantages: excessive lumen depreciation, dangerous color-rendering distortion that compromised color-coded railway signaling, and intense upward light spill causing severe disability glare for locomotive drivers.
Today, as Class I railroads across North America, trans-Eurasian rail operators, and burgeoning mining freight corridors across Australia and Africa overhaul their logistics hubs, demand for modernized high mast lighting systems has surged. The contemporary rail yard environment requires uniform horizontal and vertical illuminance across multi-track trackbeds. Workers coupling cars, inspecting brake lines, and operating remote shunt engines require glare-free optical clarity at track level, while gantry crane operators require clear sightlines across stacked intermodal container lanes.
Intermodal Rail Depots
Demands high mounting elevations (30m - 40m) to clear automated rail-mounted gantry (RMG) cranes, casting uniform vertical illuminance along container stack aisles without blinding top-pick container operators.
Gravity Hump Yards
Dynamic sorting zones where decoupled freight cars roll downhill through automated retarders into classification tracks. Requires zero shadow pockets and high-speed optical uniformity to track car separation.
Trackside Maintenance Facilities
Locomotive running sheds and bogie turnaround pits require precision forward-throw asymmetrical floodlighting, providing over 150 lux of vertical illuminance on wheelsets and undercarriages.
Engineering Standards for Rail Yard High Mast Luminaires
How China's leading specialized OEM factories manufacture heavy industrial high masts engineered to eliminate disability glare, survive cyclonic wind shear, and withstand persistent ground-transmitted vibration.
1. Photometric Distribution & Glare Mitigation (GR Management)
In railway shunting operations, an approaching train driver or ground switcher look down track corridors directly toward light sources. If the luminaires emit uncontrolled high-angle candela (above 70° from nadir), severe veiling luminance occurs. This temporary blindness or reduction in contrast can cause operators to misread wayside switch signals or overlook track personnel.
Our dedicated rail yard floodlighting systems leverage custom asymmetric TIR (Total Internal Reflection) PMMA optical lenses combined with physical internal louvers and visor cutoffs. This engineering yields an absolute cutoff above 75°, driving disability glare down below $GR = 42$ even when luminaires are aimed across an 18-track classification yard.
| Rail Operational Zone | Standard Horizontal Lux ($E_h$) | Standard Vertical Lux ($E_v$) | Uniformity Ratio ($U_o = E_{min}/E_{avg}$) | Max Glare Rating ($GR_{max}$) |
|---|---|---|---|---|
| Hump Yard Apex & Retarders | 30 – 50 Lux | 15 – 25 Lux | ≥ 0.40 | ≤ 45 |
| Classification Tracks (Body) | 15 – 25 Lux | 10 – 15 Lux | ≥ 0.30 | ≤ 50 |
| Coupling / Shunting Switch Points | 30 – 50 Lux | 20 – 30 Lux | ≥ 0.40 | ≤ 45 |
| Intermodal Gantry Aisle (RMG) | 50 – 100 Lux | 30 – 50 Lux | ≥ 0.50 | ≤ 45 |
| Locomotive Inspection Pits | 150 – 200 Lux | 100 – 150 Lux | ≥ 0.60 | ≤ 40 |
2. Structural Steel Metallurgy & Dynamic Vibration Mitigation
A crucial risk factor distinct to railway environments is low-frequency mechanical vibration transmitted through track ballast during heavy freight train transit (often reaching axle loads of 30 to 35 tonnes). Standard commercial lighting poles experience rapid fastener loosening, weld fatigue at the pole base flange, and premature fixture component failure.
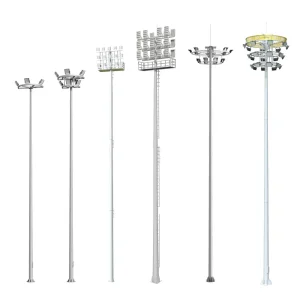
Our manufacturing complex fabricates polygonal (12-sided, 16-sided, or 20-sided) tapered steel shafts utilizing certified high-yield Q355B or Q460 structural steel plate. Longitudinal welds are executed with multi-pass submerged arc welding (SAW) providing 100% penetration along critical stress joints. Finite Element Analysis (FEA) is utilized to simulate vortex-induced vibration (VIV) and gust wind load conditions in accordance with AASHTO LTS-6 and EN 40 standards.
ASTM A123 Hot-Dip Galvanizing
Total immersion in molten zinc baths at 450°C creates an iron-zinc alloy metallurgical bond exceeding 86–100 μm in coating thickness, providing 25+ years of active cathodic protection against sulfur dioxide and diesel engine exhaust fumes.
Positive Mechanical Latching
Winch-operated lowering systems feature dual mechanical latch pins that lock the luminaire ring securely into the masthead top flange, unloading the stainless steel wire hoisting cables from tension during normal service.
Vibration-Damped Optical Heads
LED driver compartments utilize vibration-isolated elastomeric grommets and aircraft-grade safety cable tethers tested to withstand 3G continuous sinusoidal sweep vibration without fatigue fracture.
Submerged Arc Welded Base Flanges
Heavy gusset-reinforced base plates (thickness 25mm to 45mm) welded with complete structural penetration to resist cyclic overturning bending moments from extreme crosswinds.
Raising & Lowering (R&L) Systems vs. Fixed Platform Towers
A critical engineering decision for rail yard project directors: balancing initial capital expenditure against trackside maintenance safety and track possession logistics.
Motorized Raising & Lowering (R&L) Masts
Operational Architecture: Incorporates an internal electro-mechanical winch system, multi-drum aircraft cable assembly, and self-docking ring with automatic electrical power disconnect.
- Track Safety: Maintenance is executed safely at ground level by 1–2 technicians; eliminating cherry pickers and bucket trucks between operational rail tracks.
- Zero Track Possession: Eliminates the costly need to apply for track downtime or de-energize overhead catenary wiring during luminaire servicing.
- Integrated Fail-Safes: Equipped with bidirectional mechanical limit switches, dynamic rope slack sensors, and redundant fall arrest pawls.
Ideal Deployment: Tight switch yards, inter-track aisles, and multi-track switching corridors where vehicle clearance is restricted.
Fixed Platform Head-Frame Masts
Operational Architecture: Rigid steel platform featuring safety guardrails, internal or external caged climb ladders, and fall-arrest vertical lifeline systems conforming to OSHA / EN 353-1.
- Heavy Payload Capacity: Capable of accommodating up to 24x 1200W high-output LED floodlights, optical telemetry cameras, Wi-Fi mesh transceivers, and anemometers.
- Mechanical Simplicity: Zero moving mechanical parts, cables, or winches, delivering maximum structural resilience in corrosive coastal terminals.
- Rigid Optical Aiming: Fixtures remain locked into exact photometric coordinate aiming angles without displacement over time.
Ideal Deployment: Yard perimeters, intermodal container crane boundaries, and heavy maintenance depot exterior gates.
Localized Engineering Solutions Across Global Climate Extremes
From the freezing permafrost of northern trans-continental corridors to the high-salinity coastal marine yards of Southeast Asia and Middle Eastern desert dust storms.
Sub-Zero Alpine & Permafrost
Location Focus: Central Asia, Eastern Europe, Northern Canada.
Engineering Adaptation: Pole shafts engineered from low-temperature impact resistant steel (Q355D/E with Charpy V-notch impact toughness tested down to -40°C). Winch lubricants feature aerospace synthetic low-temp greases preventing mechanical lockup. Luminaire drivers rated to -50°C cold-start.
High Salinity Coastal Intermodal
Location Focus: Deep-water ports, maritime container rail yards.
Engineering Adaptation: Dual duplex coating: ASTM A123 hot-dip galvanizing underlayer topped with an electrostatic thermoset fluorocarbon (PVDF) powder coat to resist C5-M extreme marine corrosive attack. All hardware, winch cables, and junction enclosures specified in 316 marine stainless steel.
Arid High-Temperature Deserts
Location Focus: GCC Middle East, North Africa, Central Australia.
Engineering Adaptation: Luminaire housing features ultra-fin heat sink aerodynamics preventing sand accumulation. Driver compartments isolated with thermal thermal-break insulation plates. Fixtures rated for ambient operating temperatures up to +55°C with IP66/IP67 ingress protection against fine particulate sand infiltration.
High Seismic & Typhoon Corridors
Location Focus: Pacific Rim, Southeast Asia, South America.
Engineering Adaptation: Widened foundation anchor bolt pitch diameters with Grade 8.8 or 10.9 high-tensile anchor rods embedded deep in mass concrete. Pole shafts designed with heavier wall profiles (6mm to 12mm thickness) calculated to resist gusts up to 240 km/h (Category 5 hurricane threshold).
The Evolution of Intelligent Rail Yard Infrastructure
High mast towers are transforming from isolated passive lighting supports into connected digital nerves for autonomous yard logistics, safety tracking, and automated asset inspection.
Machine Vision & Wagon Tracking
High mast crowns mounted at 35m offer clear elevated perspectives. Integration of high-resolution AI edge cameras enables continuous optical automatic container code recognition (ACCR) and rolling stock defect inspection as trains pull through yard necks.
Dynamic Adaptive Dimming (DALI-2 / Zhaga)
Radar and infrared tracking sensors feed real-time activity metrics to an IoT central command gateway. Empty track clusters automatically dim to 20% standby output, instantly scaling to 100% illumination upon incoming train block detection, yielding an extra 30% power savings.
Cloud-Linked Structural Health (SHM)
Integrated MEMS accelerometers and tilt sensors on the masthead stream deflection and resonant frequency data to cloud maintenance twins. Predictive alerts notify infrastructure managers of anchor bolt loosening or foundation soil displacement prior to critical failure.
Frequently Asked Rail Yard Lighting Engineering Questions
Detailed technical responses addressing tender specifications, structural safety, compliance standards, and procurement processes for global railway authorities.
Integrated Lighting & Power Infrastructure Systems
Explore our complete export range including off-grid solar luminaires, high-load municipal columns, and low-voltage power distribution poles engineered for harsh operating environments.