Featured Infrastructure & Lighting Pole Series
Directly manufactured from our 100,000 m² automated facility in Jiangsu. Engineered to meet rigid EN, ASTM, and AASHTO global tender compliance standards.
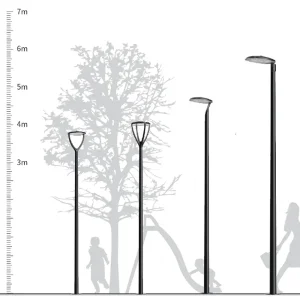
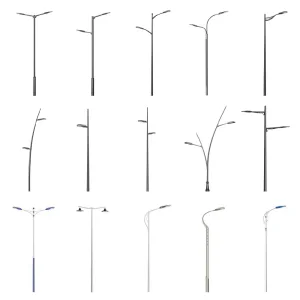
1. Technical Deep-Dive: Structural Mechanics & Metallurgical Engineering
In modern civil and municipal engineering, structural poles must satisfy complex aeroelastic, static, and dynamic stress criteria. Octagonal lighting poles represent an optimal mathematical equilibrium between manufacturing feasibility and structural load-bearing capacity. Unlike circular or cylindrical poles, an octagonal geometry provides eight longitudinal bending folds, significantly boosting the section modulus ($Z$) and moment of inertia ($I$) along key principal axes without increasing steel wall thickness.
Aerodynamic Drag & Vortex Shedding
Square cross-sections exhibit a high drag coefficient ($C_d \approx 1.2$ to $2.0$) and generate destructive von Kármán vortex street vibrations under high wind shear. Octagonal profiles reduce $C_d$ to approximately 0.75 – 0.85 by interrupting vortex synchronization, minimizing wind-induced fatigue at the pole base and welding joints.
Cross-Sectional Stress Distribution
The eight cold-formed longitudinal bends induce strain hardening along the outer boundaries, raising local yield strength ($f_y$). Under combined lateral wind load ($P_w$), luminaire dead weight ($G$), and dynamic torque ($T$), stress is evenly distributed across the octagonal perimeter, preventing local plate buckling.
Optimized Strength-to-Weight Ratio
By transitioning from low-strength round pipe to high-grade cold-formed steel (Q355B / S355JR), octagonal structures achieve a 18% to 25% weight reduction while maintaining identical wind-deflection limits. This yields massive freight savings during cross-border maritime container transit.
Engineering Insight: Steel Grade Selection Criteria (Q235B vs. Q355B / ASTM A572 Gr 50)
Selecting the appropriate structural steel chemical composition is paramount to preventing brittle fracture under extreme ambient temperatures. For standard municipal lighting (3m to 12m), Q235B steel ($f_y \ge 235 \text{ MPa}$, $f_u = 370\text{--}500 \text{ MPa}$) provides excellent ductility and weldability. For heavy-load applications, high wind corridors (>160 km/h), or high mast installations (15m to 40m), Q355B / Q355D steel ($f_y \ge 355 \text{ MPa}$, equivalent to ASTM A572 Grade 50 or EN 10025 S355JR) is standard, providing superior low-temperature impact toughness (Charpy V-notch energy $\ge 27 \text{ J}$ at $-20^\circ\text{C}$).
Steel Specification & Mechanical Parameter Comparison
| Steel Grade | Equivalent Standard | Yield Strength $f_y$ (MPa) | Tensile Strength $f_u$ (MPa) | Elongation $A_5$ (%) | Recommended Applications |
|---|---|---|---|---|---|
| Q235B | GB/T 700 / EN S235JR | $\ge 235$ | $370 - 500$ | $\ge 26$ | Urban residential streets, pedestrian walkways, low-height solar poles (<8m) |
| Q355B | GB/T 1591 / EN S355JR | $\ge 355$ | $470 - 630$ | $\ge 22$ | Highways, major arterials, coastal cyclone regions, split-type solar poles |
| Q355D | ASTM A572 Gr 50 / S355J2 | $\ge 355$ | $470 - 630$ | $\ge 22$ | Sub-zero arctic infrastructure, high-altitude alpine highways, heavy traffic gantries |
| Q460C | GB/T 1591 / S460N | $\ge 460$ | $550 - 720$ | $\ge 17$ | Super high-mast lighting towers (>35m), port container yard floodlighting masts |
2. Precision Manufacturing Roadmap & Anti-Corrosion Metallurgy
Producing world-class octagonal lighting poles requires strict control over raw coil uncoiling, CNC plasma cutting, multi-point press braking, automated longitudinal seam submerged-arc welding (SAW), and complete hot-dip galvanizing immersion.
1. Precision CNC Cutting & Single-Seam Forming
High-precision CNC plasma and laser cutting machines slice trapezoidal steel sheets with structural taper tolerances within $\pm 1.0\text{ mm}$. A 2000-Ton CNC hydraulic tandem press brake presses the plate through 7 precise bending operations to yield an accurate octagonal cross-section with a single longitudinal joint seam.
2. Submerged Arc Welding (SAW) & NDT Inspection
The formed octagonal tube passes through automated longitudinal welding mills utilizing gas metal arc or submerged arc welding (AWS D1.1 standard). Continuous penetration welds are verified via Non-Destructive Testing (NDT)—including Ultrasonic Testing (UT) and Magnetic Particle Inspection (MT)—to guarantee structural integrity under dynamic wind shear.
3. Hot-Dip Galvanizing per BS EN ISO 1461 / ASTM A123
After surface degreasing, acid pickling, and fluxing, poles are fully submerged into a molten zinc bath at $450^\circ\text{C}$. Metallurgical reaction creates intermetallic Zinc-Iron alloy layers ($\Gamma, \delta, \zeta$) covered by a pure zinc outer layer ($\eta$). Average coating thickness ranges from $85\text{ }\mu\text{m}$ to $120\text{ }\mu\text{m}$, offering 25+ to 50 years of maintenance-free anti-corrosion protection in atmospheric environments (ISO 12944 C3–C5 categories).
4. Electrostatic Thermosetting Powder Coating
For architectural compliance and harsh marine installations, an optional duplex system applies an architectural-grade polyester powder coating ($80\text{--}120\text{ }\mu\text{m}$) over the galvanized surface. The coating undergoes 3,000 hours of neutral salt spray testing (ASTM B117) without blistering, cross-hatch flaking, or gloss degradation.
3. Macro-Industry Solutions & Sector Integration
Octagonal steel poles serve as critical physical nodes across municipal, transportation, power distribution, and smart city infrastructure projects. Customization capabilities accommodate diverse dynamic load profiles, accessory mountings, and extreme geographical environments.
Highway & Expressway Transport Corridors
Compliant with AASHTO Standard Specifications for Structural Supports for Highway Signs, Luminaires, and Traffic Signals. Engineered for 8m to 14m heights, single or double curved arms, with crashworthy breakaway base-plate designs that absorb dynamic vehicle impacts to reduce passenger fatality rates.
Smart City & 5G IoT Multifunctional Hubs
Octagonal smart poles serve as structural backbones for urban digitisation. Internal cabling channels and dedicated access doors house 5G micro-base stations, CCTV surveillance cameras, environmental sensors, public Wi-Fi APs, and emergency call buttons without compromising structural load margins.
Seaports, Airports & High Mast Logistics Nodes
Heavy-duty 15m to 40m octagonal polygonal towers with automated, motorized head-frame raising and lowering systems. Designed to illuminate expansive container terminals, apron zones, and stadium complexes while withstanding hurricane-force wind velocities up to $250\text{ km/h}$.
Urban Grid Low-Voltage Steel Power Distribution
Engineered to replace fragile concrete utility poles, tubular steel octagonal power distribution poles support low-voltage overhead conductor spans, transformers, and distribution cross-arms, featuring superior bending stiffness against heavy conductor tension and icing loads.
4. China Factory 4.0: Supply Chain Resilience & Scale
Our 100,000 m² state-of-the-art facility in Gaoyou, Jiangsu combines vertical raw material sourcing, automated CNC manufacturing lines, and stringent ISO quality control gates to protect global EPC contract delivery schedules.
Upstream Steel Hedging & Capacity Guarantee
Direct raw material partnerships with premier steel conglomerates (Baosteel, Shougang Group) ensure immediate access to prime-certified steel coils. Direct hedging buffers international procurement teams against spot market price volatility during large-volume tenders.
Sub-Assembly Quality Control & Traceability
Every single octagonal lighting pole is stamped with a unique QR code and production lot ID. Inspection records track raw material Mill Test Certificates (EN 10204 3.1), weld NDT logs, galvanizing thickness readings, and final visual inspection sign-offs before container packing.
Logistics & Container Packing Optimization
Custom nesting algorithms organize tapered octagonal poles inside 40ft High Cube (40HC) containers, maximizing weight and volume efficiency. Wrapped in protective bubble sheets or woven fabric bundles, poles arrive at destination ports free of galvanizing abrasions or shipping damage.
5. Global Enterprise Procurement & Tender Specification Framework
Engineers of Record (EOR), municipal procurement officers, and EPC contractors require fully compliant tender submittals. Below is the standard engineering documentation framework supplied with XINTONG tender packages:
1. CAD Structural & Base-Plate Drawings
Detailed structural engineering drawings covering shaft height, top/bottom cross-sectional diameter, wall thickness, door opening reinforcement, base plate dimensions, and anchor bolt pitch circle diameter (PCD).
2. Finite Element Analysis (FEA) & Wind Load Reports
3D FEA stress simulations verifying pole deflection limit states under project-specific basic wind speeds ($V_{3s} = 30\text{--}70 \text{ m/s}$) per AASHTO LTS-6 or EN 40-3-1 standards.
3. DIALux Photometric Lighting Simulation
Integrated photometric calculation report matching octagonal pole height, arm tilt angle, overhang distance, and LED fixture optical distribution against target road lux and uniformity ($U_0, U_1$) metrics.
4. Quality & Mill Test Certificates (MTC)
Raw material test certificates per EN 10204 3.1 detailing chemical analysis (C, Si, Mn, P, S) and mechanical strength testing, alongside hot-dip galvanizing coating thickness test reports.
Tender Proposal Checklist for Overseas Engineering Buyers
When submitting a Request for Quotation (RFQ), please provide: 1) Mounting height ($H$) & quantity; 2) Local design wind speed ($\text{m/s}$ or $\text{km/h}$); 3) Luminaire weight and effective projected area (EPA); 4) Single/double arm projection length and tilt angle; 5) Surface coating preference (Galvanized only or HDG + Powder Coating); 6) Target delivery port.
6. Localized Engineering Support & Technology Roadmap (2025–2035)
Localized Engineering Support & Compliance
Navigating country-specific civil engineering codes can delay tender execution. XINTONG maintains a dedicated overseas project support division staffed by structural engineers experienced in regional certifications:
- Middle East (GCC): SASO, MOT, and SEC regional storm and extreme heat resilience standards.
- Southeast Asia: Tropical cyclone wind load calculations and high humidity marine saline protection.
- Americas & Caribbean: AASHTO LTS-6, ASTM A123 galvanizing, and ASTM A572 steel compliance.
- Europe & Central Asia: CE marking compliance, EN 40 structural design criteria, and S355JR structural steel certifications.
Technology Roadmap: The Next Decade of Lighting Poles
The humble street lighting pole is undergoing a profound technological transformation into intelligent micro-infrastructure:
- Ultra-High-Strength Steels: Transitioning to Q460 and Q690 steels to further reduce steel consumption and carbon footprint during production.
- Integrated Kinetic & Flexible Solar PV: Wrapping octagonal shafts with flexible CIGS or monocrystalline solar modules for seamless off-grid power generation without external brackets.
- Digital Twin & SHM Sensors: Installing micro-strain gauges and tilt sensors inside access doors for real-time Structural Health Monitoring (SHM) during extreme wind events.
7. Frequently Asked Questions (Technical & Procurement FAQ)
Expert answers to technical engineering and procurement queries regarding octagonal lighting poles and factory manufacturing standards.
XINTONG is a direct manufacturing group established in 1999. We operate a 100,000 m² heavy manufacturing facility in Gaoyou, Jiangsu Province, China. Our plant houses 7 full production lines covering steel sheet shearing, CNC tandem press bending, continuous submerged-arc welding, hot-dip galvanizing, electrostatic powder coating, and LED / solar system assembly. Global clients are welcome to perform on-site factory audits or request live video facility inspections.
Octagonal lighting poles offer distinct structural advantages over round conical poles. The eight longitudinal cold-formed bends induce strain hardening along the corners, raising local yield strength ($f_y$). This octagonal cross-section provides a higher section modulus ($Z$) against directional wind shear while interrupting vortex shedding, effectively reducing wind-induced vibration and fatigue at the base plate weld joint.
Our octagonal lighting poles are designed, fabricated, and galvanized in accordance with major international standards, including:
- Structural Design: EN 40-3-1 / EN 40-3-3, AASHTO LTS-6, GB 50017.
- Steel Material: EN 10025 (S235JR, S355JR), ASTM A572 Grade 50, GB/T 700 / GB/T 1591.
- Welding Quality: AWS D1.1 / EN ISO 15614 (Submerged Arc Welding).
- Galvanizing: BS EN ISO 1461, ASTM A123 / A123M.
For extreme corrosive environments (ISO 12944 C4/C5 marine categories), poles undergo complete internal and external hot-dip galvanizing with a zinc coating thickness exceeding $100\text{ }\mu\text{m}$. Furthermore, we apply a Duplex Protective System by adding an architectural-grade electrostatic polyester powder coating ($80\text{--}120\text{ }\mu\text{m}$) cured at $200^\circ\text{C}$. This double-layer system yields a maintenance-free service life exceeding 30 to 50 years.
Our structural engineering team requires: 1) Required pole mounting height ($H$); 2) Design maximum wind speed (3-second gust speed in $\text{m/s}$ or $\text{km/h}$); 3) Total weight and Effective Projected Area (EPA in $\text{m}^2$) of luminaires or equipment to be mounted; 4) Arm length projection and quantity; 5) Soil condition parameters for foundation anchor bolt calculations.
Every shipment includes a comprehensive Quality Quality Dossier: Mill Test Certificates (MTC EN 10204 3.1) verifying steel chemical and mechanical properties, Non-Destructive Testing (NDT) weld reports, magnetic coating thickness test records for galvanizing, dimensional inspection sheets, and factory certificate of compliance.
Comprehensive Product Catalog & High Mast Series
Explore our full range of customizable lighting poles, high mast floodlighting systems, and smart urban power distribution poles.