Featured Light-Duty Galvanized Distribution Poles & Modular Mast Systems
Precision-fabricated in our 100,000 m² Gaoyou facility. Fully compliant with international electrical and municipal tenders, integrating hot-dip galvanizing for up to 30 years of maintenance-free service.
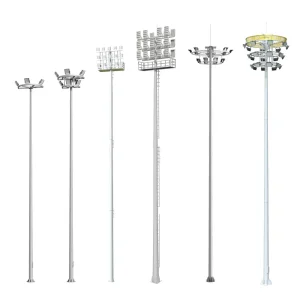
OEM PUBLIC TRANSIT Series Municipal High Mast Poles Manufacturers, Supplier
Explore Technical Specs
Best XT-DT-1 Series (Split Type) Manufacturer, Factories
Explore Technical Specs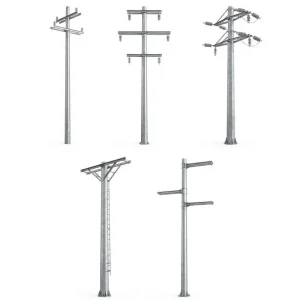
High-Quality URBAN-GRID Series Urban Low Voltage Steel Power Distribution Poles Suppliers, Factories
Explore Technical Specs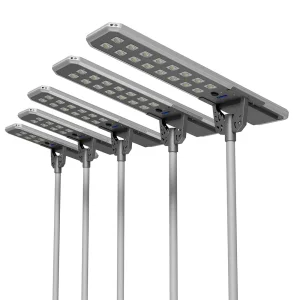
OEM XT-YTH-9 Series (All-In-One) Factory, Factories
Explore Technical Specs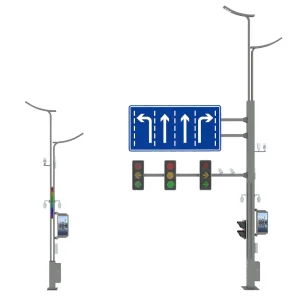
OEM XINTONG Multifunctional Light Poles Integrated Design, Octagonal, Conical & Square Poles For Smart City Engineering Supplier, Factory
Explore Technical Specs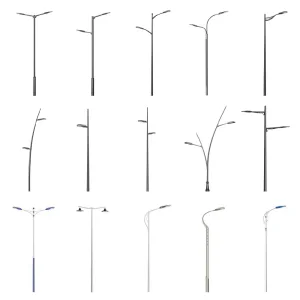
Custom XINTONG Full Series Municipal Street Light Poles Conical, Octagonal & Customizable Poles for Municipal Engineering Factory, Factories
Explore Technical Specs
OEM AIRPORT-PORT SERIES High Mast Light Manufacturer, Supplier
Explore Technical Specs
Buy XINTONG Municipal Street Light Pole Series Factories, Exporter
Explore Technical SpecsGlobal Energy Transition: Transforming Low-Voltage Distribution Grids
Examining the structural evolution from wood and pre-stressed spun concrete poles to modular, thin-walled polygonal galvanized steel utility systems across global distribution networks.
Grid Modernization & Hardening
Global utility operators are phasing out chemical-treated timber (creosote/CCA) due to environmental regulations and fire vulnerabilities. Tapered octagonal and dodecagonal steel power poles provide predictable ductility, uniform yield strengths ($F_y = 355\text{ MPa}$), and zero rot deterioration during extreme storm loading.
Total Life-Cycle CapEx Optimization
Light-duty steel utility poles weigh approximately one-third of equivalent pre-stressed spun concrete poles. This substantial mass reduction cuts ocean shipping freight charges, slashes inner-country transport tariffs, and enables direct installation via light excavation hoists without requiring heavy crawler cranes.
Multi-Utility Smart Infrastructure
The contemporary power grid demands integrated co-location. Modern light-duty galvanized poles function as joint-use physical assets, simultaneously carrying low-voltage (0.4kV–33kV) conductors, optical-ground ADSS lines, solar micro-generation arrays, and telecommunication micro-cells without structural resonance.
Structural Architecture, Cross-Section Mechanics & Steel Selection
Detailed material properties, cross-sectional geometry, and non-linear yield parameters governing Yangzhou Xintong Traffic Equipment Group Co., Ltd.'s light-duty galvanized power pole production lines.
Light-duty galvanized power poles represent a critical structural category in utility transmission and municipal distribution systems, filling the capacity spectrum between conventional lighting standards and heavy angle-lattice transmission towers. Operating typically across system voltages from 400V secondary reticulation up to 34.5kV/35kV intermediate sub-transmission feeders, these single-shaft tubular structures must endure complex combined loading regimes: dead-weight gravitational loads from phase conductors, cross-arms, and line insulators; lateral wind-pressure vectors on both the pole envelope and aerial cables; longitudinal unbalanced tension during conductor break incidents; and secondary P-Delta geometric deflections.
Technical Design Standard Compliance: Xintong steel power structures are computed and verified using finite-element numerical modeling in accordance with ASCE Manual of Practice No. 72 (Design of Steel Transmission Pole Structures), ANSI C136.20, BS EN 40-3, and AASHTO Standard Specifications for Structural Supports for Highway Signs, Luminaires, and Traffic Signals.
| Structural Parameter | Light Duty Standard Class | Intermediate Feeder Class | Reinforced Heavy Corridor | Evaluation Norm |
|---|---|---|---|---|
| Nominal Height Spectrum (m) | 6.0 m – 9.0 m | 10.0 m – 12.0 m | 13.0 m – 18.0 m | Project Specific / Custom |
| Structural Steel Grade | Q235B (ASTM A36 Equiv.) | Q355B (ASTM A572 Gr 50) | Q355D / Q420B High-Yield | EN 10025-2 / GB/T 1591 |
| Minimum Yield Strength ($R_e$) | $\ge 235 \text{ N/mm}^2$ | $\ge 355 \text{ N/mm}^2$ | $\ge 420 \text{ N/mm}^2$ | ISO 6892 Tensile Testing |
| Cross-Sectional Geometry | Octagonal / Conical Tapered | Dodecagonal (12-sided) | Hexadecagonal (16-sided) | Single-seam longitudinal weld |
| Shaft Taper Ratio | 11 mm/m to 14 mm/m | 12 mm/m to 15 mm/m | 13 mm/m to 18 mm/m | Continuous automated press |
| Shaft Wall Thickness | 3.0 mm – 4.0 mm | 4.5 mm – 6.0 mm | 6.0 mm – 10.0 mm | Ultrasonic Thickness Tested |
| Base Connection Topology | Direct Embedment / Flange | Anchored Flange Base Plate | High-Tensile Base Ring (42CrMo) | ASTM A563 / ISO 898-1 |
| Galvanizing Thickness | $\ge 86 \ \mu\text{m}$ ($610\text{ g/m}^2$) | $\ge 100 \ \mu\text{m}$ ($710\text{ g/m}^2$) | $\ge 120 \ \mu\text{m}$ ($860\text{ g/m}^2$) | ISO 1461 / ASTM A123 |
The manufacturing process at Xintong utilizes computerized 14-meter tandem CNC press brakes to fold premium hot-rolled coil structural plates into polygon forms. By choosing octagonal or 12-sided polygonal sections over round cross-sections, the structure attains significantly higher moments of inertia ($I_{xx}$) along primary directional planes while generating aerodynamic vortex disruption that suppresses destructive Karman vortex-induced vibrations (VIV) during high-laminar wind exposure.
Hot-Dip Galvanization Science: Microstructure & Duplex Longevity
How chemical bath controls and intermetallic iron-zinc diffusion layers provide multi-decade barrier and sacrificial cathodic protection across corrosive ISO 12944 atmospheric tiers.
Intermetallic Fe-Zn Diffusion
Upon submerging pickled and fluxed steel shafts into our $450^\circ\text{C}$ molten zinc bath, metallurgical reaction generates distinct iron-zinc alloy layers: Gamma ($\Gamma$, 75% Zn, 25% Fe), Delta ($\delta_1$, 90% Zn, 10% Fe), Zeta ($\zeta$, 94% Zn, 6% Fe), and the outer ductile Eta ($\eta$, 100% Zn) phase, achieving chemical bonding far superior to mechanical paint adhesion.
Cathodic Sacrificial Shielding
Should the outer zinc layer experience localized mechanical scratching during installation or cable-stringing operations, zinc's lower electrochemical potential ($E^\circ = -0.76\text{ V}$) relative to iron ($E^\circ = -0.44\text{ V}$) ensures that zinc corrodes sacrificially, preserving structural steel core integrity even in wet, ion-dense soils.
Duplex Electrostatic Finishing
For high-salinity marine interfaces (ISO 12944 Category C5-M) or severe industrial sulfur exposures (C4/C5-I), Xintong applies a secondary electrostatic polyester powder coat (80–120 $\mu\text{m}$) over sweep-blasted galvanizing. This duplex barrier multiplies protection longevity through a 1.5× to 2.3× synergy factor over single-coat coatings.
Full Traceability, Tender-Ready Submittals & Factory Auditing
Navigating complex international EPC qualification requirements with complete material origin tracking, rigorous NDT weld testing, and factory acceptance procedures.
Traceable Mill Certificates
Every steel batch arrives with primary EN 10204 Type 3.1 inspection documentation tracking carbon equivalent (CEV), silicon content (under 0.04% or 0.15%–0.25% to eliminate Sandelin reactivity), and Charpy V-notch impact toughness.
Non-Destructive Testing (NDT)
Shaft longitudinal seam welds are submerged-arc welded and subjected to ultrasonic testing (UT) and magnetic particle testing (MT) per AWS D1.1 structural welding code to ensure defect-free penetration and zero inclusions.
Full-Scale Proof Deflection
Equipped with horizontal hydraulic proof-test rigs capable of simulating maximum design cantilever tip load, measuring temporary plastic strain, elastic return, and ultimate moment capacity for client acceptance testing.
Logistical Slip-Joint Nesting
Poles intended for deep export are engineered with precision telescoping slip-joints (1.5× mating diameter tolerance). This allows multi-section packaging inside standard 40-foot High Cube (40HC) ocean containers, minimizing ocean freight rates.
Engineered Implementations Across Global Utility Topologies
Case studies and environmental adaptation strategies deployed by Xintong engineers across distinct climate and geological regimes.
Typhoon & Coastal Corridors
Deployment: Southeast Asia island distribution lines.
Challenge: Category 5 cyclonic gusts ($V_{\text{gust}} > 60\text{ m/s}$) paired with severe marine saline mist.
Solution: Dodecagonal Q355B steel shafts with upgraded base-plate gussets and $120\mu\text{m}$ thick hot-dip zinc coatings resistant to persistent chloride pitting.
Desert Electrification Networks
Deployment: Middle East & North Africa (MENA).
Challenge: Daily thermal swings from $0^\circ\text{C}$ to $+55^\circ\text{C}$ accompanied by severe airborne silica abrasive wear.
Solution: Direct-burial shafts with heavy polyurethane subterranean coatings and specialized internal cable heat-dissipation ventilation slots.
Permafrost & Seismic Zones
Deployment: Central Asia & Andean Highlands.
Challenge: Low ambient temperatures (down to $-40^\circ\text{C}$) generating cold-shortness brittle risks and frost heave foundation upheaval.
Solution: Charpy V-notch tested Q355D steel retaining impact energy $\ge 27\text{ Joules}$ at $-20^\circ\text{C}$ to $-40^\circ\text{C}$, coupled with self-anchoring helical steel foundation plates.
Narrow Urban Utility Right-of-Way
Deployment: Densely built metropolitan downtowns.
Challenge: Narrow sidewalk corridors prohibiting spread guy wires, requiring compact self-supporting structures.
Solution: High-moment capacity flanged base poles mounted to bored micro-piles, accommodating underground cable ingress via internal handholes.
Technological Roadmap: The Evolution of Intelligent Steel Poles
Pioneering smart-grid physical assets, ultra-high-strength green steel alloys, and predictive health monitoring for mission-critical infrastructure.
Low-Carbon Recycled Steel
Incorporation of Electric Arc Furnace (EAF) steel with certified recycled scrap content $\ge 70\%$, reducing embedded Scope 3 greenhouse carbon intensity per utility pole by 42% relative to blast-furnace routes.
Structural Health Telemetry
Integration of low-power passive surface acoustic wave (SAW) and optical fiber Bragg grating (FBG) strain sensors inside pole apexes, delivering real-time conductor tension and inclination data via LoRaWAN/NB-IoT.
Eco-Zinc-Aluminum Alloys
Transition to Zn-Al-Mg (Zinc-Aluminum-Magnesium) bath chemistries offering 3× the salt-spray resistance of conventional pure zinc coatings, enabling reduced zinc consumption while extending C5-M service lifetime.
Dynamic Thermal Rating (DTR)
Multifunctional smart poles equipped with integrated micro-weather telemetry and conductor temperature sensors, empowering utilities to adjust power line ampacity in real-time based on local wind cooling.
Frequently Addressed Engineering & Procurement Inquiries
Authoritative answers on structural safety factors, foundation engineering, coating standards, and manufacturing lead times.
How does steel pole deflection criteria compare with prestressed concrete?
Under maximum design wind-load conditions, steel poles are engineered to accommodate ductile elastic deflections up to 10%–15% of total shaft height without plastic yielding ($F_y$ remaining within the elastic limit). Concrete poles, conversely, suffer from surface tension micro-cracking when deflections exceed 2%–3%, exposing reinforcing rebar to moisture and accelerated carbonation decay.
What is the standard embedment depth for direct-buried power poles?
Direct embedment depth typically adheres to the standard empirical rule: $10\% \text{ of overall pole length} + 0.6 \text{ meters}$ ($10\% + 2 \text{ feet}$). In unstable or loose sandy soils, depths are adjusted using Broms' or Hansen's lateral soil bearing methods, frequently supplemented with bottom bearing plates or crushed-aggregate backfill.
How is the Sandelin Range controlled during hot-dip galvanization?
Silicon levels between 0.04% and 0.14% can accelerate zinc-iron diffusion excessively, leading to brittle, matte-gray coatings with poor mechanical adhesion. Xintong specifies structural steel heats with low silicon content ($Si \le 0.03\%$) or adds nickel alloy micro-pellets to our molten zinc kettle to suppress rapid phase growth per ASTM A385.
Can low-voltage steel poles accommodate distribution transformers?
Yes. By calculating the eccentric vertical gravitational load and secondary bending moments, Xintong fabricates factory-welded mounting channels or transformer platform brackets capable of bearing 25kVA to 167kVA single-phase or three-phase pole-mounted distribution transformers (pole weight capacities rated up to 1,500 kg eccentric load).
What grounding and lightning dissipation provisions are standard?
Every pole section features a welded, corrosion-resistant stainless steel or copper-faced M12/M16 grounding nut located 300 mm above the base plate or ground line. Internal grounding conductor paths run unobstructed down through the pole interior, shielding earthing lines from external physical theft.
What documentation accompanies an international export shipment?
Standard export submittal packets include: Mill Test Certificates (MTC) to EN 10204 3.1, Hot-Dip Galvanizing Inspection Thickness Reports (ASTM A123/ISO 1461), Ultrasonic NDT Weld Test Certifications, Finite Element Design Calculation Sheets (signed by qualified structural engineers), and Packing List Nesting Diagrams.
Full Series Power Distribution, Decorative & Heavy-Load Poles
Engineered for diverse utility corridors, municipal roads, and extreme condition applications worldwide.
OEM XINTONG Multifunctional Light Poles Integrated Design, Octagonal, Conical & Square Poles For Smart City Engineering Supplier, Factory
Review Engineering Drawings
Custom XINTONG Full Series Municipal Street Light Poles Conical, Octagonal & Customizable Poles for Municipal Engineering Factory, Factories
Review Engineering Drawings
OEM AIRPORT-PORT SERIES High Mast Light Manufacturer, Supplier
Review Engineering Drawings
Buy XINTONG Municipal Street Light Pole Series Factories, Exporter
Review Engineering Drawings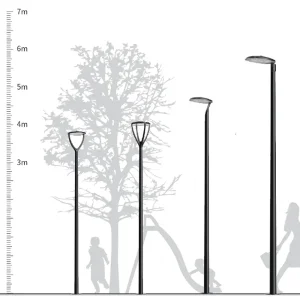
Best Series Decorative Street Light Pole Manufacturers, Manufacturer
Review Engineering Drawings
Custom XINTONG High Strength Light Pole Series: Engineered for Extreme Conditions & Heavy Loads Manufacturers, Factories
Review Engineering Drawings
Buy XT-YTH-3 Series (All-In-One) Exporter, Exporters
Review Engineering Drawings