High Mast & Specialized Infrastructure Portfolio
Explore heavy-load polygonal towers, transit lighting structures, and proprietary lifting apparatus trusted by municipal engineers across 80+ nations.
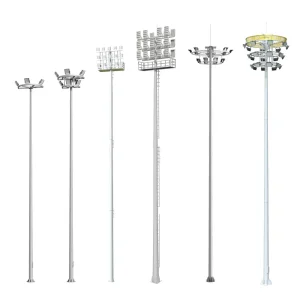
Global State of High Mast Winch Systems & Raising-Lowering Technology
Strategic analysis of mechanized lighting maintenance, mechanical failsafes, and the procurement imperatives shifting infrastructure projects toward China's leading manufacturing clusters.
Zero-Working-at-Height Safety Directives
Global civil aviation authorities (ICAO, FAA) and maritime logistics agencies now enforce strict zero-climb policies on high-traffic hubs. Raising and lowering winch systems eliminate dangerous cherry-picker deployments and rope-access procedures, allowing 18m to 45m luminaire rings to be serviced safely at ground level.
Dual-Drum Self-Sustaining Mechanics
Modern EPC tenders explicitly reject single-cable winches due to catastrophic single-point failure hazards. The engineering standard has transitioned toward dual-drum worm-gear winches with integrated centrifugal brakes and mechanical locks that secure the luminaire carriage independently of continuous cable tension.
Supply Chain Consolidation in China
China has become the global epicenter for integrated high mast fabrication. Facilities like Yangzhou Xintong Traffic Equipment Group combine 100,000 m² of specialized workshops—uniting automated 1600-ton CNC press braking, submerged-arc longitudinal seam welding, deep-bath hot-dip galvanizing, and gear assembly under ISO 9001 governance.
Structural Integrity Insight: The Mechanics of Mechanical Latching vs. Non-Latching Systems
In standard non-latching high masts, wire ropes remain under permanent load for decades, leading to inevitable metallurgical fatigue, creep elongation, and ultimate failure under high crosswinds. Chinese engineering standard GB 50017 along with international standard EN 40 dictate that premium high-mast winch designs must incorporate mechanical latching barrels at the mast-head. Once the ring reaches the top, spring-loaded latch pins engage heavy steel docking collars, transferring 100% of the luminaire weight onto the rigid masthead structure and relieving the stainless steel hoist cables entirely.
Engineering Anatomy of an Industrial High Mast Winch Assembly
Delivering uncompromised structural reliability via precision planetary drive gearing, multi-layer anti-corrosion Metallurgy, and multi-core electrical trailing connections.
Self-Locking Worm & Planetary Reduction
Manufactured using high-tensile phosphor bronze worm gears paired with case-hardened alloy steel worms. The mechanical advantage guarantees irreversible self-locking under sudden power loss, preventing luminaire descent without active motorized or manual input from the operator.
AISI 316 Stainless Steel Wire Ropes
Fitted with dual or triple aircraft-grade 7x19 construction AISI 316 stainless steel flexible wire ropes. Engineered with a minimum safety factor of 5:1 (optionally 8:1 for critical zones), certified according to ISO 2408 and tested for zero internal kink under rotational deflection.
Heavy-Duty Umbilical Power Feeder
Multi-core EPR/CSP insulated trailing electrical cables connect the luminaire ring to the base distribution board. Includes integrated strain-relief steel core wires to prevent copper conductor stretching during raising and lowering cycles, terminating into an IP66 quick-disconnect plug.
| Component Unit | Standard Specification | Heavy-Industrial / Maritime Grade | Compliance Test Benchmark |
|---|---|---|---|
| Winch Gearbox System | Worm Gear Reduction (Ratio 40:1 to 50:1) | Dual-Drum Oil-Bath Self-Locking Worm Gearing | Dynamic Load Test at 150% Rated Capacity |
| Suspension Wire Cables | Hot-Dip Galvanized Aircraft Cable (7x19) | AISI 316 Marine-Grade Stainless Steel Wire Rope | Tensile Rupture Test & Salt Spray (ISO 9227) |
| Mast Head Pulley Block | Cast Aluminum Alloy Sheaves with Sintered Bushings | Deep-Groove Nylon/Stainless Sheaves with Sealed Bearings | Fatigue & Wire Rope Abrasion Resistance Analysis |
| Carriage Latching System | Visual Latch Indicator Pins with Rubber Buffers | Spring-Loaded Mechanical Docking Collars + Proximity Sensors | 10,000 Cycle Lock/Unlock Verification Trial |
| Drive Motor Interface | External Portable Electric Drill (AC 220V/380V) | Integral Flame-Proof Drive Motor with Remote Pendant/Wireless | IP65 Motor Rating & Electronic Torque Limiting |
Engineered Turnkey Solutions for Mission-Critical Environments
Custom structural height, wind survival ratings up to 60 m/s (134 mph), and bespoke luminaire configurations tailored to specialized municipal and industrial sectors.
Seaports, Container Yards & Maritime Docks
Subjected to relentless saline moisture, high humidity, and typhoon-level winds. Our port-series high masts feature 25m to 40m polygonal shafts with minimum 100μm hot-dip galvanizing, internally sealed winches, and stainless-steel hardware engineered to resist C5-M extreme marine corrosion classifications.
International Airports & Aviation Aprons
Must comply with strict ICAO Annex 14 obstacle limitations and sharp glare cutoff restrictions. Winch systems enable rapid luminaire maintenance without interrupting apron logistics or ground support equipment movement. Integrated top-mount obstacle lights automatically re-energize upon carriage docking.
Highway Interchanges & Major Toll Corridors
Continuous vehicle flow prohibits closing lanes for bucket-truck maintenance. High masts installed in central reserve loops or interchange islands utilize automated raising/lowering winches operated from inside the base door compartment, protecting highway maintenance staff completely from ongoing traffic.
Technical Roadmap: Smart Winches & Autonomous Infrastructure
The convergence of industrial automation, smart pole integration, and real-time structural health monitoring in high mast engineering.
IoT Load-Cell Tension Sensing
Next-generation winch drums incorporate digital inline load cells. Real-time telemetry detects asymmetrical cable tension, ice accretion loads, and snag detection during raising/lowering, halting winch operations in milliseconds to avert cable snap events.
Wireless Remote Actuation
Eliminating trailing hardwired control pendants, technicians operate the winch lowering system via encrypted Bluetooth Low Energy (BLE) or industrial RF remotes at a safe standoff perimeter of 30 meters, fully outside the drop-zone shadow.
Autonomous Solar Integration
Hybrid high masts now couple split or all-in-one solar arrays with high mast winches. Specially designed articulating headframes allow solar panels to tilt synchronously with the lighting ring, lowering smoothly for cleaning in dusty desert or mine environments.
Composite Anti-Corrosive Sheaves
Adoption of self-lubricating polymer and ultra-high-molecular-weight polyethylene (UHMW-PE) pulley sheaves minimizes stainless steel cable friction, extending hoist wire operating life cycles past 25 years without external grease re-application.
Factory Rigor: Yangzhou Xintong Production Ecosystem
Vertical control across all manufacturing tiers—from raw plate decoiling to CNC forming, ultrasonic weld testing, and factory acceptance testing (FAT).
Certified Metallurgy (Q235 & Q355B Steel)
All steel sections are sourced exclusively with certified heat-traceable mill sheets. Low-alloy high-strength Q355B (equivalent to ASTM A572 Grade 50 and EN S355JR) provides structural yield strength surpassing 355 MPa, with high Charpy V-notch impact toughness for sub-zero deployments.
Internal & External Hot-Dip Galvanizing
Full-immersion galvanizing conducted in our computerized galvanizing bath according to ASTM A123 and EN ISO 1461. Steel shafts receive a minimum 86μm to 100μm bonded metallurgical zinc layer inside and out, guaranteeing 25+ to 50+ years of rust protection in harsh environments.
Full Tender Documentation & DIALux Design
Global EPC contractors receive turnkey submittal packages: AASHTO wind-load calculations, foundation anchor bolt layouts, finite element stress simulations (FEA), DIALux 3D photometrics, and comprehensive Factory Acceptance Test (FAT) load certificates.
Frequently Asked Questions on High Mast Winch Systems
Authoritative technical responses resolving the primary procurement, safety, and mechanical inquiries posed by international consulting engineers.
In a non-latching system, the luminaire ring remains suspended by the wire ropes 100% of the time, causing continuous stress, rope creep, and vibration fatigue. A latching system employs mechanical docking pins at the masthead. Once hoisted into position, the carriage docks onto structural latches, transferring 100% of the luminaire load to the pole shaft and allowing the hoist cables to be completely unloaded during regular operation.
Our winches use precision self-locking worm gears with high reduction ratios (up to 50:1) combined with centrifugal friction safety brakes. The gears are mechanically non-reversible, preventing unwinding under load. For electric drives, adjustable torque limiters and integrated travel limit switches immediately shut off power if the carriage reaches the masthead or encounters abnormal resistance.
Poles and lifting systems are manufactured strictly under ISO 9001, ISO 14001, and ISO 45001. Structural steel conforms to EN 10025 (S355JR) or ASTM A572 Grade 50. Wind loading calculations follow AASHTO Standard Specifications for Structural Supports for Highway Signs, Luminaires, and Traffic Signals, or EN 40-3. Galvanizing conforms directly to ASTM A123 and EN ISO 1461.
Yes. Every motorized winch assembly features a dual-input shaft. In the event of a power outage or on un-energized job sites, a manual emergency hand-crank clutch connects directly to the high-reduction worm shaft, allowing two technicians to safely raise or lower the lighting ring manually without electrical power.
Infrastructure Series: Luminaires, Smart Columns & High Masts
Ensure tender compliance with our full range of certified municipal poles, high-lumen floodlights, and heavy-duty utility columns.
Global Project Specification Checklist
Ensure your project engineering team captures every critical site variable before issuing high mast winch inquiries.
Mechanical Payload Data
Define total luminaire count, individual fixture weights, luminaire wind-projected surface areas (EPA), and auxiliary attachments such as CCTV PTZ cameras, aviation beacons, or IoT telecommunication antennas.
Environmental Wind Velocity
State 50-year or 100-year recurrence mean basic wind velocities (m/s or km/h), gust response factors according to AASHTO or EN 1991-1-4, topographic elevation indices, and seismic acceleration parameters.
Electrical & Motor Control
Specify utility supply parameters (e.g., 380V 3-Phase, 220V Single-Phase 50Hz/60Hz), internal carriage power split, junction enclosure IP ratings (IP66/IP67), and if portable or integrated electric winch drives are required.