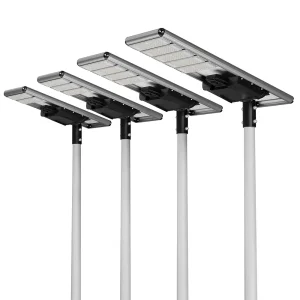
Heavy-Duty Galvanized Iron Poles & Structural Solutions
Precision-engineered octagonal, conical, and high-mast assemblies manufactured to withstand extreme aerodynamic conditions and coastal corrosion environments.
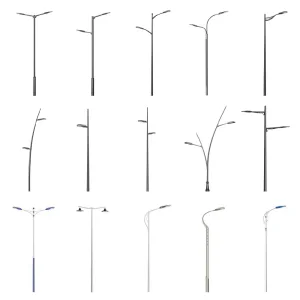
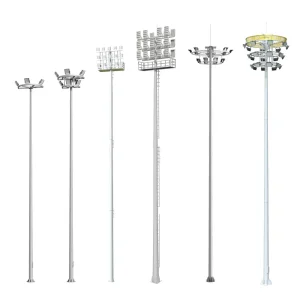
The Evolution of Galvanised Iron Pole Manufacturing
From passive structural illumination supports to connected, aerodynamic, multi-payload smart city backbones: a technical evaluation of manufacturing paradigms.
Metallurgical Innovations & Yield Strength
Traditional mild steel (Q235B) has transitioned toward ultra-high-yield alloyed structural steel (Q355B and ASTM A572 Grade 50). By controlling silicon content below 0.04% or within the Sandelin curve bracket (0.15% to 0.25%), our processing prevents excessive brittle iron-zinc alloy phase growth (Zeta and Delta phases), guaranteeing high ductility and thermal shock resilience during extreme galvanizing thermal cycles.
Corrosion Dynamics in Coastal Corridors
Urban microclimates and maritime industrial zones classified under ISO 12944 C4 and C5 corrosive environments demand protective barriers far beyond basic electroplating. By implementing hot-dip galvanizing per ISO 1461 and ASTM A123 with a minimum bath temperature of 445°C–455°C, poles achieve an alloyed metallurgical bond that provides cathodic protection and self-healing zinc oxide barriers exceeding 25–50 years.
Multi-Payload Smart City Integration
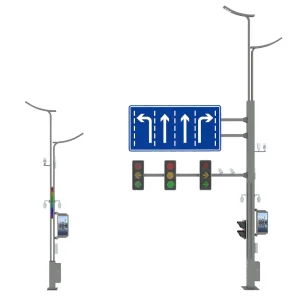
The contemporary GI pole is no longer merely a light carrier; it serves as a structural digital node. Engineering requirements now integrate structural vibration mitigation, continuous dynamic resonance analysis, internal thermal management channels for 5G microcell transceivers, IoT environmental sensing payloads, and unified municipal CCTV infrastructure without sacrificing aerodynamic performance.
Global Enterprise Procurement Criteria & Structural Specs
A technical cross-comparison of structural steel standards, coating methodologies, and aerodynamic validation protocols for international EPC contractors.
| Evaluation Parameter | EN 40-5 / ISO 1461 Specification | AASHTO / ASTM A123 Specification | Xintong Heavy-Duty Export Standard |
|---|---|---|---|
| Base Raw Material | S235JR, S355JR (EN 10025-2) | ASTM A36, ASTM A572 Grade 50 | Traceable Q235B / Q355B with Mill Certificates |
| Galvanizing Thickness | 70 µm – 85 µm (depending on wall gauge) | 86 µm – 100 µm (600 g/m² min) | 86 µm – 120 µm (Internal & External Full Immersion) |
| Welding Certification | ISO 3834-2 / EN 1090-2 (Execution Class 2) | AWS D1.1 Structural Steel Welding | Submerged Arc Longitudinal Welding (100% Penetration) |
| Wind Load Resistance | Calculated up to 36 m/s per Eurocode 1 | 160 km/h – 260 km/h (AASHTO LTS-6) | Custom Calibrated: 160–240 km/h (Typhoon/Hurricane Rated) |
| Coating Duplex Option | Polyester Powder Coat per Qualicoat Standard | Electrostatic Thermoset TGIC Powder Coat | Shot-blasted (Sa 2.5) + Hot-Dip Zinc + 100 µm Duplex TGIC |
Macro-Infrastructure Structural Deployments
Engineered pole configurations optimized for high wind shear, variable dead loads, and specialized utility distribution.
Deep-Water Seaports & Maritime Terminals
Characterized by aggressive airborne salinity and high wind vortices. Our high-mast towers utilize multi-piece slip-fit telescopic shafts (polygonal 12-sided to 20-sided) hot-dip galvanized up to 120 µm. Features fail-safe motorized head-frame hoisting assemblies, stainless steel wire ropes (AISI 316), and IP66 gearboxes for unhindered 24/7 port logistical operations.
Interstate Expressways & High-Speed Arterials
Expressway poles undergo repetitive cyclic wind loading, vehicle vortex shedding, and lateral buffeting. Our tapered octagonal and conical shafts are hydro-formed with continuous automatic seam welding. Anchor baseplates are reinforced with full-gusset structural stiffeners to eliminate fatigue cracking at the pole-to-base weld throat.
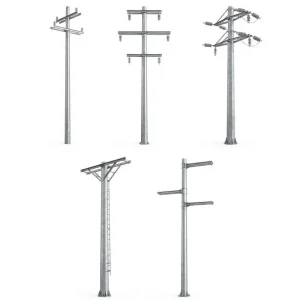
Low-Voltage Urban Power Distribution (Power Poles)
Replacing deteriorating timber and brittle concrete poles, galvanized iron distribution poles deliver predictable structural shear and moment capacity under uneven cable tension. Sized to withstand transverse line wind forces and dead-end tension spans with specialized cross-arm bracket attachments.
Localized Support & Tender Compliance Guarantee
A rigorous five-tier inspection protocol guaranteeing that delivered components align seamlessly with the consulting engineer's design criteria.
Tender Submission Packs
Complete documentation deliverables including finite element structural calculations, DIALux simulation files, anchor foundation design recommendations, and structural fabrication drawings.
Destructive & NDT Testing
Ultrasonic weld testing (UT), magnetic particle inspection (MPI), tensile yield verification, Charpy V-notch impact tests at sub-zero temperatures, and cross-hatch coating adhesion tests.
Global Export Logistics
Poles are bundled using protective bubble wrap, woven non-scratch webbing, and customized wooden dunnage to eliminate abrasion damage to zinc coatings during long maritime transit.
Field Engineer Dispatch
Comprehensive remote video guidance or on-site engineer deployment for critical high-mast hoisting, telescopic slip-joint hydraulic pressing, and anchor bolt torque validation.
Technological Roadmap: The Next Era of Structural Metallurgy
Anticipating structural engineering demands over the coming decade through advanced materials, smart manufacturing, and sustainable production.
Formulating zinc-aluminum-magnesium (Zn-Al-Mg) bath chemistries enhanced with colloidal graphene to increase salt spray resistance from 1,000 hours to over 4,500 hours without thickness increases.
Replacing traditional submerged arc systems with high-power multi-axis fiber laser tracking, minimizing Heat Affected Zones (HAZ) and virtually eliminating micro-porosity at longitudinal joints.
Embedding passive piezoelectric and strain-gauge sensors in high-mast bases to stream continuous structural resonance, wind-fatigue data, and anchor-bolt loosening warnings to smart city dashboards.
Integrating 100% electric arc furnace (EAF) low-carbon recycled steel certified through global Environmental Product Declarations (EPD) to support stringent LEED and BREEAM project compliance.
Frequently Answered Engineering & Sourcing Questions
Direct technical responses addressing common procurement, structural specification, and corrosion questions.
What is the true difference between Galvanised Iron (GI) and Hot-Dip Galvanized Steel?
In industry terminology, "Galvanised Iron" is a historical and widespread colloquial classification for carbon structural steel (such as Q235B or Q355B) that has undergone hot-dip galvanization per ISO 1461 / ASTM A123. Unlike pre-galvanized sheet (which is roll-formed after thin electro-galvanizing), our poles are submerged into molten zinc after all fabrication, cutting, punching, and welding are finished, sealing all edges and interior walls.
How are high mast poles connected on site without compromising structural integrity?
High mast structures ranging from 15m to 40m+ utilize precision-tapered slip joints (friction joints). The sections are assembled on the ground using hydraulic pullers applying pre-calculated pulling tonnage. This eliminates cross-sectional field welds that could damage the zinc protective layer, maintaining wind-load structural elasticity without structural degradation.
How does Xintong calculate wind load resistance for foreign municipal tenders?
We deploy finite-element modeling based on project site-specific 50-year or 100-year mean recurrence interval wind velocities. The structural engineering models account for basic wind velocity (Vb), terrain roughness categories, top-mounted effective projected area (EPA), luminaire weight, and vortex-induced dynamic vibrations to calculate minimum base diameter, top diameter, and wall thickness.
Can galvanized iron poles be powder coated, and how is adhesion maintained?
Yes, this is known as a Duplex Coating System. Hot-dip galvanized poles are degreased, chemically etched or sweep-blasted with non-metallic fine media to create an anchoring profile, and treated with a chromate or zirconium conversion layer before electrostatic deposition of pure polyester architectural powder. This prevents peeling or flaking in extreme UV and marine environments.
What is the standard production lead time and minimum order quantity (MOQ)?
Standard municipal series poles maintain an average turnaround time of 15 to 25 business days for quantities of 100 to 2,000 units. For customized heavy-duty high masts or specialized power transmission poles, lead time ranges between 20 to 30 business days depending on design approvals. We support project-based MOQs based on container load optimization.
Specialized Galvanized Columns & Mast Configurations
Explore our complete catalog of industrial, distribution, and smart city infrastructure solutions manufactured in our 100,000m² Jiangsu facility.