Featured Swaged & Municipal Steel Pole Series
Explore our flagship hot-dip galvanized swaged tubular steel poles and integrated smart infrastructure solutions built for high-wind loads and prolonged durability.
Executive Whitepaper: Swaged Steel Poles in Global Infrastructure
A comprehensive analysis of swaged tubular pole manufacturing, structural mechanics, anti-corrosion science, and international procurement standards.
Structural Mechanics & Advantage of Swaging
Swaged tubular steel poles are manufactured through a specialized rotary cold or hot forging process that reduces the diameter of seamless or high-frequency welded (ERW) steel pipes at discrete transition zones. Unlike continuously tapered polygonal poles, swaged poles maintain a stepped cylindrical geometric profile. This structural design offers uniform torsional resistance, predictable natural resonance frequencies, and optimized wind-load distribution along the vertical axis, making them preferred for urban distribution lines, street lighting, and telecommunication micro-cells.
Global Industrial Demand Dynamics
The global shift toward resilient smart grid networks, municipal electrification, and off-grid solar infrastructure has accelerated the procurement of swaged tubular poles. Industrial utility operators in Asia, the Middle East, Africa, and South America prioritize swaged poles due to their modular transportation footprint, rapid site assembly, and compatibility with standard mounting brackets. As urban centers transition to 5G smart poles, swaged steel structures provide ideal internal conduit routing for power cables and fiber optic lines without compromising structural stability.
Technical Advantage: Swaged Tubular Steel vs. Folded Tapered Poles
Swaged poles utilize high-tensile structural steel tubes (Q235B, Q355B, ASTM A500 Grade B) joined via internal hydraulic swaging with full circumferential fillet welding at joint transitions. This eliminates vertical seam stress concentrations found in press-braked polygonal poles, providing superior resistance to dynamic fatigue caused by vortex-induced vibration (VIV) and extreme gust loadings up to 260 km/h (72 m/s).
Swaged Pole Manufacturing Process & Quality Engineering
From raw chemical composition verification to metallurgical hot-dip galvanizing, examine the exact engineering standards governing high-integrity swaged steel poles.
1. Precision Rotary Swaging
Cold and hot hydraulic rotary swaging equipment forces structural steel pipes into overlapping stepped joints. The joint overlap length is engineered to be at least 1.5 to 2.0 times the outer pipe diameter, ensuring that mechanical load transfer across the joint exceeds the ultimate tensile strength of the base steel pipe.
2. Circumferential Welding
Joint swaging zones undergo automated Submerged Arc Welding (SAW) or Gas Metal Arc Welding (GMAW). Weld seams are subjected to Non-Destructive Testing (NDT), including Ultrasonic Testing (UT) and Magnetic Particle Inspection (MPI) per ISO 5817 Level B standards, verifying complete penetration without porosity or micro-fissures.
3. Hot-Dip Galvanizing (HDG)
Fabricated poles undergo acid pickling, fluxing, and full immersion in a molten zinc bath maintained at 445°C to 460°C per BS EN ISO 1461 / ASTM A123. The resulting metallurgically bonded zinc-iron alloy layers provide an outer zinc protection thickness exceeding 85 µm, offering a 30+ year maintenance-free lifespan in corrosive marine and industrial zones.
| Specification Parameter | Swaged Steel Tubular Poles | Octagonal Tapered Steel Poles | Prestressed Concrete Poles |
|---|---|---|---|
| Structural Profile | Stepped Multi-Diameter Tubular (ERW/Seamless) | Folded Single/Double-Seam Octagonal Taper | Solid / Hollow Cast Concrete with Steel Rebar |
| Wind Load Capacity | Up to 260 km/h (FEA Verified per AASHTO) | Up to 180 km/h (Subject to seam fatigue) | Moderate (Prone to brittle shear failure) |
| Corrosion Protection | Internal & External HDG + Duplex Powder Coat | Hot-Dip Galvanized / Painted Surface | Rebar spalling under coastal chloride attack |
| Transport & Assembly | Lightweight modular sections, low freight bulk | Nest-able tapered sections | Extremely heavy, requires crane equipment |
| Smart City Integration | Internal cable routing, 5G & IoT compatible | External conduit modification required | Limited internal raceway space |
XINTONG Group Engineering Capacity & Global Reach
A proven track record of structural engineering excellence across municipal, highway, and utility tenders worldwide.
Regional Compliance & Application Scenarios
Adapting swaged tubular steel poles to geographical wind pressures, seismic conditions, and regional electric utility standards.
Municipal Arterials & Highways
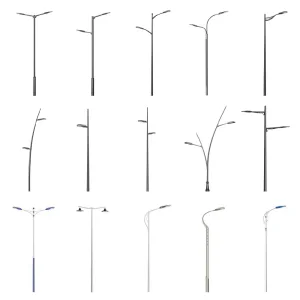
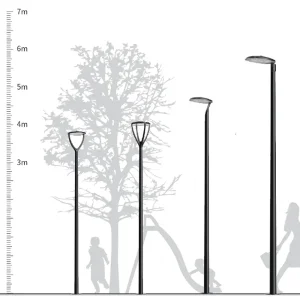
For high-speed expressways and urban boulevards, swaged poles support single or double luminaire arms ranging from 4m to 15m in height. Engineered according to EN 40-5 and AASHTO LTS-6 standards, they accommodate wind shear forces while housing internal fuse boxes, service doors, and earthing terminals safely above flood levels.
Low-Voltage Utility Distribution
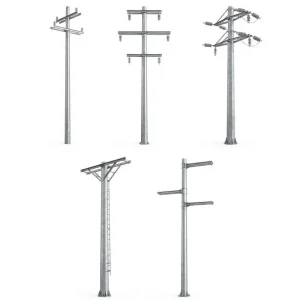
Utility electrification programs rely on swaged steel poles (such as SP-1 through SP-72 utility standards) to replace aging wooden and concrete distribution structures. Steel swaged poles handle overhead conductor tensions, cross-arm transformer loads, and service drops with minimal deflections.
Smart City & IoT Multi-Sensor Poles
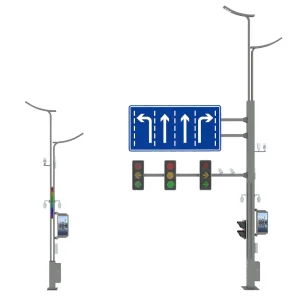
Modern swaged tubular poles serve as structural backbones for smart cities. Equipped with internal mounting rails, fiber-optic distribution boxes, environmental monitoring sensors, emergency call buttons, and 5G micro-cell antennas, they blend seamlessly into urban streetscapes without unsightly external wiring.
Technology Roadmap & Next-Generation Innovations
Anticipating future infrastructure demands through advanced metallurgy, sustainable manufacturing, and smart structural monitoring.
Zinc-Aluminum-Magnesium (ZAM) Coatings
To exceed traditional hot-dip galvanizing protection in harsh coastal and high-salinity industrial environments, next-generation swaged poles are adopting ZAM alloy coatings. ZAM provides self-healing cut-edge corrosion protection and up to 3 times the atmospheric corrosion resistance of conventional pure zinc coatings, reducing lifecycle maintenance costs for municipal authorities.
Embedded Structural Health Monitoring (SHM)
Integration of low-power MEMS accelerometers and strain gauges inside the swaged joint transitions allows real-time structural health monitoring. Municipal asset managers receive automated alert signals regarding mechanical fatigue, wind overload events, or vehicle collision damage, shifting infrastructure management from reactive repair to predictive maintenance.
Frequently Asked Questions (Technical & Procurement Guidance)
In-depth technical answers addressing engineer submittals, tender specifications, and quality verification standards.
How are swaged poles designated according to international standard dimensions?
Swaged poles are designated based on total overall height (e.g., 9m, 11m, 12m), the nominal outside diameters of each stepped tube section (e.g., bottom 139.7mm, middle 114.3mm, top 88.9mm), and the corresponding wall thickness (e.g., 4.5mm / 3.65mm / 3.25mm). Standard utility designs follow standard designations such as IS 2713 or equivalent BS/EN structural profiles.
What structural safety factor is calculated for wind shear and top equipment loading?
XINTONG swaged poles are engineered with a minimum safety factor of 1.5 to 2.0 relative to the yield strength of the steel ($f_y = 235 \text{ MPa}$ for Q235B or $f_y = 355 \text{ MPa}$ for Q355B). Structural finite element analysis (FEA) verifies that maximum bending moments under design wind pressure (e.g., 45 m/s gust) remain safely within elastic deformation limits.
What documentation is provided for international tender submittals?
Every shipment includes a comprehensive Quality Assurance Package: Mill Test Certificates (MTC) according to EN 10204 3.1, Hot-Dip Galvanizing Coating Thickness Inspection Reports (ISO 1461), NDT Weld Test Certificates, Non-Destructive Dimension Verification, and DIALux Photometric / Structural Design Calculations.
Can swaged poles be installed via direct burial or baseplate mounting?
Yes. Swaged poles are available in both direct-burial configurations (where the bottom section extends 1.5m to 2.0m below ground with an anti-rotation planting sleeve) and base-plate flange configurations (welded structural baseplate anchored to concrete foundation bolts via anchor cage assemblies).
Complete Swaged & High-Mast Product Catalog
Select specialized pole configurations for high mast transit, stadium lighting, urban power distribution, and decorative municipal applications.
Partner with a Certified Swaged Pole Manufacturer
Direct factory sourcing from Yangzhou Xintong Traffic Equipment Group Co., Ltd. Over 25 years of manufacturing excellence, 100,000 m² plant capacity, and certified ISO/EN/ASTM technical compliance for global EPC project tenders.