High Mast & Infrastructure Engineering Product Showcase
Pre-engineered structural designs with turnkey photometric validation, hot-dip galvanization, and ISO/CE certified manufacturing protocols.
High Mast Lighting in Global Infrastructure Procurement
Modern mega-scale infrastructure projects require certified structural integrity, standardized metallurgical fabrication, and turnkey optical engineering.
Engineered strictly under AASHTO LTS-6 and EN 40-3 structural safety factors.
Certified yield strengths providing optimal elastic deformation margins under gust shocks.
ISO 1461 and ASTM A123 compliance guaranteeing 30+ years of anti-corrosion life.
Modular polygonal sections (12-sided, 16-sided, 20-sided) with precision slip joints.
Maritime Terminals & Heavy Ports
Seaport container berths, freight sorting yards, and dry docks demand massive surface coverage with zero blind spots. Salt-fog atmospheric corrosion (ISO 12944 C5-M marine rating) necessitates dense hot-dip zinc layers combined with dual-layer marine polyurethane topcoats.
- Vibration-dampened floodlight mounting rings
- Dual-winch stainless steel hoist mechanisms
- Resistance to corrosive chloride maritime environments
International Airports & Aprons
Apron floodlighting towers require strict optical beam cut-offs to eliminate pilot glare and prevent interference with Air Traffic Control (ATC) towers, compliant with ICAO Annex 14 Vol. 1 and FAA Advisory Circular AC 150/5345-43 standards.
- Medium/High Intensity ICAO Type A/B obstacle beacons
- Electromagnetic compatibility (EMC) shielded drivers
- Asymmetric downward optical targeting (0% upward lux)
Expressway Interchanges & Rail Depots
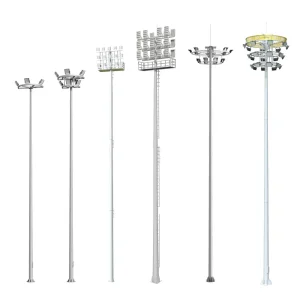
Complex multi-tier highway flyovers and marshaling yards utilize high masts (20m to 35m) to replace dozens of small street poles. This reduces roadside collision hazards, unifies surface illuminance, and lowers civil maintenance downtime.
- Motorized internal winch eliminating maintenance bucket trucks
- Automated mechanical docking and latching barrels
- High illuminance uniformity ratio (U0 > 0.40)
Engineering Architecture of Industrial High Mast Systems
A comprehensive breakdown of structural geometry, winch mechanics, and metallurgical standards essential for engineering submittals and BOQ compliance.
| System Component | Structural Engineering Specification | International Standard Alignment | Procurement & Tender Relevance |
|---|---|---|---|
| Pole Shaft Geometry | 12, 16, or 20-sided polygonal tapered sections; telescoping overlap joints (slip joint ratio 1.5 × diameter). Single longitudinal submerged arc weld. | EN 40-3, BS 5649, ASTM A595 Gr. A/B | Eliminates circumferential weld fatigue; ensures laminar aerodynamic wind flow reducing vortex shedding. |
| Base Flange & Anchoring | Thermally cut structural steel plate (thickness 25mm–45mm), radial gusset plate reinforcements; Grade 8.8 hot-dip galvanized anchor J-bolts. | AASHTO Standard Specifications for Structural Supports, ISO 898-1 | Transfers overturning bending moments directly into civil reinforced concrete pile caps. |
| Lifting Mechanism | Integrated bi-directional self-locking worm gear winch, dual stainless steel wire ropes (AISI 316, 7×19 construction), safety factor ≥ 5:1. | EN 12100 Safety of Machinery, OSHA 1926.552, TR. No. 7 ILP | Enables safe ground-level maintenance without bucket trucks; internal fail-safe torque limiter prevents cable slippage. |
| Latching & Docking Head | Mechanical latching barrel with stainless steel locking pins; dual flag visual confirmation indicators; heavy-duty cast aluminum pulley cluster. | Institution of Lighting Professionals (ILP) TR. No. 7 | Relieves continuous tensile stress from hoisting cables once the luminaire ring is locked in its elevated operating state. |
| Optical Fixtures | High-pressure die-cast aluminum (ADC12), IP66/IP67 ingress protection, IK09/IK10 impact resistance, luminous efficacy ≥ 150–170 lm/W. | IEC 60598-2-5, IESNA LM-79, LM-80, TM-21 | Delivers exact asymmetric photometric profiles via precise DIALux simulation; suppresses upward skyglow (ULOR < 1%). |
| Corrosion Protection | Internal and external hot-dip galvanizing bath (≥ 450°C) producing Fe-Zn alloy metallurgical bonding. Optional electrostatic polyester powder coat. | ISO 1461, ASTM A123, EN ISO 12944 (C4 to C5-M) | Guarantees 25 to 50 years operational lifespan in coastal salt spray, industrial sulfur dioxide, and tropical humidity. |
EPC Engineering Submittal Checklist
Before issuing requests for quotation (RFQs) or confirming letters of credit (LCs) for high mast pole lights, project engineers and procurement officers must verify that the manufacturing partner provides the following technical dossier:
Macro-Scale Municipal & Industrial Solutions
Engineered structural assemblies configured to meet distinct mechanical, environmental, and electrical requirements across critical global sectors.
Civil Intermodal Freight & Rail Terminals
Rail freight hubs require consistent ground-level lux to safely guide intermodal container reach stackers, gantry cranes, and train operators. High masts positioned at 40m intervals provide continuous 50-lux illumination across tracks without creating shadows behind container stacks.
- High-mast heights: 25m to 40m with heavy floodlight payloads
- Multi-directional aiming head-frames (circular, symmetric, or asymmetric)
- Heavy-duty junction boxes rated IP67 with centralized surge suppression (20kV)
Mega-Sports Stadiums & Arenas
Broadcast-grade sports floodlighting must adhere to FIFA, FIBA, and Olympic television transmission criteria, requiring Flicker Factor < 1% for ultra-slow-motion cameras, Television Lighting Consistency Index (TLCI) > 85, and Color Rendering Index (CRI) ≥ 90.
- Custom structural head-frames with multi-tier floodlight ladders
- Integrated maintenance cages and climbable safety ladders with fall arrester rails
- DMX512 and DALI-2 dynamic digital dimming networks for arena entertainment
Refineries, Mining & Hazardous Facilities
Petrochemical tank farms, open-cast mining sites, and processing plants necessitate rugged lighting towers that withstand extreme dust, explosive gas atmospheres, and aggressive chemical fumes. Our high mast assemblies are customized with explosion-proof options and severe vibration dampeners.
- Optional ATEX and IECEx compliant luminaire installations
- Heavy wall steel tubing engineered for seismic ground vibrations
- Double-drum cable winches preventing accidental carriage drop during shock waves
Technology Roadmap & Future Outlook (2025–2035)
The high mast industry is undergoing a paradigm shift from passive structural steel posts to smart, sensor-integrated, and energy-resilient infrastructure assets.
GaN Optical Drivers & 200+ lm/W Micro-LEDs
Next-generation high mast floodlights utilize Gallium Nitride (GaN) power semiconductors to slash driver thermal output by 40% while increasing electrical conversion efficiency to > 96%. Combined with multi-junction Micro-LED emitters, operational system efficacy exceeds 200 lumens per watt, cutting municipal operating power costs in half.
Digital Twin & Structural Vibration Telemetry
IoT-enabled accelerometers and laser deflection monitors mounted inside the mast cap monitor real-time harmonic resonance and vortex-induced vibrations (VIV). Data streams through LoRaWAN or 5G private cellular networks directly to municipal Digital Twin platforms, scheduling predictive maintenance prior to structural metal fatigue.
Robotic Crawlers & Automated Cable Inspection
Eliminating high-risk human maintenance, emerging high mast setups utilize magnetic crawler robots equipped with high-resolution eddy current testing (ECT) probes. These robots traverse the exterior galvanized shaft to inspect weld integrity, measure zinc coating degradation, and verify cable health autonomously.
Global Compliance & Localized Engineering Support
How certified manufacturers streamline regulatory approvals for international general contractors and public tenders across North America, Europe, the Middle East, and Latin America.
AASHTO & EN Structural Standards
Our engineering division executes finite structural calculations aligned with the American Association of State Highway and Transportation Officials (AASHTO) Standard Specifications for Structural Supports for Highway Signs, Luminaires, and Traffic Signals, as well as European standard EN 40-3-1 / EN 40-3-3.
Detailed verification calculations assess pole drag coefficients ($C_d$), gust effect factors, maximum tip deflection limits, and fatigue life under cyclical wind loading.
ISO 1461 Hot-Dip Galvanization Guarantees
All structural components undergo comprehensive surface preparation, including chemical degreasing, acid pickling, and fluxing before immersion in molten zinc maintained at 445°C–455°C. The resulting iron-zinc metallurgical layers provide self-healing cathodic protection.
Standard coating thickness exceeds 86 μm (610 g/m²), with options for specialized coastal marine packages exceeding 120 μm thickness for severe offshore exposure.
Third-Party FAT & Non-Destructive Testing
Factory Acceptance Testing (FAT) is facilitated on-site or via live encrypted high-definition video streaming for international engineering auditors. Certified Level II inspectors perform:
- Ultrasonic Flaw Detection (AWS D1.1 / ISO 17640) on full-penetration flange welds
- Magnetic Particle Inspection (MPI) along the longitudinal submerged arc seams
- Magnetic coating thickness gauge checks across all pole sections
High Mast Procurement & Engineering FAQ
Authoritative answers to the most critical technical, commercial, and logistical questions posed by consulting engineers, EPC firms, and municipal procurement directors.
High mast lighting poles are typically engineered for 3-second gust wind speeds ranging from 120 km/h up to 200 km/h (33 m/s to 55 m/s), calculated based on local meteorological codes (e.g., ASCE 7-16 in the Americas, Eurocode 1 EN 1991-1-4 in Europe, or CP3 in the Middle East). The Effective Projected Area (EPA) and aggregate weight of the luminaire carriage are factored into finite element analysis to ensure the maximum deflection does not exceed 10% of total pole height under extreme gusts.
The system consists of an internal double-drum worm gear winch driven by a portable electric motor tool or manual backup crank. It features an automated mechanical latching mechanism located inside the mast cap. Once raised, mechanical dogs engage with latch pins, transferring the entire luminaire weight onto the rigid mast structure. This releases all continuous tension from the stainless steel wire ropes, preventing cable fatigue and safeguarding personnel working below.
Tender-grade high masts are fabricated from high-strength low-alloy structural steel, predominantly Q355B (equivalent to EN 10025 S355JR, ASTM A572 Grade 50) or Q460 for extreme-height poles (40m–50m). These steels offer a minimum yield strength of 355 to 460 MPa, providing excellent weldability, ductile fracture toughness in cold climates (Charpy V-notch impact testing tested at 0°C or -20°C), and optimal silicon content (0.15% to 0.25%) for uniform hot-dip galvanization.
Slip joint assembly relies on telescoping tapered polygonal sections that overlap under hydraulic pressure (overlap length ≥ 1.5 times the mating inner diameter). It is the globally preferred method for 15m to 40m masts because it avoids circumferential welds that are prone to wind fatigue and dramatically reduces shipping container volume. Flange-bolted joints are typically reserved for specialized heavy industrial towers or locations where site space prohibits horizontal hydraulic pulling.
The foundation design must be prepared by a registered civil geotechnical engineer using site-specific soil borehole data. Our manufacturing package provides the exact foundation reaction loads: overturning moment ($M$), vertical dead weight ($N$), and base shear ($V$). We supply complete anchor bolt cage assemblies with heavy-duty template rings, high-tensile Grade 8.8 galvanized J-bolts, leveling double-nuts, and lock washers to ensure precise civil alignment.
Glare mitigation is achieved through precision DIALux EVO optical simulations using asymmetric flat-glass floodlights. By utilizing forward-throw lens optics and internal baffles, light is directed downward with an Upward Light Output Ratio (ULOR) of 0%. For airports, luminaires must strictly comply with ICAO Annex 14 criteria limiting the maximum luminous intensity directed into approaching cockpit flight angles and air traffic control cabs.
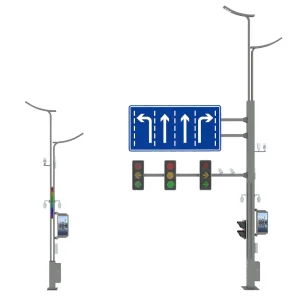
Yes. Modern multifunctional high masts are engineered with multi-compartment internal cabling channels, isolated low-voltage data conduits, and external mounting brackets for 360-degree PTZ surveillance cameras, weather stations (anemometers), cellular micro-base stations, and public address horns. Our engineers perform structural recalculations to account for the additional weight and wind drag of all auxiliary devices.
Poles are nested using high-density polyethylene spacers and protective geotextile bubble wrapping to eliminate metal-to-metal abrasion during maritime transit. Smaller telescoping sections are nested inside larger base sections when dimensions allow, maximizing 40ft High Cube (40HC) or flat-rack container utilization. All winch gearboxes, stainless steel ropes, and precision electrical fixtures are crated in seaworthy fumigated timber boxes.
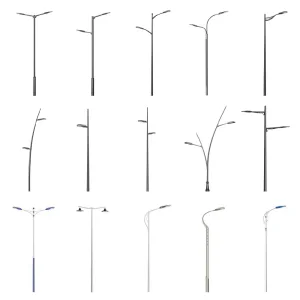
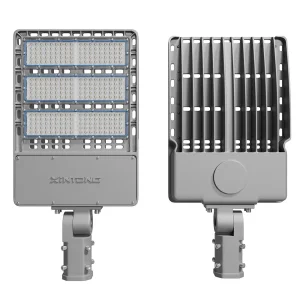
Explore Our Comprehensive High Mast & Municipal Series
From extreme-duty coastal towers to integrated smart city steel columns, review our complete line of export-grade municipal and utility structures.
How General Contractors Procure High Mast Infrastructure
A step-by-step technical due diligence workflow ensuring zero-defect manufacturing, seamless customs clearance, and error-free on-site erection.
Phase 1: Photometric & Civil Discovery
Contractors submit their CAD site layout, environmental wind conditions, and target lux parameters. Our engineering department executes a comprehensive DIALux EVO study that confirms luminaire count, tilt angles, optical beam spreads, and mounting heights to achieve target illumination without light pollution.
Phase 2: Structural Verification Dossier
Prior to steel cutting, an in-depth structural report is compiled for the client's Engineer-of-Record (EoR). The package includes exact section dimensions, base plate anchor sizing, slip joint overlap lengths, and finite calculation models confirming safety margins under peak wind pressure.
Phase 3: Automated Fabrication & QA
Computer-controlled CNC plasma cutters, massive hydraulic bending presses (up to 2,000 tons), and submerged arc welding gantries form the high mast sections. Products pass through chemical hot-dip galvanizing, followed by multi-point ultrasonic weld checks and mechanical dry-fit testing.
Phase 4: Global Incoterms Logistics
Whether operating on FOB, CIF, or DDP terms, our dedicated logistics specialists coordinate container loading to prevent nesting damage, manage phytosanitary timber certification, prepare consular invoices, and provide accurate bill-of-lading (B/L) tracking for port arrivals.