Engineered Grid Solutions Ready for Deployment
Direct from our 100,000 m² Gaoyou facility. Explore our primary low-voltage distribution, municipal infrastructure, and smart lighting lines engineered to withstand extreme environmental stress.
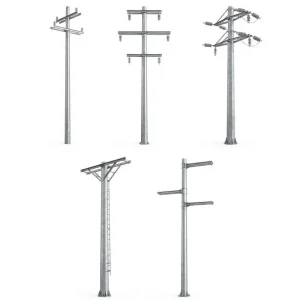
The Paradigm Shift in Low Voltage Distribution Infrastructure
Low voltage (LV) power distribution networks—operating typically below 1 kV AC (230V single-phase / 400V three-phase)—represent the critical "last-mile" bridge connecting primary substations to end-use commercial, industrial, and residential meters. As national power grids worldwide face unprecedented decentralized generation, extreme climatic events, and the surge of electric mobility, traditional structural assets are proving insufficient.
Grid Decarbonization & DRE Integration
Decentralized Renewable Energy (DRE), including commercial rooftop photovoltaics and micro-wind installations, requires LV distribution poles capable of supporting bi-directional power flows, pole-mounted step-up transformers, and smart switchgear assemblies without compromising safety factors.
Material Transition from Wood to Steel
Historically dominated by treated timber and prestressed spun concrete, modern utility engineering mandates a total shift toward hot-dip galvanized hollow steel poles. Steel offers a strength-to-weight ratio over 400% higher than concrete, eliminating micro-cracking and core moisture intrusion.
Severe Climate Resilience
Modern LV distribution networks are engineered to ASCE Manual 72 and EN 40 standards. Tapered octagonal and conical tubular steel geometries dramatically reduce the aerodynamic drag coefficient (Cd), resisting cyclonic wind speeds exceeding 200 km/h and heavy radial ice accumulation.
Key Technical Insight: Aerial Bundled Cable (ABC) Torsional Loading Mechanics
Unlike high-voltage transmission lines that rely on open-air bare conductors on extensive right-of-ways, urban and suburban low-voltage distribution relies heavily on Aerial Bundled Cables (ABC). While ABC enhances dielectric safety and prevents power theft, it significantly increases mechanical windage and deadweight. Our Q355B high-tensile structural steel distribution poles are calculated via finite element analysis (FEA) to provide elevated polar moments of inertia, resisting severe torsional twisting and deflection at terminal dead-ends and angle-strain structures.
International Demand Trends Across Energy & Infrastructure Sectors
From state-owned national utility tenders to turnkey international engineering, procurement, and construction (EPC) conglomerates, procurement criteria for low-voltage power poles have evolved beyond initial unit cost toward holistic Total Cost of Ownership (TCO) and rapid logistics scalability.
North America & Europe
Grid Modernization & Wildfire Hardening: Massive replacement programs targeting aging timber poles in wildland-urban interfaces (WUI). Utilities prioritize non-combustible Class 1 fire-rated tubular steel poles with anti-climb coatings and pre-drilled hardware mounts.
Middle East & North Africa
C5-M Marine & Thermal Resistance: Rapid industrialization and desalinization microgrids require poles certified for extreme ultraviolet radiation, abrasive sandstorms, and hypersaline atmospheres via multi-layer HDG plus polyurea topcoats.
Asia-Pacific (APAC)
Typhoon Corridors & Urban Growth: Heavy demand for tapered octagonal steel distribution poles rated for Category 5 tropical cyclones, capable of dual-purpose function as overhead cable supports and municipal LED illumination columns.
Latin America & Africa
Last-Mile Electrification: Focus on modular slip-joint steel distribution poles that optimize shipping container payload cubic space, slashing intermodal freight costs and enabling manual winch erection in roadless rural regions.
| Evaluation Parameter | Xintong Hot-Dip Galvanized Steel | Prestressed Spun Concrete | Creosote-Treated Timber | Fiberglass / FRP Composite |
|---|---|---|---|---|
| Structural Service Life | 50+ Years (C4 Environment) | 25–35 Years (Susceptible to spalling) | 15–25 Years (Subject to rot/termites) | 30–40 Years (UV degradation risks) |
| Weight / Transport Footprint | Ultra-Low (Hollow, slip-joint) | Extremely Heavy (High crane cost) | Moderate (Solid core, bulky) | Extremely Light (Premium cost) |
| Bending & Torsional Strength | Yield Strength ≥ 355 MPa | High compression, poor ductility | Unpredictable natural grain variance | High flexible deflection |
| Fire & Combustion Rating | Class A Non-Combustible | Non-combustible (Explosive spalling) | Highly Combustible (Accelerant) | Self-extinguishing (Resin smoke) |
| Total Lifecycle TCO | Lowest (Zero field maintenance) | High (Installation & replacement labor) | High (Frequent replacement cycles) | Very High (Elevated CAPEX) |
| Recyclability & Circularity | 100% Recyclable Scrap Value | 0% (Landfill waste / crushing cost) | 0% (Hazardous chemical disposal) | <10% (Difficult polymer separation) |
China Factory 4.0: Supply Chain Resilience & Precision Scale
Operating from our centralized 100,000 square meter industrial manufacturing complex in Gaoyou, Jiangsu—China’s global hub for traffic and lighting pole fabrication—Yangzhou Xintong Traffic Equipment Group represents the pinnacle of automated steel pole processing and end-to-end quality assurance.
Traceable Low-Silicon Structural Steel
We source primary flat-rolled sheet coils exclusively from tier-1 mills (BaoSteel, Shougang) with complete EN 10204 3.1 Material Test Reports (MTR). Silicon content is controlled within the strict Sandelin curve bracket (<0.03% or 0.15%–0.25%) to prevent excessive Fe-Zn crystal growth during hot-dip galvanizing, ensuring smooth, non-brittle protective coatings.
16-Meter CNC Tandem Press Braking
Equipped with computerized 1,200-ton 16-meter hydraulic tandem press brakes, our forming shop forms continuous conical and polygonal sections up to 16 meters in a single operation. This completely eliminates transversal circumferential welds on poles up to 14 meters, significantly mitigating fatigue notch concentration points.
Automated Dual-Arc Submerged Arc Welding
Our longitudinal seams are closed using high-speed dual-wire Submerged Arc Welding (SAW) stations guided by laser seam tracking. Full joint penetration exceeds 85% on structural bodies and 100% on base flange connections, validated through in-house ultrasonic (UT) and magnetic particle (MT) non-destructive testing.
Field-Proven Deployment Scenarios for Low Voltage Distribution
Low voltage poles operate in diverse microclimates and urban typologies. Xintong tailors steel wall thickness, taper rates, baseplate gussets, and cross-arm geometries to specific environmental loadings.
Urban Microgrids & Smart Streets
Low voltage feeders co-located with smart lighting luminaires, telecommunication 5G microcells, and municipal video surveillance. Poles integrate internal flush cable access doors, tamper-proof locks, and copper earthing studs for subterranean conduits.
Coastal Maritime & Port Terminals
High-saline C5-M atmospheric zones requiring hot-dip galvanizing exceeding 100 µm zinc thickness, combined with marine-grade polyester powder barrier coatings to combat saltwater spray, high humidity, and continuous winds (e.g., Cebu Port Terminal project).
Distributed Solar PV Feeder Lines
Connecting utility-scale or agrivoltaic distributed solar fields to centralized distribution transformer pads. Engineered for intermediate run support, acute angle turns, and conductor dead-ending without guy-wires, preserving agricultural equipment clearance.
High-Wind & Mountain Corridors
Sectional slip-joint poles designed to ASCE 72 wind velocity maps up to 60 m/s. Lightweight steel modules can be delivered via light utility trucks and winched manually into rock-drilled direct burial sockets or flanged anchor-cage footings.
Standard Technical Data Matrix: Low Voltage Steel Poles
The following parameters outline our baseline serialized LV power distribution pole range. All poles are fully customizable regarding height, nominal wall thickness, conductor bracket configurations, and foundation interfaces.
| Pole Height (Nominal) | Top Diameter (mm) | Bottom Diameter (mm) | Wall Thickness (mm) | Design Ultimate Moment | Conductor Capacity | Foundation Type |
|---|---|---|---|---|---|---|
| 7.0 Meters (23 ft) | 140 mm | 210 mm | 3.5 mm – 4.0 mm | 18.5 kNm | Up to 4x 70 mm² ABC + Streetlight | Direct Burial or Flanged Base |
| 8.5 Meters (28 ft) | 150 mm | 240 mm | 4.0 mm – 4.5 mm | 26.0 kNm | Up to 4x 120 mm² ABC + Service Drops | Flanged Base (4x M24 Anchor Bolts) |
| 10.0 Meters (33 ft) | 160 mm | 270 mm | 4.5 mm – 5.0 mm | 38.2 kNm | Multi-circuit LV + 25kVA Transformer | Flanged Base (8x M27 Anchor Bolts) |
| 11.5 Meters (38 ft) | 180 mm | 310 mm | 5.0 mm – 6.0 mm | 54.0 kNm | Heavy Strain / Angle Tension Support | Flanged Base (8x M30 Anchor Bolts) |
| 13.0 Meters (43 ft) | 200 mm | 350 mm | 6.0 mm – 8.0 mm | 78.5 kNm | Terminal Dead-End / Dual Circuit LV | Reinforced Concrete Pier Foundation |
Corrosion Shield Standards
Conforms to ISO 1461 and ASTM A123. Hot-dip galvanization is conducted after all punching, cutting, and welding are complete. Average coating thickness ranges from 86 µm to 120 µm, providing over 50 years of cathodic protection in aggressive outdoor soil and ambient air environments.
Quality Control & NDT Protocol
Each production batch undergoes 100% dimensional inspection, coating thickness magnetic gauge testing, weld cross-section macro-etching, and ultrasonic flaw detection. Standard FAT (Factory Acceptance Test) reports accompany every shipping container bill of lading.
Tender Submittal Engineering Packages
Our in-house technical department provides complete tender submittals within 48 hours: 2D fabrication shop drawings (AutoCAD), structural loading and deflection calculations (PLS-POLE / STAAD.Pro), baseplate anchor reaction forces, and DIALux lighting simulations for combined-use poles.
Specialized Infrastructure & Distribution Equipment
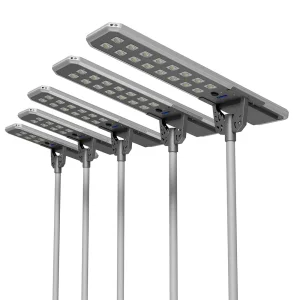
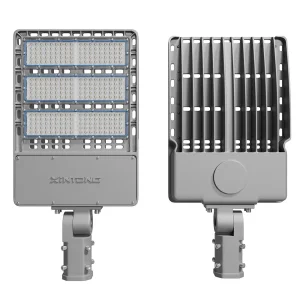
Explore our full line of specialized power distribution poles, all-in-one solar luminaires, and municipal lighting columns serving major global EPC contractors and energy utilities worldwide.
Frequently Asked Questions: Engineering & Procurement
Clear, technically rigorous answers to the critical engineering, quality compliance, and international logistics questions raised by utility procurement officers and consulting engineers.
Q355B (GB/T 1591) and ASTM A572 Grade 50 are chemically and mechanically equivalent high-strength low-alloy (HSLA) structural steels. Both possess a specified minimum yield strength of 355 MPa (approx. 50,000 psi) and minimum tensile strength ranging from 470 to 630 MPa. Q355B mandates guaranteed Charpy V-notch impact toughness tested at 0°C (minimum 34 Joules), making it ideal for temperate to sub-zero distribution networks. We supply full dual-certified mill test certificates (MTR) verifying compliance with both standards.
Coating integrity depends heavily on steel substrate metallurgy and immersion bath control. We maintain low-silicon and low-phosphorous steel inputs (Sandelin control: Si < 0.03%), which eliminates overly rapid, brittle iron-zinc alloy phase growth. Furthermore, our hot-dip galvanizing plant operates a 99.995% pure molten zinc kettle at a monitored 445°C–455°C. For extreme marine zones (ISO 12944 C5-M), we apply an electrostatic thermoset epoxy barrier primer followed by an architectural aliphatic polyurethane topcoat (Duplex System), exceeding 3,000 hours in salt spray testing.
The choice depends on geotechnical soil stability, right-of-way spatial restrictions, and local civil labor costs. Direct Burial (Embedded) requires an additional 10% to 15% pole length (typically 1.2m to 2.0m ground embedment), backfilled with crushed aggregate or concrete slurry. It eliminates anchor bolt casting, lowering civil CAPEX in open rural or cross-country terrains. Base Flange Mounting utilizes a precision steel base plate (16mm–30mm thickness) secured to a reinforced concrete pier via high-tensile J-bolts or threaded cages. This is preferred in congested urban streetscapes where excavation depth is constrained by underground municipal utilities.
Our engineering team performs non-linear second-order (P-Delta) structural modeling in accordance with ASCE Manual 72 and EN 40. We calculate the transverse wind load acting simultaneously on the projected area of the tapered pole shaft and the aerial bundled cables (ABC), combined with radial ice thickness (typically 10mm to 25mm glaze ice per IEC 60826). Longitudinal unbalanced tension loads—such as an accidental line drop or terminal dead-end pull—are modeled to ensure pole top deflection does not exceed 2.5% of total above-ground height at maximum working tension.
Yes. We regularly host certified third-party testing agencies—including SGS, Bureau Veritas (BV), TÜV Rheinland, and Intertek—designated by clients or public utility boards. Inspection scopes typically encompass Raw Material Traceability verification, Welding Procedure Specification (WPS) review, Welder Performance Qualification (WPQ), non-destructive testing (NDT/UT) of longitudinal and flange welds, zinc coating thickness measurement via calibrated magnetic gauges, and full-scale cantilever deflection destruction testing on prototype samples.
To avoid "white rust" (wet storage stain) and metal-to-metal rubbing during containerized maritime transit, each pole is individually wrapped with protective non-hygroscopic bubble film or heavy-duty burlap/geotextile strapping at contact points. Custom hardwood saddles and high-tensile steel strapping secure bundles inside 40ft High Cube (HC) or Open Top (OT) containers. Tapered poles can also be nested telescopically (pole-inside-pole) when modular slip-joint designs are specified, increasing freight container volume efficiency by up to 35%.
Submit Your Bill of Quantities (BOQ) or Tender Specifications
Our export engineering team provides structural reviews, CAD fabrication drawings, Foundation Reaction calculations, and firm factory-direct pricing within 24 hours. Connect with our Gaoyou manufacturing headquarters directly.