High-Performance Outdoor Lighting & Structural Mast Series
Engineered for extreme structural integrity, high wind loads, and zero-corrosion lifetimes in challenging municipal, transit, and heavy industrial environments.
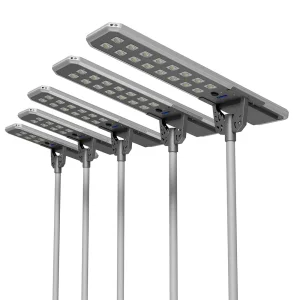
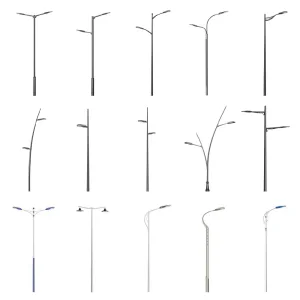
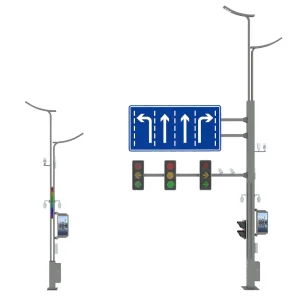
Global Commercial Dynamics: Outdoor Lighting Poles Market Evolution
A technical examination of global outdoor structural lighting requirements, urban renewal mandates, and rigorous municipal engineering compliance across international markets.
Civil Infrastructure & Public Works Tenders
Global civil tenders increasingly mandate life-cycle durability over initial acquisition costs. In North America and Europe, highway electrification contracts demand minimum 25-to-50-year maintenance-free life, verified by EN ISO 1461 hot-dip galvanizing benchmarks and AASHTO LTS-6 fatigue criteria. Municipalities are shifting procurement scoring models away from single component purchases toward fully certified structural assemblies with documented yield test records.
Supply Chain Realignment & Cost Pressures
Infrastructure contractors face extreme volatility in raw hot-rolled coil (HRC) steel pricing and oceanic freight tariffs. As EPC contractors operate under tight completion windows backed by liquidated damages, the necessity for integrated tier-one manufacturers who own in-house submerged-arc welding, automated slitting, and internal galvanizing baths has become critical for cost certainty and project timeline preservation.
Decarbonization & Solar-Hybrid Transition
Developing nations across Africa, Southeast Asia, and Latin America are heavily leapfrogging traditional grid extension through off-grid and hybrid solar-powered lighting networks. In contrast, mature economies are integrating EV micro-charging bases and micro-inverter hubs into existing low-voltage urban power distribution columns, merging public utility lines with autonomous aesthetic lighting fixtures.
Localized Engineering Application Scenarios
Outdoor lighting poles operate in vastly diverse environmental and mechanical conditions. Our structural engineering profiles are customized to match microclimates, seismic profiles, and local municipal mandates.
Deep-Water Seaports & Container Terminals
Challenge: Marine atmospheric corrosivity class C5-M, intense saline fog, and typhoon-force coastal wind gusts exceeding 200 km/h.
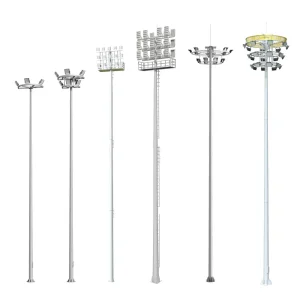
Engineering Solution: 25m to 40m polygonal high mast towers fabricated from Q355B structural steel with heavy base-flange stiffener gussets. Minimum 100μm hot-dip galvanization followed by dual-layer electrostatic polyurethane fluorocarbon coating. Motorized raising and lowering crown systems enable rapid ground-level maintenance without requiring aerial basket trucks in active gantry crane corridors.
Interstate Expressways & High-Speed Corridors
Challenge: High cyclic aerodynamic turbulence from heavy semi-truck traffic, demanding AASHTO fatigue-resistant engineering.
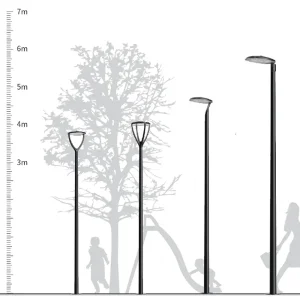
Engineering Solution: Seamless conical and multi-fluted octagonal poles with continuous one-pass longitudinal submerged arc welding. Optimized wall thicknesses (4mm to 8mm) calculated to prevent vortex shedding harmonic oscillations. Supplied with J-bolt foundation anchor cages fabricated to exact ASTM F1554 specifications for maximum sub-grade tensile resistance.
Smart City Arterials & Dense Civic Corridors
Challenge: Municipal visual clutter, rising sensor count, and high power-data segregation requirements within compact urban footprints.
Engineering Solution: Multifunctional integrated smart poles engineered with internal multi-compartment wiring channels, internal DIN-rail equipment bays, and external modular track brackets for 5G micro-cells, PTZ surveillance domes, environmental IoT sensors, and public Wi-Fi access points, fully powder-coated in customer RAL architectural tones.
Sub-Zero Mountain Passes & Steppe Regions
Challenge: Low-temperature brittle fractures, frost heave ground displacement, and sustained freezing blizzards in Central Asian and Nordic latitudes.
Engineering Solution: Steel grades formulated with Charpy V-notch impact toughness certified to -40°C (-40°F). Deep embedment direct-burial root sections or oversized thermal ground sleeves designed to resist frost heave forces, preserving vertical alignment across annual freeze-thaw cycles without anchor sheared-bolt degradation.
Arid Middle East Deserts & Mining Complexes
Challenge: Extreme UV radiation, daytime heat exceeding 50°C, abrasive sandstorm grit, and massive day-night thermal cycling expansion.
Engineering Solution: Heavy-gauge galvanized poles combined with abrasive-resistant silicone polyester powder coats. IP66 sealed electrical hand-holes with synthetic neoprene gasketing to prevent particulate ingress. Solar setups integrate high-temperature LiFePO4 battery enclosures with subterranean heat sinks.
International Airports & Military Perimeters
Challenge: Stringent FAA/ICAO obstacle height limits, radar non-interference requirements, and uncompromised perimeter illumination.
Engineering Solution: Frangible and hinged fold-over mast designs engineered to safely deform upon controlled physical impact. Integrated certified top-mount aviation obstruction beacons, pre-wired grounding conductors, and specialized shield brackets to eliminate upward glare in flight path clearance zones.
Outdoor Structural Lighting: Technology Roadmap to 2030
How next-generation metallurgical engineering, automated robotic welding, and intelligent edge-computing integration are reshaping physical pole infrastructures into cyber-physical assets.
High-Strength Micro-Alloys
Transitioning to ultra-high-yield automotive-grade cold-rolled steel (650–700 MPa yield strength), decreasing dead-weight by 22% while boosting maximum allowable wind resistance and significantly cutting ocean container shipping footprint.
Zinc-Aluminum-Magnesium Baths
Upgrading standard zinc baths to cutting-edge Zn-Al-Mg formulations providing auto-repairing edge passivation that outperforms traditional galvanized coatings by 300% in salt-spray ASTM B117 laboratory chamber stress tests.
Edge Computing Smart Cores
Standardizing universal plug-and-play Zhaga Book 18 and NEMA 7-pin socket architecture across all structural pole heads, facilitating field conversion to LoRaWAN, NB-IoT, and centralized 5G smart mesh city controllers without re-cabling.
Zero-Carbon Recycled Steel
Integrating certified Electric Arc Furnace (EAF) scrap-recycled green steel along with circular modular component joints to guarantee 98% end-of-life recycling efficiency and provide tender-ready Environmental Product Declarations (EPDs).
| Pole System Category | Typical Base Alloy | Yield Strength (ReH) | Corrosion Protection Standard | Wind Load Tolerance | Expected Design Life |
|---|---|---|---|---|---|
| Standard Conical Municipal Pole | Q235B / ASTM A36 | ≥ 235 MPa | ASTM A123 / ISO 1461 (≥86μm) | 120–140 km/h | 25+ Years |
| Heavy-Duty Polygonal Highway Pole | Q355B / ASTM A572 Gr 50 | ≥ 355 MPa | Hot-Dip Galvanized + RAL Polyester | 150–180 km/h | 30+ Years |
| High Mast Tower (Raising/Lowering) | Q355C / High Toughness | ≥ 355 MPa | Internal/External Zinc Immersion ≥100μm | 180–220 km/h | 35+ Years |
| Multifunctional Smart City Column | Q355B Structural Alloy | ≥ 355 MPa | Duplex System: HDG + Fluorocarbon PU | 140–160 km/h (Multi-payload) | 30+ Years |
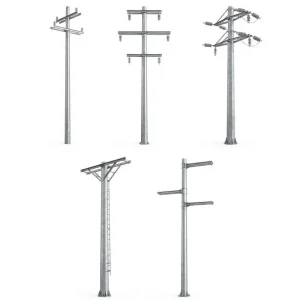
| Urban Distribution Utility Power Pole | Q420B / High Yield Alloy | ≥ 420 MPa | Heavy Immersion Zinc (≥120μm) | Per ASCE 48 Heavy Ice/Wind | 40+ Years |
Supply Chain Velocity: The Gaoyou Production Hub Advantage
How centralized regional clustering, end-to-end in-house manufacturing lines, and direct deep-water port logistics create unassailable efficiency and cost protection for overseas engineering contractors.
Integrated 100,000 m² Facility
Unlike trading middlemen or small assemblers, our Gaoyou facility consolidates steel coil CNC uncoiling, hydraulic laser cutting, automated 16-meter single-seam tandem pressing brakes, robotic submerged arc welding, deep hot-dip galvanizing kettles, and automated multi-color powder booths under one certified management chain.
Rapid 14-Day Production Cycles
Direct raw material supply alliances with major domestic primary steel producers (Baosteel, Shagang) give us perpetual access to mill-certified sheet stock without supply choke points. Standard container-volume municipal street light orders ship in as little as 14 business days, eliminating the multi-month backlogs common in Western supply chains.
Direct Shanghai & Ningbo Seaport Exit
Situated strategically along the Yangtze River delta industrial corridor, our logistics division manages seamless containerized drayage and break-bulk flat-rack vessels to Shanghai and Ningbo marine terminals, guaranteeing punctual vessel boarding and reliable bill-of-lading (BL) turnaround for tender milestones.
Localized Engineering Support & Tender Compliance Assurance
From initial DIALux lighting calculations to engineer-stamped structural calculations and comprehensive metallurgical inspection reports, we equip contractors to pass review on the very first submittal.
DIALux EVO Simulation & Photometrics
Our lighting design engineers produce turn-key DIALux EVO simulation reports modeling exact roadway geometry, surface reflectance indices (R1–R4), driver observer viewpoints, and target lighting classes (M1–M6, C0–C5, P1–P6). You get optimal pole spacing and luminaire tilt plans to eliminate zebra banding and guarantee energy compliance.
Structural FEA & Wind Load Engineering
Every pole design undergoes 3D Finite Element Analysis (FEA) evaluating maximum bending moments, shear stress distribution at the base flange, and natural resonant frequencies under sustained and gusting wind conditions up to 220 km/h in accordance with AASHTO LTS-6 and Eurocode 3 (EN 1993-1-1). Stamped calculations are supplied directly for project approval.
Multi-Stage Quality Control Protocol
Every production lot is documented under a traceable ISO 9001/14001 Quality Inspection Plan (ITP). Testing includes ultrasonic testing (UT) and magnetic particle testing (MT) of longitudinal weld seams, magnetic dry-film thickness (DFT) checks on zinc coatings per ASTM A123, spectrochemical composition analysis, and pull-out tensile tests on anchor cages.
Engineered Municipal & Highway Infrastructure Solutions
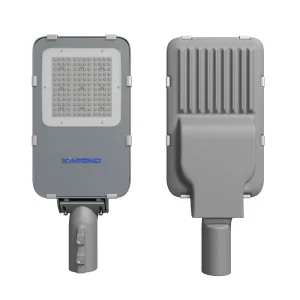
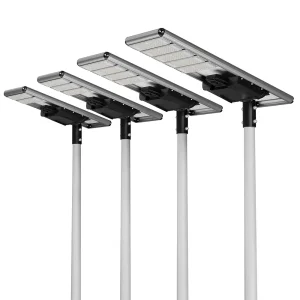
Explore our complete export line: custom street light poles, solar street lights, high masts, and power distribution columns engineered to global standards.
Frequently Asked Questions: Sourcing Outdoor Lighting Poles
In-depth responses covering procurement specifications, steel metallurgy, anti-corrosion chemistry, structural calculation review, and international shipping protocols.
Yangzhou Xintong is a verified manufacturer founded in 1999. We own and operate a specialized 100,000 square meter industrial production complex in Gaoyou, Jiangsu Province, China. Our facilities feature seven automated production lines covering coil uncoiling, laser slitting, CNC 16-meter hydraulic press braking, longitudinal submerged arc welding, integrated hot-dip galvanizing, and electrostatic powder coating. International clients are welcome to inspect our facility in person or arrange third-party audits via SGS or Bureau Veritas.
We fabricate standard lighting columns from Q235B structural steel, which matches or exceeds European EN 10025 S235JR and American ASTM A36. For heavy-duty masts, high-wind corridors, and power transmission shafts, we use Q355B (equivalent to EN 10025 S355JR and ASTM A572 Grade 50). Every steel heat batch is supplied with an EN 10204 Type 3.1 mill test certificate (MTC) documenting tensile strength, yield limits, elongation, and carbon equivalent values.
Corrosion protection begins with total chemical immersion pickling and fluxing, followed by complete hot-dip galvanization according to ASTM A123 or BS EN ISO 1461. The structural steel is completely submerged in a 450°C molten zinc kettle, producing a metallurgical iron-zinc alloy layer with an outer zinc shell typically measuring 86μm to 120μm thick. For severe marine environments (Class C5-M), we apply an optional electrostatic polyester powder topcoat or two-pack polyurethane fluorocarbon layer, delivering a 25- to 50-year maintenance-free service life.
Yes. Our engineering division operates dedicated DIALux EVO and AutoCAD stations along with specialized finite element structural software. When given your road classification, roadway cross-section, target lux/luminance criteria, and local design wind velocity, we prepare complete tender packages. These include 3D photometric isolux maps, pole spacing plans, anchor bolt reaction calculations, and foundation base design recommendations for engineer-of-record submission.
Our standard high mast towers (15m to 40m) are modeled against standard AASHTO LTS-6 (Standard Specifications for Structural Supports for Highway Signs, Luminaires, and Traffic Signals) or Eurocode EN 1991-1-4. Masts are commonly certified for sustained gust speeds from 160 km/h up to 220 km/h (approx. 45 to 61 m/s), factoring in EPA (Effective Projected Area) fixture loads. Base plates and foundation anchor cages are calculated to accommodate dynamic deflection limits and local UBC/IBC seismic zone parameters.
To prevent surface abrasion, metal scraping, and container salt contamination during ocean transit, poles are wrapped in dense bubble wrap, woven geotextile fabric, or thick corrugated sleeves. For nested shipping configurations, internal rubber edge collars prevent metal-to-metal rubbing. Anchor cages, access cover plates, luminaire brackets, and hardware kits are crated in seaworthy, fumigated solid-timber boxes labeled with matching project mark numbers.
Ready-to-Submit Project Proposal Checklist
To receive an accurate technical quotation, CAD fabrication shop drawing, and photometric simulation within 24 business hours, please assemble the following project criteria:
1. Geometry & Height
Target mounting height (m/ft), bracket outreach length, single or double arm orientation, pole shape (conical, octagonal, square, stepped cylindrical).
2. Wind & Climate
Basic design wind speed (m/s or km/h), topography factor, operational temperature range, and exposure category (coastal, open terrain, urban canyon).
3. Power & Photometrics
Grid AC low-voltage line input or standalone off-grid DC solar system (including required autonomy days for cloudy weather), target maintained lux or EN 13201 class.
4. Delivery & Standards
Contract lot quantity, intended destination seaport (Incoterm: FOB, CIF, or DDP), and mandatory national certifications (AASHTO, EN 40, CE, SASO, RETIE).