Primary Infrastructure Series
High Mast & Distribution Pole Systems Ready for Export
Pre-engineered foundation-ready pole platforms fabricated in our 100,000 m² automated facility in Jiangsu, China, built to integrate seamlessly with standard reinforced civil footing packages.
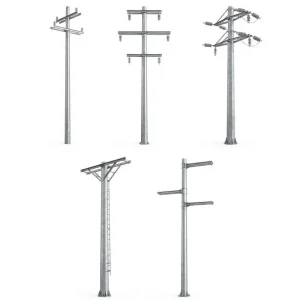
High-Quality URBAN-GRID Series Urban Low Voltage Steel Power Distribution Poles
Configure Spec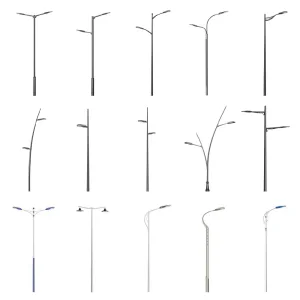
Custom XINTONG Full Series Municipal Street Light Poles Conical, Octagonal & Customizable
Configure Spec
Best Series Decorative Street Light Pole Manufacturers, Manufacturer
Configure Spec
OEM AIRPORT-PORT SERIES High Mast Light Manufacturer, Supplier
Configure Spec
High-Quality STADIUM SERIES High Mast Light Factory, Exporter
Configure Spec
Buy XINTONG Municipal Street Light Pole Series Factories, Exporter
Configure Spec
OEM PUBLIC TRANSIT Series Municipal High Mast Poles Manufacturers, Supplier
Configure Spec
Technical Whitepaper: Engineering Foundation Systems
High Mast Foundation Dynamics: Mitigating Overturning Moments & Dynamic Fatigue
In high-elevation area lighting systems ranging from 15 meters to 50 meters, the civil foundation is the single most critical structural element dictating overall asset lifespan and public safety.
Unlike standard street lighting poles that primarily sustain vertical dead weight and modest localized wind shear, high mast lighting towers (HMLT) act as massive cantilevered inverted pendulums. The foundation is subjected to extreme dynamic overturning moments (Mu), cyclic torsional fluttering, cross-wind vortex shedding, and base-shear stresses generated by variable wind profiles exceeding 160 km/h to 260 km/h. As a leading manufacturer and exporter in China's specialized infrastructure sector, Xintong designs and manufactures fully integrated high mast foundation anchor cages, engineered template assemblies, and bespoke structural sub-grade anchorages that eliminate the risks of structural shearing, bolt elongation, and foundation tilting.
Every foundation package is calculated utilizing finite element modeling (FEM) based on the project's precise geotechnical soil parameters, local ground acceleration coefficients (PGA for seismic zones), and aerodynamically projected luminaire cross-sections (Effective Projected Area, EPA). By bridging the gap between structural steel fabrication and on-site geotechnical civil execution, we deliver certified tender-compliant foundation designs ready for municipal, port authority, airport, and mega-transportation installations worldwide.
Drilled Shaft Caisson Foundations
The global gold standard for high mast towers. Deep cylindrical cast-in-place drilled shafts utilize continuous peripheral soil skin friction and passive lateral soil resistance to withstand enormous overturning moments with minimal surface footprint.
Pad & Chimney Spread Footings
Engineered for rocky strata or sites with shallow impenetrable bedrock where deep drilling is cost-prohibitive. Wide reinforced spread concrete pads counteract base uplift and lateral thrust via concrete gravity deadweight.
Marine Piled Cluster Foundations
Tailored specifically for coastal container ports, reclaimed land, and estuarine terminals. Driven pre-stressed concrete or steel tube pile clusters tied into an integrated structural capping slab absorb high-cyclic dynamic marine vibrations.
Geotechnical Sizing Benchmarks
High Mast Foundation Engineering Parameter Matrix
Reference technical matrix illustrating relationship between pole mounting heights, soil bearing capacities, anchor bolt cage diameters, and foundation volumetric concrete parameters.
| Tower Height | Typical Overturning Moment | Min. Soil Bearing Capacity | Recommended Foundation Type | Shaft Diameter × Depth | Anchor Bolt Spec & Grade |
|---|---|---|---|---|---|
| 15m – 20m (Interchanges/Plazas) | 120 – 250 kN·m | ≥ 150 kPa (Cohesive Silt/Sand) | Drilled Cylindrical Shaft | Ø 1.0m × 3.5m Depth | 8× M30 (ASTM F1554 Gr 55 / 8.8) |
| 25m – 30m (Rail Terminals/Highways) | 350 – 680 kN·m | ≥ 180 kPa (Dense Sandy Gravel) | Drilled Caisson or Pad Footing | Ø 1.3m × 4.8m Depth | 12× M36 (ASTM F1554 Gr 55 / 8.8) |
| 35m – 40m (Seaports/Aprons) | 850 – 1,450 kN·m | ≥ 200 kPa (Stiff Clay/Weathered Rock) | Deep Caisson with Rock Socket | Ø 1.6m × 6.5m Depth | 16× M42 (ASTM F1554 Gr 105 / 10.9) |
| 45m – 50m (Stadiums/Super-Hubs) | 1,800 – 3,200 kN·m | ≥ 250 kPa (Competent Bedrock) | Multi-Pile Cap or Heavy Caisson | Ø 2.0m × 8.5m Depth | 20-24× M48 (42CrMo High-Tensile) |
*Note: Geotechnical parameters above are representative benchmarks. Final foundation dimensions must be determined by a licensed Geotechnical Engineer of Record (EOR) incorporating local soil borehole SPT (Standard Penetration Test) blow counts, water table elevations, frost line depths, and site-specific ultimate limit state (ULS) load factors.
Smart Manufacturing & Supply Chain
Why Tier-1 EPC Contractors Procure Foundations from China
Combining industrial cluster efficiencies, fully automated CNC production lines, and direct metallurgical integration in Gaoyou, Jiangsu.
End-to-End Vertical Manufacturing
From primary Q235B/Q355B coil decoiling and laser-cutting anchor templates to robotic rebar ring welding and internal hot-dip galvanizing kettles, our 100% in-house manufacturing process eradicates multi-tiered sub-contractor markups and guarantees stringent QA/QC oversight.
High-Integrity Anchor Cages
We supply pre-assembled or flat-packed modular anchor bolt cages manufactured with CNC-cut dual positioning steel templates (top and bottom). This guarantees pitch-circle diameter (PCD) tolerances within ±1.5 mm, eliminating on-site alignment drift during concrete pouring.
Severe Corrosion Metallurgy
All anchor threads and hardware undergo ASTM A153 Class C or EN ISO 1461 hot-dip galvanizing with spun centrifuge de-burring, or proprietary Dacromet / Sherardizing anti-corrosion treatments capable of surpassing 1,500 hours of continuous neutral salt spray (ASTM B117) testing.
Containerized Export Logistics
By nesting foundation templates, segmented rebar cages, and hardware kits directly alongside multi-sided high mast mast polygonal sections, shipping space utilization reaches 95%+, drastically cutting ocean freight costs per unit for international maritime consignments.
Technological Evolutions
Emerging Trends in High Mast Civil Foundation Engineering
Transforming static civil foundations into smart, sustainable, and dynamically monitored structural assets for future-proof smart city infrastructure.
IoT Structural Health Monitoring (SHM)
Integration of fiber-optic Bragg grating sensors and tri-axial MEMS tilt sensors within the concrete foundation core to measure dynamic soil settling, base plate micro-deflections, and bolt tension losses in real time via cloud platforms.
Low-Carbon Geopolymer Concrete
Adoption of blast furnace slag and fly-ash based geopolymer concrete mixes for heavy foundation pours, reducing embodied carbon dioxide emissions by up to 45% while offering superior resistance to aggressive soil sulfate attacks.
BIM LOD 400 Digital Twin Modeling
Full 3D digital coordination of underground rebar placement, conduit stub-ins, grounding copper meshes, and civil foundation envelopes to resolve spatial clashes with adjacent sub-surface utilities prior to site mobilization.
Challenging Geotechnical Environments
Localized Engineering Solutions Across Extreme Geographies
Customized geotechnical footing adaptations engineered to counteract extreme terrestrial and maritime site conditions.
Coastal Typhoon Corridors
For installations along hurricane and typhoon-prone coastlines (e.g., Southeast Asia, Caribbean). We specify oversized drilled shaft depths with flared bell-bottom footings and Grade 105 high-tensile anchor rods designed for Category 5 gusts up to 260 km/h.
High Seismic & Liquefaction Zones
In regions with high Peak Ground Acceleration (PGA > 0.4g) and loose saturated sandy soils subject to seismic liquefaction. Foundations integrate interlocking spiral reinforcement ties and deep micro-piling anchoring directly into firm bedrock.
Arid Deserts & Shifting Sand Dunes
Middle Eastern and North African installations face extreme surface heat fluctuations, thermal differential expansion, and non-cohesive shifting sands. We engineer geogrid-stabilized sub-bases with sacrificial corrosion allowances on subterranean steel elements.
Sub-Zero Permafrost & Frost Heave
Designed for Central Asia and high-latitude mining infrastructure. Foundations incorporate non-frost-susceptible backfill sleeves and insulated foundation caps extended beneath the active seasonal freezing depth to prevent vertical jacking.
Macro EPC Turnkey Solutions
Integrated High Mast Foundation Systems for Key Global Sectors
Comprehensive turnkey engineering support from structural anchor fabrication to on-site concrete curing guidelines.
Container Terminals & Maritime Ports
High-volume cargo ports require 30m–40m masts supporting high-powered LED floodlight clusters adjacent to heavy container crane travel corridors. Foundations withstand heavy axle wheel surcharge loads from reach stackers and straddle carriers.
International Airport Aprons & Terminals
FAA/ICAO compliant aprons demand strict tower rigidity to maintain precise beam aiming and eliminate strobe flutter for pilots. Foundations are engineered with minimal permissible rotational deflection (< 0.5° at mast top under design winds).
Sports Stadiums & Olympic Complexes
Heavy head-frames carrying asymmetrical TV broadcast floodlighting configurations generate pronounced torsional twisting loads. Double-rebar cage designs provide exceptional torsional rigidity and dampening response.
Global EPC Qualification
Tender Compliance & Quality Verification Standards
Ensuring complete documentation, traceable raw material certification, and rigorous inspection protocols for international civil tenders.
Global procurement teams working for Tier-1 contractors (such as Bechtel, VINCI, Bouygues, and CSCEC) mandate exhaustive structural compliance files before issuing factory approval. Xintong fulfills all primary international design codes and material inspection standards:
AASHTO Standard Specifications
Calculations adhere to AASHTO Standard Specifications for Structural Supports for Highway Signs, Luminaires, and Traffic Signals, addressing both Ultimate and Fatigue Limit States (Fatigue Category I for high mast structures).
ASTM F1554 / ISO 898-1 Bolting
Anchor bolts fabricated strictly from ASTM F1554 Grade 55 or Grade 105 alloy steel, or ISO 898-1 Class 8.8/10.9, accompanied by EN 10204 Type 3.1 Inspection Certificates with Charpy V-Notch impact testing at -20°C.
NDT Weld & Thread Inspection
100% Non-Destructive Testing (NDT) via Magnetic Particle (MPI) and Ultrasonic Testing (UT) on critical load-bearing template welds, verifying complete root penetration and zero micro-fissures in primary stress transfer zones.
Engineered Foundation-Compatible Product Catalog
High Mast & Specialized Infrastructure Poles for Global Tenders
Explore our complete manufactured product range ready for pairing with precision foundation anchor packages.
OEM XINTONG Multifunctional Light Poles Integrated Design, Octagonal, Conical & Square
Configure Spec
Custom XINTONG High Strength Light Pole Series: Engineered for Extreme Conditions
Configure Spec
Buy XT-YTH-3 Series (All-In-One) Exporter, Exporters
Configure Spec
OEM XT-YTH-9 Series (All-In-One) Factory, Factories
Configure Spec
OEM AIRPORT-PORT SERIES High Mast Light Manufacturer, Supplier
Configure Spec
High-Quality STADIUM SERIES High Mast Light Factory, Exporter
Configure Spec
Buy XINTONG Municipal Street Light Pole Series Factories, Exporter
Configure Spec
OEM PUBLIC TRANSIT Series Municipal High Mast Poles Manufacturers, Supplier
Configure Spec
Technical Clarifications
High Mast Foundation Engineering FAQ
Expert engineering answers to critical geotechnical and structural queries frequently raised by project consultants and international buyers.
How are anchor bolt embedment depths and pull-out cones calculated?
Embedment depths ($h_{ef}$) are engineered based on ACI 318 Chapter 17 (Anchoring to Concrete) or Eurocode 2 Part 4. We calculate both the concrete breakout strength in tension and the steel pullout capacity. To prevent premature concrete breakout cone failure under extreme cyclic overturning moments, anchor bolts are supplied with heavy hex anchor nuts and welded bottom bearing plates that transfer tensile forces into the lower third of the reinforced concrete caisson.
Why is dual-template positioning critical during cage installation?
High mast base plates are precision flame-cut from 25mm–50mm thick structural steel plates with zero tolerance for hole misalignments. When concrete is poured into a drilled shaft caisson, the hydraulic force and vibrator action can shift individual anchor bolts. We supply sacrificial bottom positioning templates and rigid top reusable installation templates that maintain bolt verticality and pitch-circle diameter (PCD) within an ultra-strict ±1.5 mm tolerance window.
What is the standard procedure for dry-pack non-shrink structural grouting?
Between the concrete foundation pedestal and the high mast base plate, a 50mm–75mm grouting gap is maintained via leveling nuts. After final plumbness verification using dual-axis electronic theodolites, high-strength non-shrink cementitious or epoxy grout (minimum 28-day compressive strength ≥ 60–80 MPa) is packed. This ensures 100% bearing contact across the base plate surface, preventing moisture ingress and eliminating dynamic shear slippage.
How do you mitigate hydrogen embrittlement in galvanized anchor bolts?
For high-tensile anchor rods exceeding Grade 105 or Class 10.9 (yield strength > 640 MPa), acid pickling prior to hot-dip galvanizing presents a risk of hydrogen embrittlement. Xintong utilizes blast cleaning (mechanical descaling) in lieu of aggressive acid pickling, followed by temperature-controlled zinc immersion and automated centrifugal spinning. Alternatively, we apply Dacromet zinc-flake coatings, fully satisfying ASTM F2329 and ISO 10684 standards.
Can you provide certified structural calculations for our local engineering authority?
Yes. Our in-house engineering team delivers comprehensive calculation packages stamped by certified structural engineers. Deliverables include Foundation Reaction Summary sheets (Axial Force P, Shear Force V, Overturning Moment M, Torsional Moment T), L-Pile lateral soil deflection models, concrete reinforcement schedules, and 3D CAD/Revit DWG construction shop drawings tailored to the contractor's specific soil borehole investigation report.
What is the standard production lead time for customized export foundation packages?
Standard anchor bolt cages and template assemblies for production runs up to 100 sets are fabricated within 10 to 15 working days following drawing approval. Complete packages, including matching multi-section polygonal high mast towers and luminaire head-frames, are typically consolidated, export-crated, and container-dispatched via Shanghai or Ningbo ports within 20 to 30 days, complete with mill test certificates and full shipping documentation.