Featured High Mast Structures & Heavy-Duty Pole Assemblies
Direct-from-factory high mast light poles, structural cross arm frames, and smart municipal power distribution systems engineered to ASTM, AASHTO, and EN international standards.
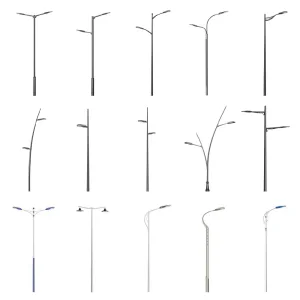
Custom XINTONG High Strength Light Pole Series: Engineered for Extreme Conditions & Heavy Loads
Request Technical Data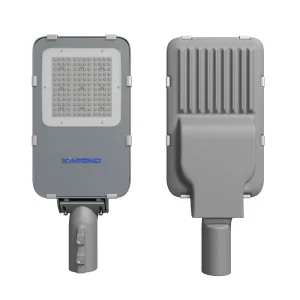
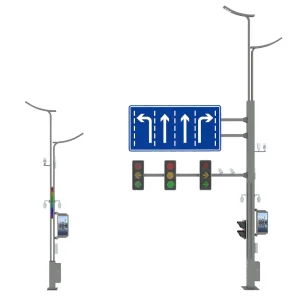
OEM XINTONG Multifunctional Light Poles Integrated Design, Octagonal, Conical & Square Poles
Request Technical Data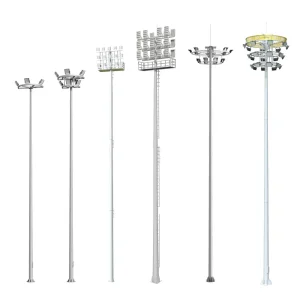
Custom XINTONG Full Series Municipal Street Light Poles Conical, Octagonal & Customizable
Request Technical Data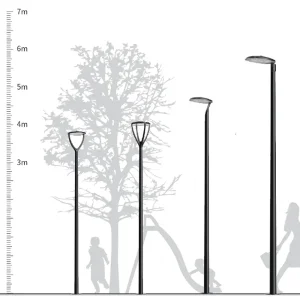
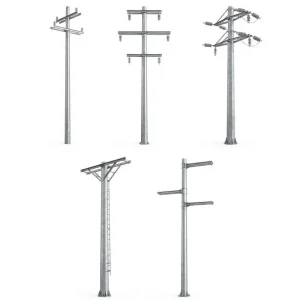
High-Quality URBAN-GRID Series Urban Low Voltage Steel Power Distribution Poles
Request Technical DataComprehensive Engineering Report: High Mast Cross Arm Structural Systems & Global Supply Chains
An authoritative technical guide on stress distribution, dynamic fatigue resistance, hot-dip galvanizing standards, and Industry 4.0 production paradigms for municipal, airport, port, and industrial lighting infrastructure.
1. The Evolution of High Mast Cross Arm Architecture & Dynamic Fatigue Mitigation
In high-mast outdoor illumination engineering—spanning towers from 15 meters to well over 50 meters in height—the High Mast Cross Arm serves as the critical mechanical junction between the vertical structural shaft and the floodlight luminaire array. Historically, cross arms were rudimentary welded steel brackets subject to severe micro-vibrations, localized stress concentrations, and premature structural failure caused by wind-induced vortex shedding. Modern structural engineering, however, treats the cross arm as a highly specialized dynamic component designed under strict AASHTO LTS-6 (Standard Specifications for Structural Supports for Highway Signs, Luminaires, and Traffic Signals) and EN 40-3 structural design codes.
As luminaire arrays shift from traditional high-pressure sodium (HPS) fixtures to high-density LED floodlights with asymmetric optical distributions, the effective projected area (EPA) and deadweight parameters have fundamentally changed. LED arrays often impose high torsional forces during wind gusts. To overcome these dynamic challenges, leading manufacturers utilize finite element analysis (FEA) to simulate 3D stress tensors under multi-directional wind speeds up to 60 m/s (approx. 216 km/h). Modern cross arm design prioritizes smooth geometric transitions, continuous longitudinal submerged-arc welding (SAW), and internal stiffener gussets to prevent localized fatigue cracking at mounting flanges.
2. Global Procurement Demands: Standardizations, Wind Speeds & Environmental Ratings
Global EPC (Engineering, Procurement, and Construction) contractors, port operators, and civil transportation agencies demand cross arms manufactured with full metallurgical traceability. Procurement specifications now mandate specific structural steel grades—predominantly Q355B, Q355C, Q355D (EN 10025 S355JR/J2) or ASTM A572 Grade 50—offering superior yield strength (≥355 MPa) and guaranteed low-temperature impact toughness down to -40°C for northern maritime or sub-polar deployments.
Environmental longevity is equally decisive. High mast installations at container ports, bulk material docks, offshore oil terminals, and coastal highways operate in severe ISO 12944 C5 (Coastal/Industrial) or CX (Extreme Marine) atmospheric corrosivity categories. To prevent interior and exterior oxidation, cross arm fabricators must implement hot-dip galvanizing conforming to ISO 1461 and ASTM A123 standards. A minimum zinc coating thickness of 86 μm (microns) is required for steel structural thickness exceeding 6mm, providing sacrificial anodic protection for over 25 to 50 years without structural degradation.
Cross Arm Structural & Material Specifications Matrix
| Engineering Metric | Standard Specification | Heavy-Duty Port / Coastal Grade | Extreme Wind / Arctic Grade |
|---|---|---|---|
| Steel Structural Grade | Q235B / ASTM A36 | Q355B / S355JR | Q355D / S355J2 (-40°C Impact) |
| Yield Strength (R_eH) | ≥ 235 MPa | ≥ 355 MPa | ≥ 355 MPa (Guaranteed Toughness) |
| Corrosion Protection | Hot-Dip Galvanized (65 μm) | HDG (86–100 μm) + Epoxy Powder Coating | Duplex System (HDG 120 μm + Fluorocarbon) |
| Design Wind Load (V_ref) | 120 km/h (33.3 m/s) | 160 km/h (44.4 m/s) | 216 km/h (60 m/s Gust Capacity) |
| Design Codes | GB 50017, ISO 1461 | EN 40, AASHTO LTS-6, BS EN 1090 | NV65, ANSI C136.3, AS/NZS 1170 |
3. China Industry 4.0: Supply Chain Resilience, Precision Robotics & Cost Advantages
The manufacturing ecosystem for heavy structural lighting poles and cross arms has undergone a monumental shift toward automated Industry 4.0 smart factories. Leading Chinese manufacturing clusters, such as those situated in Jiangsu Province, integrate complete vertical supply chains under a unified quality management framework. Key technological advantages include:
- Automated Laser Cutting & CNC Press Braking: Structural steel plates up to 20mm thick are precision-cut using high-power fiber lasers with zero heat-affected zone (HAZ) edge deformation, followed by multi-axis CNC bending to create exact octagonal, dodecagonal, or hexadecagonal cross-arm structural profiles.
- Robotic Submerged-Arc Welding (SAW): Longitudinal seam welding executed by multi-head robotic welding cells guarantees 100% full-penetration joints with ultra-low porosity, verified via non-destructive ultrasonic (UT) and magnetic particle testing (MT).
- In-House Environmentally Sealed Galvanizing Facilities: Integrated, fully enclosed hot-dip galvanizing lines featuring computerized thermal control ensure uniform zinc bath immersion, eliminating human error and preventing structural warping.
- Supply Chain Resilience & Lead-Time Agility: Direct access to primary domestic steel mills (such as Baosteel and Shougang Group) secures raw material availability during global steel price volatility, reducing standard project production cycles by up to 40%.
4. Localized Application Scenarios & Engineering Case Implementations
High Mast Cross Arms are customized to fit distinct optical, mechanical, and architectural requirements across major civil and industrial sectors:
Deep-Water Container Terminals
High-salinity marine environments demand circular symmetrical or semi-circular cross arms capable of holding up to 16 to 24 heavy-duty 1000W LED floodlights. Anti-vibration damper brackets prevent harmonic resonance caused by gantry crane movements and intense ocean winds.
International Airports & Aprons
Aviation aprons enforce strict cutoff glare restrictions and precise tilt angle locks. Cross arms are engineered with calibrated protractor gear plates, allowing engineers to set luminaire elevation angles accurately according to ICAO Annex 14 safety mandates.
Highway Interchanges & Expressways
Multi-directional radial and offset cross arms ensure uniform horizontal illuminance across complex, multi-level flyovers without creating blinding glare for oncoming drivers operating at high speeds.
Specialized Lighting Poles, Solar Systems & Power Distribution
Explore our full engineering portfolio, including split-type solar lighting assemblies, integrated smart city poles, airport high masts, and grid distribution supports.
Custom XINTONG Full Series Municipal Street Light Poles Conical, Octagonal & Customizable
Request Technical Data
High-Quality URBAN-GRID Series Urban Low Voltage Steel Power Distribution Poles
Request Technical Data
Frequently Asked Questions & Engineering Intent Analysis
In-depth answers covering mechanical integrity, structural calculations, custom fabrication tolerances, and global logistics for high-mast cross arms and pole infrastructure.
What primary structural steel grades are utilized for high mast cross arm manufacturing?
We primarily utilize Q355B and Q355C structural steel (equivalent to European S355JR/S355J2 or American ASTM A572 Grade 50). For arctic or sub-zero installations subjected to low-temperature brittle fracture risks, we utilize Q355D steel tested for impact energy values of ≥ 34 Joules at -40°C. For standard, non-heavy-load applications, high-grade Q235B steel can also be specified based on client engineering requirements.
How do you perform wind load and dynamic vibration calculations for high-mast cross arms?
Our engineering team conducts dynamic finite element analysis (FEA) adhering to AASHTO LTS-6 and EN 40-3 standards. Calculations factor in local design wind speeds (ranging from 30 m/s up to 60 m/s gusts), topography factor, height coefficient, combined Luminaire EPA (Effective Projected Area), and drag coefficients. Cross arm geometry is optimized to eliminate gust oscillation resonance and fatigue stresses on attachment flanges.
What anti-corrosion protection standards are applied for coastal or high-salinity applications?
All cross arm structures undergo hot-dip galvanizing according to ISO 1461 and ASTM A123 specifications. The steel structure is completely submerged in molten zinc after chemical pickling and cleaning, resulting in a metallurgical bond with a minimum average zinc thickness of 86 μm to 100+ μm. For harsh marine coastal (C5-M) environments, we offer a Duplex System: hot-dip galvanizing followed by a electrostatically applied architectural polyester or fluorocarbon powder coating.
Can you manufacture custom geometric configurations for specialized floodlight aiming?
Yes. We engineer and fabricate linear, curved, circular symmetrical, octagonal ring, and multi-tier offset cross arms. Custom mounting tenons, adjustable protractor plates, internal wireway conduits, and weatherproof junction boxes are integrated directly into the cross arm structural weldment based on your DIALux photometric studies and electrical plans.
What non-destructive testing (NDT) and quality control reports are provided with shipments?
Every production batch includes Mill Test Certificates (MTC EN 10204 3.1), Hot-Dip Galvanizing Thickness Test Reports, Ultrasonic Weld Inspection (UT) reports, and Dimensional Inspection Certificates. Third-party inspections (SGS, TÜV, Bureau Veritas) can be coordinated upon request prior to container packing.
What is the standard manufacturing lead time for containerized global export orders?
Standard fabrication lead times range between 15 to 25 calendar days following engineering approval of CAD/3D drawings and deposit confirmation. Our 100,000 m² factory capacity enables us to fulfill large-scale municipal or EPC port development orders of several hundred metric tons within tight project delivery schedules.
Engineered Structural Excellence for Global Infrastructure
Partner with a proven OEM/ODM manufacturer operating 7 dedicated production lines with 25+ years of international export expertise across 80+ countries.
Tender-Ready Calculations
Complete structural calculations, AASHTO wind load reports, and CAD drawings delivered for immediate engineer-of-record approval.
ISO & EN Certified Quality
Strict multi-stage QC processes ensuring flawless longitudinal welds, uniform zinc galvanizing, and zero-defect dimensional tolerances.
Agile Global Dispatch
Strategic factory location near major international sea terminals guarantees rapid container loading and ocean freight scheduling.